CE Certified Drive-In Pallet Racking Manufacturer & Exporters

High-Density Industrial Warehouse Storage Systems Engineered for Maximum Space Efficiency & Rigorous European Safety Compliance

Factory-Direct Heavy-Duty Racking

Engineered Warehouse Storage Products

Discover our comprehensive range of high-density drive-in racking, radio shuttle systems, structural mezzanines, and adjustable industrial steel pallet shelving engineered for global supply chains.

Jracking Australian Standard Industrial Racks CE Certified Heavy Duty Pallet Racking System

Jracking Australian Standard Industrial Racks CE Certified Heavy Duty Pallet Racking System

AS4084 compliant, heavy-duty structural steel frame optimized for high-capacity warehouse storage and rigorous seismic compliance.

Contact Us
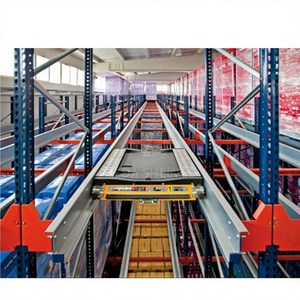
Heavy-Duty Adjustable Radio Warehouse Pallet Shuttle Racking System

Heavy-Duty Adjustable Radio Warehouse Pallet Shuttle Racking System 1000-1500kg Load

Semi-automated pallet shuttle system maximizing depth density, eliminating forklift lane entry risks while boosting pallet throughput.

Contact Us
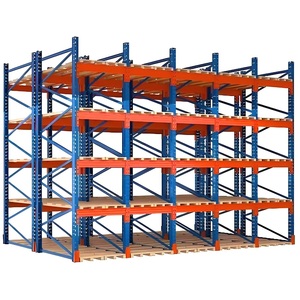
Wholesale Heavy Duty Steel Pallet Racking System

Wholesale Heavy Duty Steel Pallet Racking System for Warehouse Storage

Versatile selective pallet rack configurations built with high-tensile Q235B steel beam connections for seamless inventory access.

Contact Us
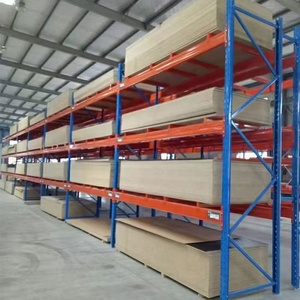
OEM Heavy Duty Pallet Racking System Warehouse Storage Rack

OEM Heavy Duty Pallet Racking System Warehouse Storage Rack Adjustable Steel 200-5000kg

Fully customizable pitch racking units designed for heavy industrial components, manufacturing hubs, and cold storage logistics.

Contact Us
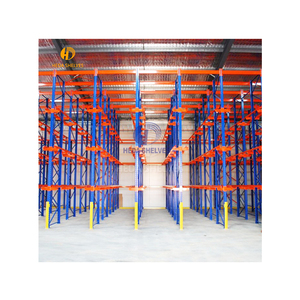
High-Capacity Drive-In Pallet Racking Storage System

High-Capacity Drive-In Pallet Racking Storage System Drive-Thru Rack for LIFO Organization

Maximizes floor area by eliminating conventional aisles. Ideal for uniform SKU batches, cold stores, and high-cube utilization.

Contact Us
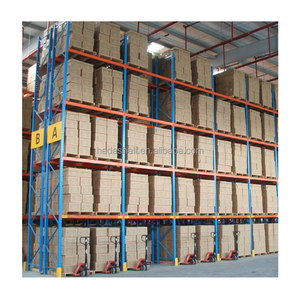
Heavy Duty Metal Pallet Storage Racking 1000kg/2000kg/3000kg

Heavy Duty Metal Pallet Storage Racking 1000kg/2000kg/3000kg Per Layer Industrial Shelving

Multi-layer high-bay racking systems engineered with continuous roll-formed upright columns for massive static loads.

Contact Us
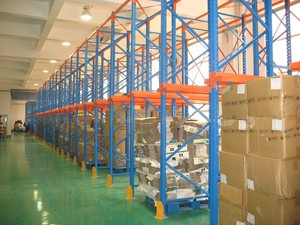
Industrial Heavy Duty Drive in Rack for Cold Storage

Industrial Heavy Duty Drive in Rack High Density Pallet Storage Racking System for Cold Storage

Specialized low-temperature steel alloy racking structures engineered to resist thermal stress in freezer storage environments.

Contact Us
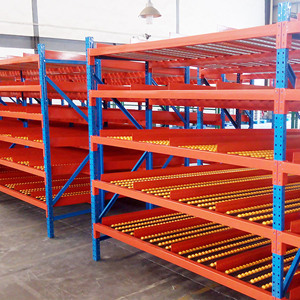
Metal Storage Carton Flow Shelves

Metal Storage Carton Flow Shelves for Industrial Warehouse Roller Picking Equipment System

Gravity-driven roller track systems designed for fast-paced order picking, FIFO inventory flow, and e-commerce distribution centers.

Contact Us
15+
Years Engineering Specs
8,000m²
Smart Production Facility
35+
Automated Machinery Sets
100%
CE & FEM Compliance
Technical Whitepaper & Architectural Guide

Engineering Principles of CE Certified Drive-In Racking

In modern industrial logistics and cold-chain infrastructure, floor space optimization represents one of the most critical drivers of operational profitability. As an industry-leading CE certified drive-in pallet racking manufacturer & exporter, Zenithrack Industrial Equipment Co., Ltd. delivers high-density warehouse storage systems engineered specifically for high-volume, low-SKU distribution frameworks. By eliminating standard operator aisles, drive-in pallet racking increases storage volume capacity by up to 75% to 80% compared to standard selective racking systems.

Key Takeaway: Volumetric Utilization vs. SKU Accessibility

Drive-In racking operates on a Last-In, First-Out (LIFO) inventory cycle, whereas Drive-Thru systems enable First-In, First-Out (FIFO) loading from opposing ends. Selecting the correct structural profile depends heavily on warehouse height clearance, pallet weight distribution, and forklift mast geometry.

1. Structural Structural Mechanics & CE Standard Compliance (EN 15512 / FEM 10.2.07)

Drive-in racking structures are uniquely vulnerable to horizontal sway and dynamic impact loads caused by forklifts driving into the storage lanes. Unlike selective pallet racking—which relies on rigid horizontal load beams—drive-in systems utilize cantilevered pallet rails supported by continuous upright columns and top-bracing frames.

To ensure total operational safety and compliance with international standards, Zenithrack manufactures all drive-in racking profiles according to rigorous European design norms (EN 15512:2019 and FEM 10.2.07):

  • High-Tensile Cold-Rolled Steel: Formed using premium Q235B and Q355B structural steel coils, offering elevated yield strength under heavy static loadings.
  • Integrated Top Tie-Beams & Diagonal Bracing: Heavy-duty top bracing trusses connect upright frames across the depth of the block, preventing longitudinal deflection and frame racking.
  • Continuous Pallet Support Rails: Cold-formed heavy-gauge steel support rails equipped with flared entry guides to minimize fork impact and align pallets smoothly.
  • Heavy-Duty Anchoring & Ground Floor Guide Rails: Floor-mounted structural steel angle rails (100mm x 75mm x 6mm minimum profile) shield upright columns from direct wheel collisions while steering forklifts down narrow aisles.

Racking System Engineering Comparison Matrix

Storage System Type Volumetric Space Density Pallet Accessibility Inventory Flow Method Forklift Risk Exposure Relative Cost per Pallet
Drive-In Racking System Very High (75%–85%) Lane Selective (LIFO) Last-In, First-Out Moderate to High Economical / Low
Radio Shuttle Racking Maximum (85%–90%) Semi-Automated (LIFO/FIFO) Both FIFO & LIFO Very Low (No Lane Entry) Moderate - High Investment
Selective Pallet Racks Standard (40%–50%) 100% Direct Access Any Order Access Low Base Level / Lowest
Structural Mezzanine Floor Doubles/Triples Area Manual / Trolley / Lift Custom Operational Flow Minimal Custom Structural Steel

2. Strategic Procurement Trends in High-Density Storage

As global supply chain operators navigate rising industrial real estate costs, logistics decision-makers are pivoting toward high-density hybrid racking solutions. Industry procurement data highlights key emerging trends shaping high-density storage sourcing:

Cold Chain Cold-Resistant Alloy Sourcing

Rapid growth in frozen food processing requires steel profiles optimized for -30°C environments without micro-fracturing or brittle fatigue.

Radio Shuttle Modular Upgradeability

Buyers now specify drive-in designs pre-engineered with dual-purpose rails, allowing seamless future upgrades to automated radio shuttle carts.

Seismic Reinforcement Protocols

Global logistics hubs require dynamic finite-element structural analysis (FEA) to verify base plate anchor shear capacity during seismic events.

3. Future Industry Development Trends (2025–2030)

The next decade of industrial storage will be governed by smart automation, advanced surface protection technology, and rapid OEM customization. Direct factory manufacturers with integrated engineering capabilities are best positioned to deliver these high-performance systems:

  1. Automated Surface Finishing & Corrosion Resistance: Micro-thin electrostatic powder coating lines (60–80 µm) combined with automated pre-treatment washing guarantee rust resistance even in coastal or humid export destinations.
  2. Integration with WMS (Warehouse Management Systems): Smart RF sensor tracking on drive-in lanes allows inventory control software to monitor batch age and prevent stock expiration in LIFO storage profiles.
  3. Factory Direct Custom Engineering (OEM/ODM): Global project contractors increasingly demand custom frame colors, tailored column pitch adjustments (50mm/75mm), and pre-welded safety barriers directly shipped from China manufacturing centers to lower total project overheads.
Why Choose Zenithrack

Factory-Direct Advantage & Quality Control

Zenithrack Industrial Equipment Co., Ltd. stands as a premier China-based storage rack manufacturer, backing global distributors and project engineers with proven technical capacity.

8,000 m² Advanced Production Hub

Equipped with 35+ automated roll-forming machines, continuous punching presses, robotic welding stations, and high-capacity powder coating lines in Dongguan, China.

Rigorous In-House Quality Assurance

A dedicated QC team performs strict structural testing on raw steel coils, weld seam integrity, dimensional tolerances, and coating thickness before container loading.

Free Layout Design & CAD Support

Our experienced structural engineering team provides complimentary warehouse layout drawings, structural load calculations, and installation guides within 24 hours.

Clear Technical Answers

Frequently Asked Questions (FAQ)

Everything procurement officers, warehouse operations managers, and structural engineers need to know about specifying CE certified drive-in racking.

How do I determine whether Drive-In or Selective Pallet Racking is right for my warehouse?
Choose Selective Pallet Racking when you stock hundreds of distinct SKUs requiring 100% immediate individual pallet access. Choose Drive-In Pallet Racking when storing uniform products in large quantities per SKU (e.g., beverage manufacturing, cold storage, seasonal inventory), where maximizing cube storage volume outweighs single-pallet accessibility.
What technical parameters are required to generate a custom racking layout and quotation?
Our engineering department requires five primary inputs:
  1. Architectural warehouse floor plan or CAD drawing showing building column positions and clear height under sprinkler/roof beams.
  2. Pallet dimensions (Length x Width x Height including cargo overhang).
  3. Maximum gross weight per loaded pallet.
  4. Forklift make, model, minimum aisle turning radius, and maximum lift height.
  5. Operating temperature range (Standard ambient room temperature vs. -30°C freezer environment).
What CE certifications and international engineering standards do Zenithrack systems meet?
Zenithrack drive-in pallet storage systems are engineered in strict compliance with CE mark requirements, FEM 10.2.07 recommendations, EN 15512 static design rules, and Australian AS4084 standards. Steel test certificates (EN 10204 3.1) and structural load calculations can be provided with export documentation.
How does drive-in racking address forklift impact safety during daily operations?
Because forklifts maneuver directly inside storage lanes, safety protection is vital. Zenithrack integrates heavy-gauge structural ground guide rails (to steer wheels cleanly), reinforced column base protectors, rounded lead-in arm entry guides, and bright safety yellow (RAL 1004) or orange powder-coating for high driver visibility.
Do you offer OEM color matching, private branding, and custom dimensions?
Yes. As a direct factory manufacturer, we regularly provide custom RAL powder-coating colors, customized upright frame depths, tailored beam pitch hole spacings, and custom-branded labeling for racking distributors, system integrators, and international engineering contractors.
What is the typical manufacturing lead time for container orders?
Standard production lead time for a 40ft high-cube container (approx. 20–25 tons of steel racking) is typically 14 to 21 days from final CAD drawing confirmation and deposit receipt. Expedited schedules are available for large-scale industrial projects.

Transform Your Warehouse Floor Space Efficiency Today

Partner with an authoritative CE certified drive-in pallet racking manufacturer. Contact our engineering team for free CAD layouts, technical consultation, and competitive direct-factory quotations.

Contact Us