Enterprise Product Line
Featured Pallet Conveyor & Storage Systems
Precision-engineered heavy-duty conveyors, radio shuttles, and ASRS warehouse racking designed for high throughput and robust load management.
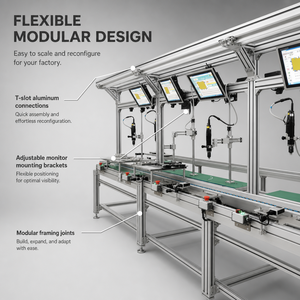
PTS2 Pallet Conveyor System for Battery Module Production Double Speed Chain
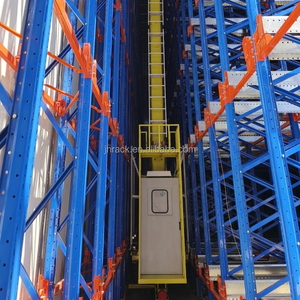
Intelligent ASRS Chain Pallet Conveyor System Industrial Automatic Pallet Racks Shelf Storage Warehouse Racking Systems
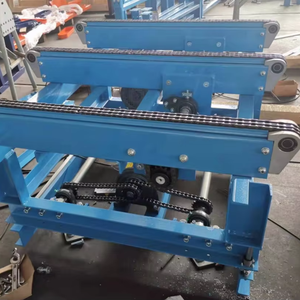
New 1000KG Load Capacity Restaurant Pallet Powered Pop up Chain Transfer Unit Conveyor System
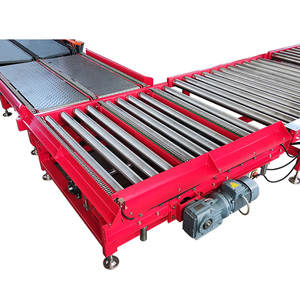
Heavy Duty Pallet Pop-up Roller Transfer Conveyor System for Australian Standard 2-Way Wooden Pallets
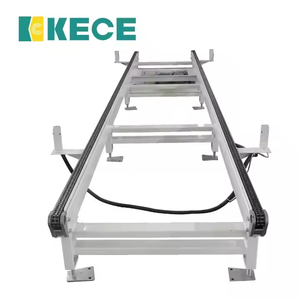
New Pallet Chain Conveyor System for Manufacturing Plant-Durable Materials Handling & Transport with Adjustable Speed
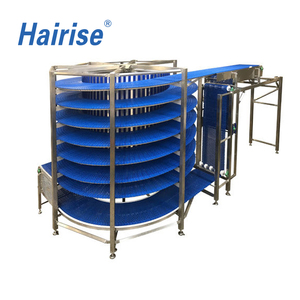
Hairise Automatic Pallet Conveyor Modular Belt Spiral Conveyor System Box Packing for Food Industry
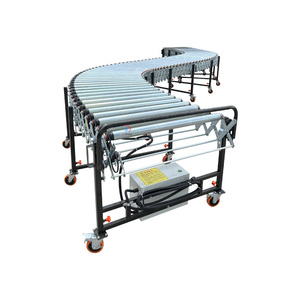
Flexible Powered Roller Conveyor Customized Pallet Handling Conveyor System for Truck Container Loading and Unloading
15+
Years Engineering Expertise
8,000m²
Advanced Manufacturing Hub
35+
Automated Equipment Sets
75+
Engineers & QC Specialists
1. Technical Architecture of Industrial Pallet Conveyor Storage Systems
Modern automated warehousing demands absolute reliability, high payload resilience, and seamlessly integrated material transport systems. As China's premier manufacturer and exporter of heavy-duty storage racking and pallet conveyor systems, Zenithrack Industrial Equipment Co., Ltd. delivers custom-engineered solutions optimized for intense industrial throughput. Pallet conveyor storage systems form the backbone of modern Automated Storage and Retrieval Systems (ASRS), cold chain distribution centers, lithium-battery manufacturing facilities, and automated automotive staging lines.
A pallet conveyor system is not merely a mechanism for horizontal transportation; it is an integrated kinematic ecosystem engineered to interface directly with high-bay pallet racking, shuttle cars, vertical lifts, and robotic palletizers. Operating under unit loads ranging from 500 kg to upwards of 2,500 kg per pallet position, structural integrity and mechanical dynamics are paramount.
Engineering Information Gain Note: Zenithrack utilizes cold-formed, high-tensile structural steel profiles (Q235B and Q355B structural grades) for frame side channels, paired with precision-ground steel rollers and dual-strand pitch drag chains. Every system is simulated via Finite Element Analysis (FEA) to ensure zero deflection under continuous maximum static and dynamic loading.
Primary Categories of Heavy-Duty Pallet Conveyor Systems
Selecting the optimal conveyor kinematic profile depends heavily on pallet bottom configuration (2-way vs 4-way entry, runner alignment), environmental factors (ambient vs sub-zero cold storage), and required cycle speeds:
- Heavy-Duty Drag Chain Pallet Conveyors: Utilizing 2 or 3 strands of precision roller chain (typically ISO 12B or 16B specification), drag chain conveyors are ideal for carrying pallets with bottom boards oriented perpendicular to the direction of travel. They offer exceptional endurance for loads up to 2,000 kg per meter.
- Motorized Live Roller Pallet Conveyors (MDR & Chain-Driven): Featuring heavy-wall steel rollers driven by sub-roller chain loops or 48V DC brushless Motorized Driven Rollers (MDR), these systems provide smooth, zero-pressure accumulation (ZPA) for fragile or high-value unit loads.
- Pop-Up Chain & Roller 90-Degree Transfer Units: Positioned at main transport junctions, these pneumatically or electrically actuated transfer mechanisms lift unit loads dynamically to change direction by 90 degrees without turning the physical pallet orientational axis.
- Double Speed Chain Conveyors (PTS2 Series): Engineered explicitly for cleanroom assembly lines, such as EV battery module assembly and electronics manufacturing. The special plastic assembly chain allows carrier plates to travel at 2.5 times the speed of the underlying drive chain, drastically reducing cycle times.
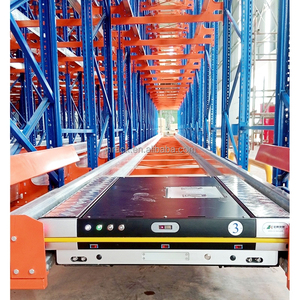
- Radio Shuttle Integrated Pallet Racking: Semi-automated high-density storage where autonomous radio-controlled shuttles travel along internal racking channels, fed directly by main inbound and outbound heavy-duty chain conveyors.
2. Structural Specifications & Operational Capabilities
To assist system integrators, warehouse architects, and procurement officers, the following matrix outlines the standard technical benchmarks of Zenithrack pallet conveyor units:
| System Type | Nominal Load Capacity | Conveyor Speed Range | Optimal Pallet Compatibility | Primary Industrial Applications |
|---|---|---|---|---|
| Heavy-Duty Chain Conveyor | 1,000 kg – 2,500 kg / pallet | 9 – 18 m/min (VFD Adjustable) | Euro (1200x800), GMA (48x40"), Block Pallets | ASRS Inbound Staging, Cold Storage, Manufacturing |
| Powered Live Roller (CDLR) | 500 kg – 1,500 kg / pallet | 12 – 24 m/min | Chep, Australian Standard (1165x1165), Slip Sheets | Zero-Pressure Accumulation, Buffer Storage |
| Pop-Up Transfer Unit | 1,000 kg – 2,000 kg / unit | Cross Transfer: 12 m/min | All 2-way and 4-way wooden/plastic pallets | Right-angle routing, Sorting Loop Intersections |
| PTS2 Double Speed Chain | 100 kg – 500 kg / pallet | Up to 30 m/min (2.5x speed) | Custom Precision Workpiece Carriers / Aluminum Pallets | EV Battery Assembly, Cleanroom Tech, Automotive |
| Radio Shuttle System | 1,500 kg / pallet slot | Unloaded: 1.2 m/s | Loaded: 0.8 m/s | Standardized Warehouse Pallets (LIFO / FIFO) | High-Density Warehouse Deep-Lane Staging |
3. Enterprise Manufacturing Advantages of Zenithrack
With over 15 years of deep industry immersion, Zenithrack Industrial Equipment Co., Ltd. has grown into one of China's top tier warehouse storage and conveyor manufacturers, recording annual domestic and export sales surpassing 100 million RMB. Operating from an expansive 8,000 m² modern manufacturing plant in Dongguan, China, we operate as a direct manufacturer—never a middleman broker.
Full In-House Fabrication
Our facility houses 35 sets of specialized production machinery, including continuous CNC cold-roll forming lines, high-precision laser tubing cutters, robotic welding cells, and an automated electrostatic powder-coating line.
Rigorous In-House QC Protocols
Our 75+ member workforce includes dedicated quality control inspectors who audit steel chemical composition (Q235B/Q355B verification), profile tolerance, weld seam depth, and powder-coat thickness (60-80 microns) at every stage.
Free Engineering & Layout Design
We provide full structural CAD engineering, load deflection calculations, and 3D layout simulation drawings entirely free of charge prior to order commitment, matching your exact building dimensions.
4. Future Global Procurement Trends in Pallet Conveyor & Storage Systems (2025–2030)
As international supply chains shift toward hyper-automation, sustainability, and resilience, global buyers and logistics managers must align their procurement strategies with four key emerging industry trends:
Trend 1: Integration of 48V DC Low-Voltage Brushless Motors (MDR)
Traditional high-power 3-phase AC motor drives are rapidly giving way to localized 48V DC Motorized Driven Rollers in zero-pressure accumulation (ZPA) conveyor circuits. 48V MDR units consume up to 60% less energy by operating purely on-demand (run-on-concept), aligning with global corporate ESG mandates while substantially lowering factory operational expenditures.
Trend 2: Hybrid Shuttle-Conveyor Synergy & Dark Warehousing
Fully automated "dark warehouses" (operating without human lighting requirements) demand autonomous interoperability between main trunk line chain conveyors and deep-lane radio shuttle racks. Procurement is trending away from isolated equipment toward turnkey integrated sub-assemblies pre-equipped with IoT sensor mounts, photo-eye brackets, and plug-and-play fieldbus connectors (Profinet / EtherNet/IP).
Trend 3: Customized Cleanroom & Anti-Corrosive Finishes
With the explosive growth of EV battery Gigafactories and pharmaceutical cold chains, standard painted steel conveyor frames are being superseded by heavy-duty hot-dip galvanized finishes and SS304/SS316 stainless steel assemblies capable of withstanding aggressive chemical washdowns and sub-zero condensation environments without flaking or oxidizing.
Trend 4: Modular Standardization for Rapid International Deployment
Global engineering procurement construction (EPC) contractors are prioritizing modular, standardized conveyor bed sections (1.5m, 2.0m, and 3.0m standard module frames). This standard modularity enables rapid ocean container packing, lowers freight costs, and permits rapid on-site assembly with minimal field welding required.
Engineering Knowledge Base
Pallet Conveyor Procurement FAQ
Expert answers to common engineering, customization, and logistics inquiries.
How do I determine whether to specify a chain conveyor or a roller conveyor for my pallets?
The decision primarily depends on pallet bottom board orientation relative to travel direction. If the pallet runners (bottom boards) are parallel to the direction of travel, a chain-driven live roller (CDLR) conveyor provides stable support across the rollers. If the pallet runners are perpendicular to travel direction, a 2-strand or 3-strand heavy-duty drag chain conveyor is mandatory to prevent the runners from dropping between rollers.
What specific warehouse information is required for Zenithrack to generate a free layout design?
To provide an accurate CAD layout and engineering quotation, please provide: (1) Warehouse structural CAD or floor plan with column locations; (2) Building clear ceiling height; (3) Pallet dimensions (Length x Width x Height including cargo overhang); (4) Maximum and average load weight per pallet; (5) Operating environment temperature range; and (6) Preferred forklift type or automated interface requirement.
Can Zenithrack pallet conveyor systems integrate directly with third-party WMS / PLC networks?
Yes. All our mechanical conveyor assemblies and automated shuttle systems can be supplied complete with standardized sensor mountings, junction boxes, motor drives (SEW, Nord, or Siemens), and control architectures compatible with Siemens S7-1200/1500, Allen-Bradley, or Omron PLCs utilizing Profinet, EtherNet/IP, or Modbus protocols.
What structural steel quality standards and safety certifications do your products comply with?
Zenithrack products are manufactured using certified Q235B and Q355B grade structural steel adhering to international standards including ISO9001 quality management, CE safety compliance, European FEM 10.2.02 racking design codes, and American RMI (Rack Manufacturers Institute) standards.
What are your lead times for export orders, and do you supply sample units?
Standard production lead times range from 15 to 25 calendar days depending on total project volume and customization complexity. We provide physical product component samples (beam profiles, upright sections, conveyor roller assemblies) free of charge (freight collect) so clients can evaluate our manufacturing quality prior to full contract signing.
How does Zenithrack ensure corrosion protection for cold storage environments?
For cold storage (-25°C to -40°C) or high-humidity food processing plants, we offer full hot-dip galvanization (HDG) exceeding 80 microns thickness or thermosetting epoxy powder coatings applied after a multi-stage zinc-phosphate pre-treatment wash to prevent structural oxidation.
Ready to Optimize Your Warehouse Throughput?
Connect directly with Zenithrack's senior engineering team. Receive your comprehensive structural load calculation, custom 3D CAD layout, and factory-direct quotation within 24 hours.