Pharmaceutical Pallet Racking Product Catalog
Engineered specifically for active pharmaceutical ingredients (APIs), biologicals, cold-chain vaccines, finished dosages, and high-density distribution hubs.
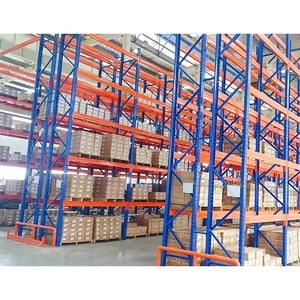 Selective Heavy Duty
Heavy Duty Steel Pallet Racking System for Pharma Storage
Direct 100% pallet accessibility engineered for high-SKU raw chemical staging and finished pharmaceutical inventory under strict GSP guidelines.
- Load Capacity: 1,000 - 4,500 kg/level
- Surface Finish: Antimicrobial Powder Coat
- Compliance: ISO 9001 / cGMP Ready
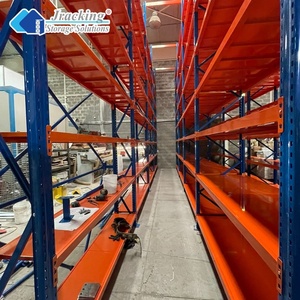 EURO Standard
 Heavy Duty Steel Pallet Racking System
Precision cold-rolled Q235B/Q355B steel structures conforming to FEM 10.2.02 and EN 15512 standards for major pharma distribution centers.
- Upright Profile: 80/90/100/120mm Omega Section
- Beam Connection: 3/4-Claw Hook Lock
- Safety Factor: 1.55 Dynamic Safety Standard
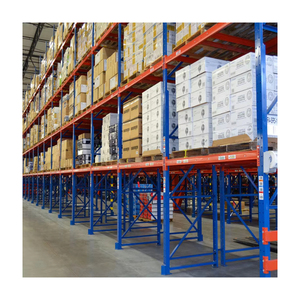 Wholesale Direct
High-Bay Selective Steel Pallet Racks for Staging
Optimized vertical footprint designed for VNA (Very Narrow Aisle) systems, maximizing volumetric efficiency in climate-controlled warehouses.
- Height Capability: Up to 15 Meters Vertical
- Aisle Width: 1.6m - 1.9m (VNA Truck Ready)
- Floor Anchorage: M16 Heavy Chemical Bolts
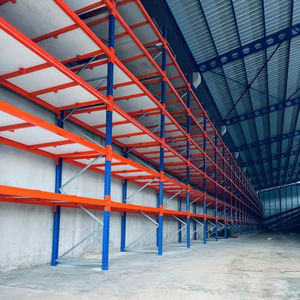 CE Certified
 Multi-Layer Stacking Racks & Pallet Shelves
Modular multi-tier structural design allowing rapid re-configuration for quarantine, release, and rejected medicine sorting areas.
- Modular Span: 1.5m - 3.3m Beam Lengths
- Certification: CE / ISO14001 / ISO45001
- Material: High Tensile Steel Strips
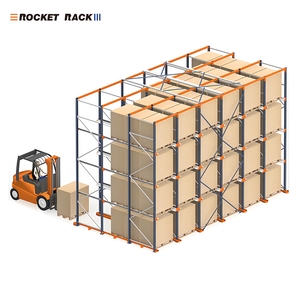 High Density Cold-Chain
Drive-In Pallet Racking System with Anti-Rust Coating
Compact LIFO high-density matrix tailored for cold storage environments (-25°C to -30°C) storing bulk vaccines and plasma products.
- Storage Density: 75% Higher Space Utilization
- Finish: Hot-Dip Galvanized / Epoxy Freeze Coating
- Operation: LIFO High-Density Deep Lane
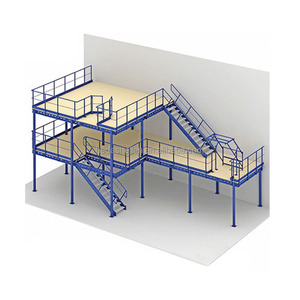 Multi-Tier Mezzanine
Rack-Supported Mezzanine Floor System for Packaging
Doubles or triples warehouse square footage, integrating specialized hand-picking levels above heavy pallet storage floors.
- Floor Load: 300 - 1,000 kg/m² Capacity
- Decking Option: Perforated Steel / Galvanized Mesh
- Access: Integrated Stairs & Cargo Lifts
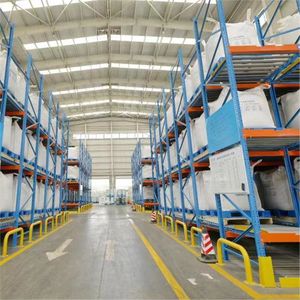 Strict FIFO Control
Dynamic Gravity Flow Pallet Racking for Expiry Tracking
Automated gravity roller system guaranteeing strict First-In-First-Out (FIFO) product flow for batch-controlled pharmaceutical goods.
- Incline Rate: 3.5% Engineered Slope Angle
- Braking System: Speed Controller Rollers Installed
- Safety: End-Separator Separates Picking Load
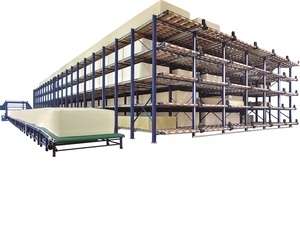 Specialized Bulk
Heavy Industrial Bulk Material & Container Racking
Custom engineered heavy-frame storage structures designed for intermediate bulk containers (IBCs) and raw material drums.
- Structure: Structural H-Steel Heavy Beams
- Protection: Corrosion-Resistant Zinc Coating
- Customization: Custom Decking & Sump Trays
Architectural Engineering Standards for Pharmaceutical Pallet Racking
Pharmaceutical supply chain management demands an unrivaled degree of structural integrity, operational cleanability, and regulatory compliance. Unlike standard commercial storage facilities, pharmaceutical pallet racking systems must comply with stringent Good Manufacturing Practice (cGMP) and Good Distribution Practice (GDP / GSP) standards. Choosing the correct China pallet racking manufacturer involves analyzing raw material metallurgy, surface chemistry, seismic deflection, and thermal expansion factors within refrigerated cleanrooms.
From storing active pharmaceutical ingredients (APIs) in controlled ISO class cleanrooms to managing high-density cold-chain vaccine hubs, warehouse structural design directly dictates bio-safety, lot separation, inventory traceability, and disaster prevention.
1. Regulatory Compliance: cGMP, GSP, and FDA 21 CFR Part 211 Alignment
In global pharmaceutical procurement, racking structures are evaluated not merely as static steel frames, but as direct environmental equipment touching regulated product distribution. Under China's revised GSP (Good Supply Practice) regulations and FDA 21 CFR 211.142, warehouse storage hardware must enable exact product segregation, prevent cross-contamination, and facilitate zero-dust hygiene.
Critical Requirement for Pharmaceutical Racking Systems
Racking systems in pharmaceutical facilities must maintain a minimum clear clearance of 100mm from walls and floor bases to allow unrestricted HVAC laminar airflow, eliminating localized micro-climates and condensation pockets that foster bacterial growth.
Key architectural standards built into top-tier Chinese pharmaceutical racking include:
- Zero-Off-Gassing Powder Coatings: Powder finishes formulated without volatile organic compounds (VOCs) or heavy metals (RoHS & REACH compliant), ensuring non-reactive performance under intense UV sterilization.
- Crevice-Free Welding Seams: Full robotic continuous MIG/TIG welding on structural joints, eliminating microscopic voids where dust, pest larvae, or chemical spills could accumulate.
- Smooth Bottom Footplates: Beveled edge floor baseplates designed to seal directly against resin epoxy flooring without puncturing fluid-tight vapor barriers.
2. Metallurgical Integrity & Cold-Chain Environmental Resilience
Cold-chain pharmaceutical warehouses operating between -25°C and -80°C place unique mechanical stress on steel structures. Standard carbon steel undergoes a ductile-to-brittle transition when exposed to sub-zero temperatures, significantly increasing the risk of structural failure under dynamic forklift impact.
Leading China racking factories utilize high-grade Q355B and specialized cold-rolled structural steel alloys alloyed with manganese and vanadium. These alloys maintain high Charpy V-notch impact toughness values at low temperatures. Furthermore, hot-dip galvanizing per ASTM A123 ensures an impermeable zinc barrier (minimum 65-85 μm thickness) that withstands thermal shock and severe condensation cycles.
| Storage Environment | Recommended Steel Grade | Surface Finish Standard | Key Engineering Focus |
|---|---|---|---|
| ISO Class 5-7 Cleanroom | SS304 / SS316L Stainless Steel | Electropolished (Ra < 0.4 μm) | Zero particulate emission, acid/alkali resistance |
| Cold Storage (-25°C) | Q355B Low-Temp Steel Alloy | Hot-Dip Galvanized (ASTM A123) | Brittle fracture resistance, condensation proof |
| Standard GSP Warehouse | Q235B Cold-Rolled Steel | Antimicrobial Epoxy-Polyester Coating | High load capacity, cost-efficiency, color coding |
| API Solvent Storage | Heavy Structural H-Beam Steel | Intumescent Fire-Resistant Coating | Explosion isolation, high-heat structural capacity |
3. Seismic Safety Dynamics & Structural Finite Element Analysis (FEA)
Because pharmaceutical inventories carry immense monetary value and critical public health importance, structural collapse during seismic events presents catastrophic risk. Premier manufacturers in China utilize 3D Finite Element Analysis (FEA) simulations based on EN 15512 and RMI (Rack Manufacturers Institute) standards to compute exact stress distribution under dynamic horizontal seismic accelerations.
Specialized seismic bracing arrays, heavy-duty floor anchor bolts, and structural beam connectors with 4-claw safety pins are standard features designed to absorb lateral displacement energy without plastic deformation.
Future Procurement & Engineering Trends (2025–2035)
The pharmaceutical logistics landscape is evolving rapidly. Next-generation warehousing relies on automated robotics, IoT sensor integration, and green materials.
1. Automated High-Bay ASRS Integration
Modern pharmaceutical facilities are moving from manual forklifts to fully Automated Storage and Retrieval Systems (ASRS). Racking acts as the structural skyscraper skeleton, requiring sub-millimeter tolerances (±0.5mm) for automated stacker cranes and AMR robots.
2. Smart IoT-Embedded Microclimate Racks
Future racking components integrate structural temperature, humidity, and vibration sensors embedded directly inside upright channels. Real-time telemetry alerts facility managers instantly if a specific rack bay breaches cold-chain thresholds.
3. Zero-VOC Antimicrobial Nanocoatings
Emerging silver-ion antimicrobial coatings applied during thermo-curing actively destroy 99.9% of bacterial spores (such as *E. coli* and *S. aureus*) upon surface contact, revolutionizing cleanroom storage sanitation.
Why Top Global Pharma Brands Partner with Zenithrack
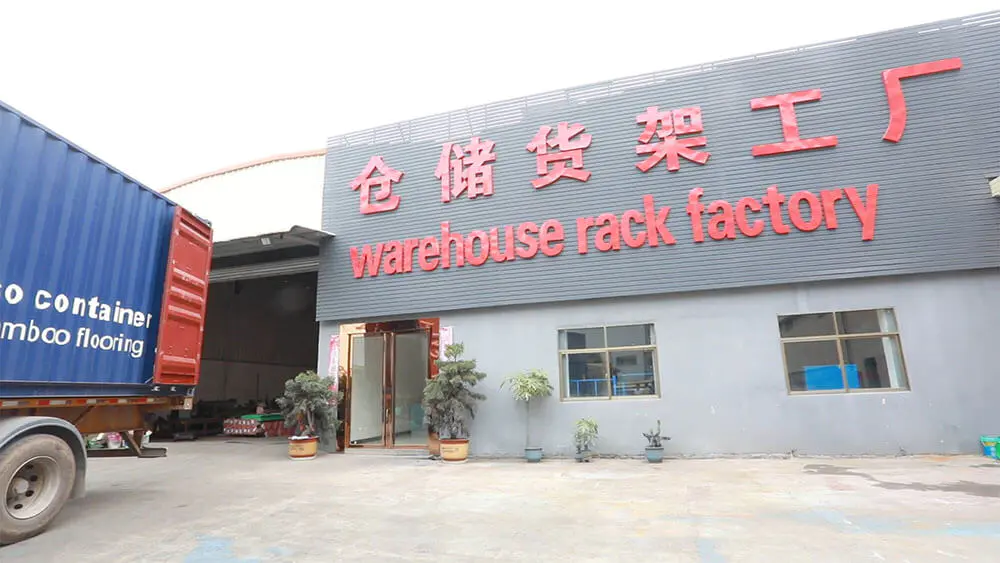
Zenithrack Industrial Equipment Co., Ltd. brings over 15 years of dedicated engineering and manufacturing excellence to the global logistics market. Operating from an advanced 8,000 m² manufacturing plant in Dongguan, China, we combine domestic scale with strict international standards.
Having grown into one of China's premier top-ten racking suppliers with annual sales exceeding CNY 100 million, our engineering team provides end-to-end support—from initial CAD layout design to global site installation guidance.
8,000 m² Modern Plant
Equipped with 35 sets of automated roll-forming and robotic welding lines.
75+ Skilled Professionals
In-house structural engineers, quality inspectors, and project managers.
Free CAD Layout & Design
Custom structural drawings tailored to your warehouse footprint within 24h.
Free Sample Policy
Examine beam profiles, steel thickness, and surface finishes risk-free.
Pharmaceutical Racking Procurement FAQ
Technical answers to key questions asked by pharmaceutical warehouse directors and project procurement managers.
How do selective racking, drive-in racking, and radio shuttle racking compare for pharmaceutical storage?
Drive-In Racks provide high-density LIFO (Last-In, First-Out) storage suitable for bulk raw materials or homogeneous finished products in cold storage rooms, though forklift entry increases collision risk.
Radio Shuttle Racks represent the optimal solution for high-density cold-chain storage: automated shuttle cars transport pallets within deep lanes, eliminating forklift entry, reducing cold-air loss, and supporting both FIFO and FILO stock rotation.
What engineering information is required to design a cGMP/GSP compliant layout?
- Warehouse CAD floor plan indicating building column positions, door access, and fire sprinkler clearance.
- Clear ceiling height under the lowest roof obstruction or HVAC ducting.
- Pallet dimensions (Length x Width x Height) including gross payload weight per pallet.
- Forklift specifications (minimum aisle turning radius, maximum mast lift height).
- Environmental conditions (operating temperature range, humidity, seismic zone rating).
Are powder coatings on your pharmaceutical racks resistant to aggressive disinfectants?
How does Zenithrack ensure load safety and structural compliance before shipment?
- Raw material spectral analysis to verify Q235B / Q355B steel composition.
- Precision laser thickness checks on roll-formed uprights and load beams.
- Ultrasonic seam inspection on all robotic welded beam connectors.
- Hydraulic compression testing according to EN 15512 static load guidelines.