Engineered Pallet Racking Systems
Select from China's top-tier warehouse racking configurations, built with high-grade Q235B/Q355B cold-rolled steel for extreme structural reliability.
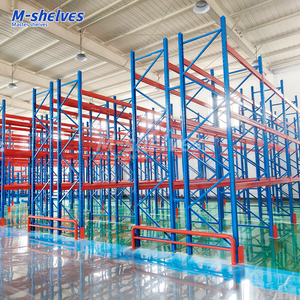
Warehouse Shelves Pallet Racking System Storage Heavy Duty Shelving Rack
Heavy-duty industrial selective racking system designed for 100% direct pallet accessibility and high floor load distribution.
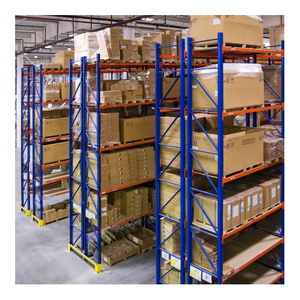
Peterack CE Certified Heavy Duty Stacking Selective Pallet Racking
CE-certified structural rack engineered for extreme weight loads, featuring adjustable beam pitch and dynamic safety locking pins.
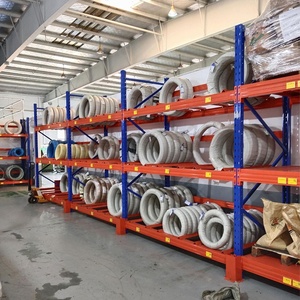
Double Deep Selective Pallet Rack for Heavy Coil Material Storage
Specialized double-deep configuration optimized for storing heavy industrial coils, maximizing storage density while preserving structural rigidity.
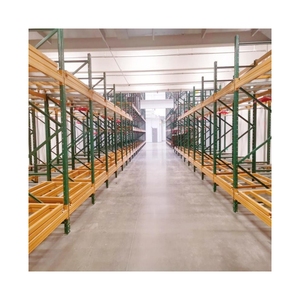
Custom Push Back Pallet Racking System With Precision Guide Rails
High-density dynamic racking utilizing nested carts and precision guide rails, allowing efficient LIFO pallet management up to 6 deep.
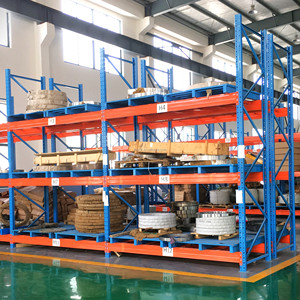
OEM Wholesale Heavy Duty Steel Pallet Racking System for Storage
Factory-direct customized industrial steel racking designed for large-scale logistics centers, cold storage, and distribution hubs.
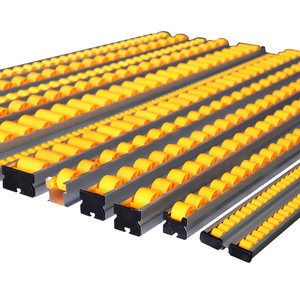
Carton Flow Rack FIFO Gravity Roller Track Storage System
Ergonomic gravity-fed flow rack featuring PE/ABS roller tracks for rapid FIFO order picking and high-volume order fulfillment.
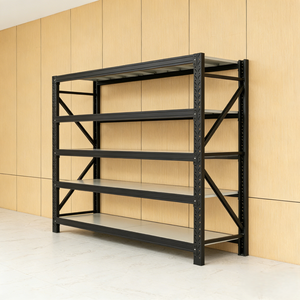
Modular Stackable Steel Racking & Shelving System
Versatile and cost-effective modular steel shelving engineered for adaptable warehouse layouts and high vertical space utilization.
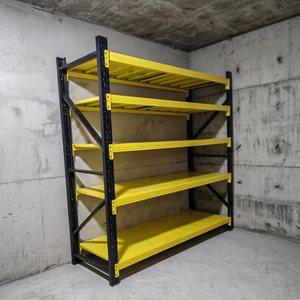
Multi-Level Industrial Steel Mezzanine Storage Platform
Rack-supported multi-tier platform system that doubles or triples warehouse usable surface floor area without building expansions.
1. Technical Engineering Architecture of Back-to-Back Pallet Racking
In modern industrial material handling and supply chain logistics, Back-to-Back Pallet Racking stands as the baseline benchmark for high-efficiency warehouse floor layout design. Structurally consisting of two single selective racking runs placed back-to-back and interconnected by structural row spacers, this configuration creates a rigid double-row structure that vastly improves frame stability, transverse moment of inertia, and overall space optimization.
By connecting adjacent upright frames with specialized tubular or structural channel row spacers, China's leading back-to-back racking factories eliminate redundant operating aisles. This design allows warehouses to achieve upwards of 40% to 50% footprint space utilization efficiency while maintaining 100% immediate selectivity for every pallet position when accessed via standard counterbalanced forklifts or reach trucks.
Information Gain Insight: Structural rigidity in back-to-back systems scales non-linearly. Connecting two upright frames with heavy-duty steel row spacers increases cross-aisle frame stability under sway loads by up to 35%, significantly reducing localized beam deflection and improving seismic safety margins under FEM 10.2.02 and RMI/ANSI MH16.1 international compliance codes.
Key Structural Components & Metallurgy Standards
A certified, heavy-duty back-to-back pallet racking assembly manufactured in China utilizes precision-rolled structural profiles engineered to handle extreme static and dynamic loads:
- Upright Frames (Columns): Cold-roll formed from high-tensile Q235B or Q355B structural steel coils. Available in profile widths ranging from 80mm to 120mm with 1.8mm to 3.0mm wall thickness, featuring teardrop or diamond-hole pitch configurations at 50mm or 75mm adjustable increments.
- Load Beams: Fabricated using dual C-section interlocking profiles continuously robot-welded to multi-claw end connectors. Beam profile depths range from 80mm to 160mm depending on span length and pallet capacity requirements (up to 4,000 kg per beam level).
- Heavy-Duty Row Spacers: Rigid horizontal tie-bars connecting paired frames at column node points, maintaining exact 200mm to 400mm flue spacing to accommodate pallet overhang and fire suppression sprinkler systems.
- Baseplates & Anchors: Heavy-gauge footplates secured to reinforced concrete slabs via expansion or chemical anchor bolts, transmitting vertical column forces evenly across floor sub-grades.
2. Comparative Matrix: Back-to-Back Racking vs. Alternative High-Density Systems
Evaluating warehouse storage systems requires analyzing space efficiency, throughput speed, capital investment per pallet position, and forklift equipment compatibility. The matrix below illustrates why procurement directors specify China-manufactured back-to-back racking for versatile logistics hubs:
| Racking System Type | Selectivity (%) | Storage Density | Forklift Compatibility | Relative Cost / Pallet | Ideal Application |
|---|---|---|---|---|---|
| Back-to-Back Pallet Racks | 100% Direct Access | Medium - High (45-55%) | Standard Reach / Counterbalance | Cost-Effective Base Rate | High SKU variety, fast stock turnover |
| Double Deep Racking | 50% Direct Access | High (60-65%) | Deep-Reach Pantograph Forklift | Moderate (+15-20%) | Multiple pallets per SKU, batch storage |
| Drive-In / Drive-Thru | Low (LIFO / FIFO) | Very High (75-85%) | Specialized Narrow Counterbalance | Moderate (+25-30%) | Cold storage, homogenous bulk goods |
| Radio Shuttle Automation | High (Automated FIFO/LIFO) | Extreme (85-90%+) | Standard Loading Forklift + Shuttle Unit | High Capital Investment | Automated distribution, high-volume FMCG |
3. Development & Technological Trends in Pallet Racking Manufacturing
The industrial warehouse rack manufacturing sector in China is undergoing a profound technological transformation. Driven by stringent global safety standards, environmental regulations, and the demand for higher vertical warehouse heights, top factories have introduced sophisticated manufacturing methodologies:
Automated Continuous Roll-Forming
Modern continuous cold-roll forming lines utilize 18 to 24 rolling stations with real-time laser monitoring, ensuring profile straightness tolerances within ±0.5mm per 10-meter column length.
Robotic Laser Welding & Fabrication
Robotic welding arms execute precise, zero-defect continuous MIG welds on beam connector claws and baseplates, eliminating human error and structural fatigue vulnerabilities under heavy dynamic loads.
Advanced Epoxy Powder Coating
Full 9-stage pre-treatment wash including automatic phosphating and degreasing, followed by electrostatic thermosetting epoxy powder coating (60-80 microns) for superior scratch and chemical resistance.
4. Future Global Procurement Trends for Warehouse Racking (2025–2030)
Sourcing structural racking systems directly from China is evolving beyond basic unit-price negotiations. Global enterprise buyers, logistics contractors, and warehouse integrators are shaping new purchasing paradigms:
A. Integration with Autonomous Mobile Robots (AMRs) & AGVs
As logistics facilities transition toward lights-out automation, back-to-back racking structures are increasingly required to incorporate bottom-level guidance channels, magnetic sensor brackets, and precise floor-level clearance profiles. Future procurement specifications prioritize factories capable of manufacturing ultra-precise tolerance uprights compatible with AMR rack-under-tunnel picking systems.
B. Carbon Neutrality & EPD (Environmental Product Declaration) Compliance
International buyers in North America, Europe, and Australia are requiring carbon footprint documentation for structural steel goods. Leading Chinese manufacturing hubs are adopting solar-powered manufacturing plants, recycled structural steel feeds (Electric Arc Furnace steel), and non-toxic powder coating processes to comply with global ESG mandates.
C. BIM (Building Information Modeling) & Digital Twin Design Workflows
Procurement teams now expect factory engineering departments to supply complete Revit/BIM 3D models alongside commercial quotations. This enables warehouse developers to conduct clash detection with HVAC, electrical conduits, and automated fire sprinkler lines before steel fabrication begins.
5. Enterprise Advantages & Manufacturing Excellence
When procuring heavy-duty storage racking systems from China, partnering with a direct manufacturer eliminates intermediary markups and guarantees rigorous quality control throughout the engineering workflow. Backed by extensive domestic and export experience, Zenithrack stands as an industry-leading manufacturing force.
Why Global Purchasing Managers Partner With Our Factory:
- Direct Factory Pricing: Eliminate middleman trading commissions. Achieve annual sales over CNY 100 million through high-capacity manufacturing scale.
- Free Custom Engineering Layouts: In-house structural engineering staff provide complimentary 2D AutoCAD floor plans, structural load calculations, and 3D installation drawings.
- Comprehensive OEM & Branding Customization: Custom RAL powder coat colors, specialized frame dimensions, localized load certification tags, and private-label packaging for international distributors.
- Rigorous In-House Quality Assurance: From raw steel coil ultrasonic testing to roll-formed profile measurement, weld seam penetration checks, and coating adhesion testing, every order is thoroughly inspected before container loading.
- Turnkey Export Services: Free sample dispatch (freight collect), bundled installation hand tools included with full-container shipments, and full sea-freight logistics support.
6. Frequently Asked Sourcing & Technical Questions (FAQ)
Direct answers from our engineering team regarding back-to-back racking layout design, international compliance, shipping optimization, and structural safety:
How do I choose between selective, drive-in, double-deep, and radio shuttle racking systems?
What parameters are required for your engineers to design a free warehouse layout drawing?
1. Building architectural plan showing clear height under roof trusses/sprinklers, column locations, dock doors, and floor slab specifications.
2. Pallet dimensions (Length × Width × Height including goods overhang) and gross weight per pallet.
3. Forklift operational parameters (make, model, aisle turning radius, maximum lift height).
4. Environmental conditions (ambient warehouse, cold storage temperature, or regional seismic load requirements).
What design standards and safety certifications do your back-to-back racking products comply with?
What is the standard production lead time and how are containers optimized for ocean freight?
Do you offer free physical samples and OEM branding support for local distributors?
How do back-to-back row spacers enhance seismic and sway stability?
Transform Your Warehouse Space Efficiency Today
Consult directly with China's leading pallet racking engineers. Receive a comprehensive CAD floor layout, structural load analysis, and competitive factory-direct quote within 24 hours.