High-Performance Pallet Racking & Crane-Supported Systems
Explore our core manufacturing line of industrial pallet racks, radio shuttle systems, and heavy-duty storage configurations designed for maximum structural longevity and high-density warehouse utilization.
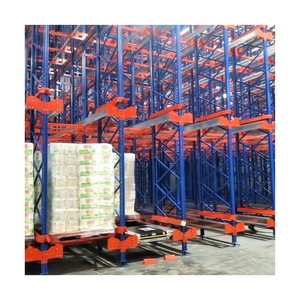
Semi-Automatic Storage Rack Corrosion Protected Shelves Radio Shuttle Pallet Racking System for Warehouse Shuttle
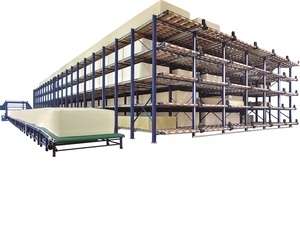
Foam Block Rack Storage System
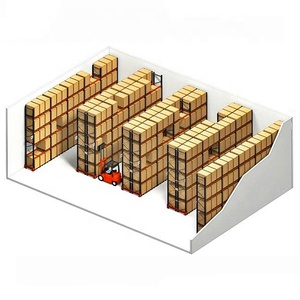
ISO CE Load 1000-3000 KG Per Level Warehouse Storage Heavy Duty Double Deep Steel Pallet Racking System Low Price
Wholesale Price Low Price 5-Layer Multi-Level Steel Adjustable Heavy Duty Pallet Racking for Sale
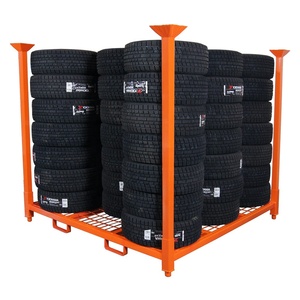
Customized Warehouse Heavy Duty Portable Rack Metal Spare Steel Detachable Stackable Pallet Tire Storage System 1000KG Powder
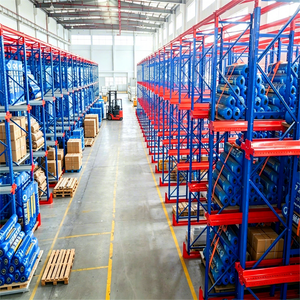
Automatic Warehouse Racking System Radio Shuttle Rack AS4084-2012 CE ISO RMI Steel Material With Corrosion Protection Raf
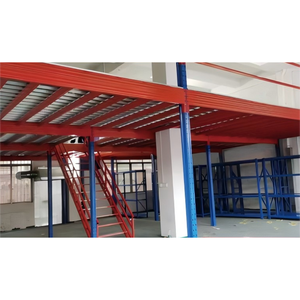
Industrial Steel Mezzanine Floor Racking System Platform Rack Warehouse Shelving Heavy Duty
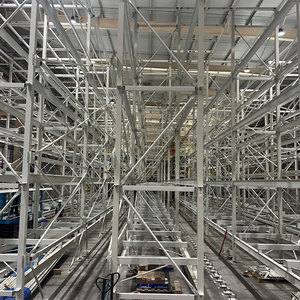
Engineering Design Pallet Rack System with High Density Layout
Structural Architecture of Crane-Supported Pallet Racking Systems
In modern high-density material handling, crane-supported pallet racking systems (frequently incorporated into Automated Storage and Retrieval Systems, or AS/RS) represent the absolute peak of volumetric warehouse efficiency. Unlike conventional free-standing pallet racks where vertical heights are constrained by forklift mast capabilities, crane-integrated structures leverage specialized stacker cranes or overhead bridge cranes to access storage heights exceeding 40 meters. As a leading manufacturer based in Dongguan, China, Zenithrack Industrial Equipment Co., Ltd. custom engineers these heavy-duty systems to handle extreme static and dynamic loading forces seamlessly.
The structural integrity of a crane-supported rack relies on cold-formed high-strength structural steel profiles—primarily Q235B and Q355B grades. In these configurations, the rack upright frame serves a dual purpose: it supports multi-tier unit loads while simultaneously absorbing dynamic impact forces, braking torques, and horizontal guide-rail thrusts generated by travelling cranes. Achieving compliance with international engineering benchmarks such as FEM 10.2.02, RMI, and AS4084-2012 requires rigorous structural calculations, including finite element analysis (FEA) to verify frame buckling stability, beam deflection limits (under strict L/200 thresholds), and seismic resistance.
High-Grade Q355B Steel
Formulated with superior yield strength (355 MPa minimum), ensuring high axial load capacity for tall upright frames under heavy stacker crane operations.
Sub-Millimeter Precision
Automated hole-punching and roll-forming guarantee tight vertical pitch tolerances (±0.5mm), critical for automated crane sensor alignment.
Modular Rack-Clad Build
Engineered to act as the primary structural skeleton of the building itself, eliminating separate building columns and maximizing interior storage footprint.
Warehouse Heavy-Duty Racking System Specifications
| Storage Racking System | Primary Load Type | Max Unit Capacity (per level) | Max Height Potential | Crane / Handling Compatibility | Compliance Standards |
|---|---|---|---|---|---|
| Crane-Supported AS/RS Racking | Palletized Goods / Heavy Containers | 1,000 kg – 3,000 kg | Up to 45 Meters | Automatic Stacker Crane / Rail-Guided Crane | FEM 10.2.02, ISO 9001, CE |
| Radio Shuttle Pallet Rack | High-Density Bulk Pallets | 1,500 kg – 2,000 kg | Up to 18 Meters | Automated Radio Shuttle + Standard Forklift | AS4084-2012, RMI, CE |
| Heavy-Duty Double Deep Rack | Standard Logistics Pallets | 1,000 kg – 3,000 kg | Up to 12 Meters | Deep-Reach Pantograph Forklift | ISO 9001, CE |
| Heavy-Duty Cantilever Rack | Pipes, Tubing, Steel Profiles, Coils | 500 kg – 4,000 kg / Arm | Up to 10 Meters | Overhead Crane / Side-Loader Forklift | CE, RMI Specifications |
| Multi-Tier Structural Mezzanine | Cartons, Small Parts, Heavy Machinery | 300 kg – 1,500 kg / m² | 2 to 4 Structural Floors | Goods Lift, Overhead Hoist, Crane Drop Zone | CE, EN 1090 Structural Steel |
Future Procurement Trends in Warehouse Storage & Crane Racking
The global warehousing and logistics industry is undergoing a structural transition towards total automation, driven by escalating labor costs, urban land scarcity, and the rise of omnichannel e-commerce. Procurement decision-makers must evaluate storage equipment not merely as static steel frames, but as dynamic assets integrated into broader digital supply chains. Key developments defining future procurement strategies include:
- Shift to Automated Rack-Supported Buildings (Clad Rack Systems): Instead of building a traditional brick-and-mortar warehouse and filling it with racks, enterprise logistics hubs are increasingly procuring rack-supported buildings. The crane racking matrix supports both the inventory loads and the building roof and side cladding, reducing initial civil construction capital expenditure by 18% to 25%.
- Smart Sensing & Continuous Structural Health Monitoring: Next-generation crane racking incorporates IoT sensor arrays directly within beam connections and upright footplates. These sensors measure real-time deflection, strain accumulation, tilt angles, and seismic vibration impacts, transmitting data directly to Warehouse Management Systems (WMS) for predictive maintenance.
- Enhanced Surface Finishes for Cold Chain & Harsh Environments: With the booming demand for pharmaceutical cold-chain and chemical storage, procurement preferences have shifted heavily toward hot-dip galvanizing (HDG) and thermosetting epoxy-polyester powder coatings with anti-microbial and anti-corrosion additives engineered to withstand sub-zero conditions down to -30°C.
- Modular Standardization & Low-Carbon Steel Supply: Global buyers are enforcing strict ESG guidelines. Chinese racking manufacturers that utilize green steel produced in hydrogen-fueled electric arc furnaces (EAF) and non-toxic powder coating processes are capturing top market share among international buyers.
Zenithrack Enterprise Capabilities & Factory Strengths
Direct Factory Manufacturing • Engineering Design • Strict Quality Assurance
8,000 m² Modernized Manufacturing Facility
Located in Dongguan, China, Zenithrack Industrial Equipment Co., Ltd. operates a state-of-the-art facility outfitted with over 35 sets of high-precision roll-forming machines, automatic continuous punch presses, and robotic MIG welding units. Over 15 years of domestic and export manufacturing experience allows us to achieve annual sales topping 100 Million RMB, solidifying our reputation as a top-tier manufacturer.
Engineered QC Protocol & Full Customization
Our 75+ team of skilled structural engineers and dedicated QC technicians verify raw steel chemistry, profile dimples, welding seam integrity, and powder coat thickness (>60 microns standard) at every production stage. We offer free CAD layout designs, structural load calculations, custom OEM colors/branding, and complimentary product samples prior to bulk production.
Frequently Asked Questions (FAQ) for Overseas Racking Buyers
How do I choose between selective pallet racking, radio shuttle systems, and crane AS/RS racking?
The choice depends on your SKU diversity, throughput velocity, and warehouse building parameters:
- Selective Pallet Racks: Ideal when you have high SKU diversity and require 100% immediate access to every pallet using standard forklifts.
- Radio Shuttle Systems: Best for high-density storage of moderate SKU counts in large quantities, significantly reducing forklift travel distances.
- Crane-Supported AS/RS Racking: Recommended when maximizing vertical space utilization (above 15 meters) with fully automated, high-speed storage and retrieval needs, operating with minimal manual labor.
What engineering information is required to generate a precise CAD layout design?
To prepare an accurate structural layout and quotation, our engineering team requires:
- Building floor plans or CAD files showing column locations, floor slab load capacities, and clear under-beam ceiling height.
- Exact pallet dimensions (Length × Width × Height including goods) and maximum weight per pallet.
- Forklift make, model, turning radius, and maximum mast reach height (if non-crane system).
- Environmental factors such as operating temperatures (cold storage vs. room temp) and regional seismic zone parameters.
Do you provide engineering design drawings and structural samples before ordering?
Yes. Zenithrack provides complete 2D layout blueprints and 3D architectural renderings completely free of charge. Furthermore, we ship physical sample components—including beam connectors, upright profile segments, and powder coat color swatches—free of charge (freight collect) so you can verify our metallurgical quality prior to contract finalization.
How does your factory handle quality control for heavy-duty crane racking orders?
Our quality control protocol follows a strict 5-tier inspection process: (1) Spectral testing of incoming raw steel coils for yield strength compliance; (2) Laser-guided tolerance checks during roll-forming; (3) Ultrasonic weld inspection on structural beam connectors; (4) Cross-hatch adhesion and thickness testing of electrostatic powder coatings; and (5) Pre-shipment trial assembly and packaging inspection to ensure flawless site erection.
Can Zenithrack produce racking according to local regional compliance standards like AS4084 or FEM?
Absolutely. Our products are fully designed, calculated, and manufactured in full alignment with international engineering benchmarks including Australian Standard AS4084-2012, European FEM 10.2.02 standards, US RMI (Rack Manufacturers Institute) specs, and ISO 9001 quality system guidelines.
Optimize Your Warehouse Storage Density Today
Consult directly with Zenithrack structural engineers to receive a free CAD layout, seismic load calculation, and factory-direct price quotation for your warehouse racking project.