Featured Automated Two-Way Shuttle Storage Systems
Factory-Direct Heavy-Duty Radio Shuttle Racking Configurations Certified to CE, ISO, and AS4084 Standards
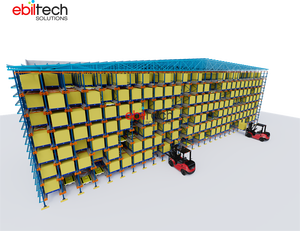
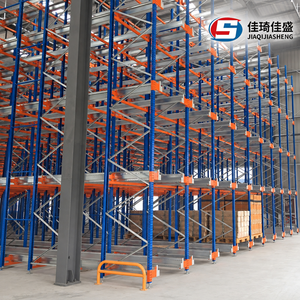
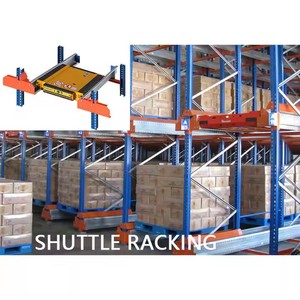
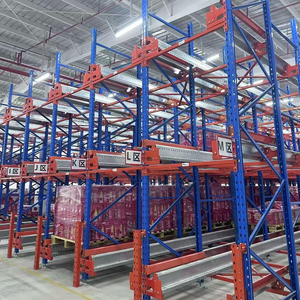
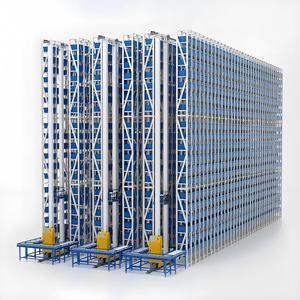
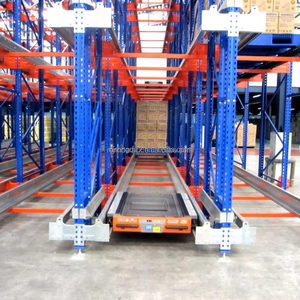
Engineering Architecture of 2-Way Radio Shuttle Racking Systems
A Comprehensive Technical Whitepaper on Structural Mechanics, Autonomous Electromechanical Motion, and High-Density Warehouse Optimization
Structural Steel Integrity & Profile Geometry
The foundation of a high-performance Two-Way Radio Shuttle Racking System rests upon structural precision and cold-rolled steel metallurgy. Upright frames are manufactured using high-tensile Q235B and Q355B structural steel grades, engineered with continuous omega profile geometry featuring 11 to 13 folding cold-formed rib lines.
This multi-stage roll-formed cross-section delivers superior torsional rigidity, effectively neutralizing dynamic lateral forces generated during the rapid acceleration and emergency braking cycles of self-propelled remote shuttle carts carrying unit loads up to 1,500 kg.
Precision Shuttle Guide Rails & Load Beam Dynamics
Unlike standard selective pallet racks or passive drive-in systems, two-way shuttle racking utilizes custom dual-purpose galvanized guide rails. These rails act simultaneously as structural load support beams for heavy pallets and as high-precision running tracks for the autonomous shuttle vehicle.
Engineered with integrated outer lip anti-derailment flanges and smooth transition entry guides, our rail profiles reduce friction coefficients to below $\mu = 0.05$, enabling whisper-quiet cart transit, zero track drift, and minimum energy consumption per pallet move.
Comparative Performance Analysis: High-Density Warehouse Systems
| System Parameter | Selective Pallet Rack | Drive-In Pallet Rack | 2-Way Radio Shuttle Rack | 4-Way Automated Shuttle Rack |
|---|---|---|---|---|
| Storage Density Index | Standard (40% - 50%) | High (65% - 75%) | Ultra-High (75% - 85%) | Maximum (85% - 92%) |
| Pallet Access Method | 100% Direct Selective | Forklift Drives into Lanes | Remote Autonomous Shuttle | 3D Matrix Automated Cart |
| Stock Handling Mode | FIFO / LIFO | Strict LIFO Only | Flexible FIFO & LIFO | Fully Automated FIFO / LIFO |
| Forklift Damage Risk | Moderate | Extremely High (Frequent Collisions) | Near Zero (External Docking Only) | Zero (Fully Automated) |
| CAPEX ROI Payback Horizon | Immediate / Low CAPEX | 12 to 18 Months | 18 to 24 Months (Optimal TCO) | 36 to 48 Months (High CAPEX) |
| Cold Storage Adaptability | Standard | Poor Air Circulation | Superior thermal flow to -25°C | Requires specialized battery heating |
Future Procurement Trends in High-Density Pallet Storage
Market Intelligence & Strategic Purchasing Insights for Supply Chain Executives (2025–2030)
1. Shift from Passive to Semi-Automated Assets
Global warehouse operators are rapidly phasing out traditional Drive-In racking in favor of Two-Way Radio Shuttle Racking Systems. Procurement managers recognize that eliminating forklift movement inside deep storage channels reduces rack structural repair costs by over 90% while doubling pallet throughput per shift.
2. Standardization of WMS / WCS API Interfaces
Modern international tenders strictly require radio shuttle carts to feature open Modbus, CAN-bus, or Wi-Fi TCP/IP communication protocols. Procurement teams are prioritizing suppliers who offer seamless RF integration with enterprise Warehouse Management Systems (WMS) for real-time inventory tracking and automated batch picking.
3. Next-Gen Lithium Iron Phosphate (LiFePO4) Power
Sourcing strategies now enforce the exclusion of obsolete lead-acid shuttle batteries. Third-generation 24V/40Ah LiFePO4 battery modules equipped with intelligent Battery Management Systems (BMS) provide continuous 8 to 10-hour operational cycles with 30-minute rapid charging capabilities and over 3,000 charge cycles.
Technology Development Trends in Two-Way Radio Shuttle Systems
Pioneering Electromechanical Innovations driving Intelligent Industrial Automation
Multi-Sensor Redundant Safety Arrays
Leading Chinese racking suppliers are embedding redundant safety arrays directly into the shuttle cart's chassis. Utilizing dual-channel photoelectric sensors, ultrasonic obstacle detectors, and mechanical anti-collision bumpers, modern shuttle carts automatically detect misplaced pallets, structural blockages, or personnel obstruction within 0.3 to 1.5 meters, executing soft braking protocols to guarantee zero warehouse incidents.
Cold Chain Thermal Isolation Management
For cold chain logistics, pharmaceutical warehouses, and frozen food distribution centers operating down to -25°C (-13°F), specialized shuttle technology has emerged. Advanced heat-tracing internal circuits, IP65 moisture-sealed electronic controls, and specialized low-temperature synthetic lubricants prevent condensation freezing and component embrittlement, ensuring 99.8% operational uptime in extreme environments.
Why Partner with Zenithrack: Industrial OEM Manufacturing Strength
15+ Years of Engineering Excellence, Direct Factory Pricing, and Rigorous ISO & AS4084 Compliance
8,000 m² Advanced Production Hub
Located in Dongguan, China, our specialized manufacturing plant houses over 35 sets of high-precision roll-forming machines, automated robotic welding cells, and continuous electrostatic powder coating production lines. We maintain absolute control over every stage of production from raw coil slitting to final surface treatment.
Strict Quality Control & Global Compliance
Every batch of raw steel sourced from premier steel mills (such as Baosteel and Shougang) undergoes rigorous yield strength, tensile testing, and ultrasonic weld seam inspections. Our two-way shuttle rack systems comply with international engineering standards including AS4084-2012, FEM 10.2.02, EN 15512, ISO 9001:2015, and CE certification.
Free CAD Layout & Turnkey Engineering
Our team of 75+ structural engineers and logistics planners offers end-to-end support, providing free CAD warehouse layout designs, 3D structural simulation models, load calculation reports, installation drawings, and complimentary spare parts kits with every global container order.
Two-Way Shuttle Racking Technical & Procurement FAQ
Essential Answers to Technical, Operational, and Commercial Inquiries from Overseas Warehouse Buyers