Industrial Grade Medium Duty Pallet Racking: Structural Engineering & Global Supply Chain Masterclass
Modern warehouse architecture demands rigorous optimization of cubic volume, structural load distribution, and operational pick efficiency. As a tier-one China wholesale medium duty pallet racking manufacturer and global exporter, Zenithrack Industrial Equipment delivers custom engineered storage systems built to ANSI MH16.1, FEM 10.2.02, and EN 15512 safety standards. This definitive guide breaks down technical material specifications, structural mechanics, total cost of ownership (TCO), and automated warehousing trends.
Featured Warehouse Storage & Pallet Racking Systems
Precision-manufactured heavy-duty and medium-duty pallet racks, automated radio shuttle bays, structural mezzanines, and gravity flow channels designed for maximum floor efficiency.
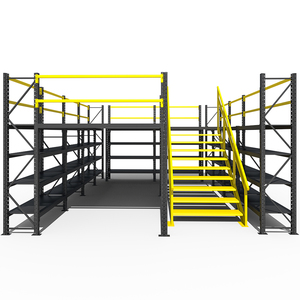
Steel Mezzanine Floor Platform & Multi-Tier Storage Rack
- Doubles overhead cubic storage space
- Heavy load rating: 300 - 1000kg/m²
- Modular staircase & handrail integration
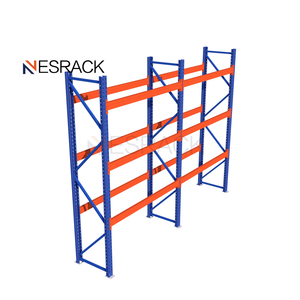
Adjustable Selective Pallet Racking & Steel Shelf System
- 100% immediate SKU accessibility
- 75mm pitch adjustable beam levels
- Cold-rolled high yield steel columns
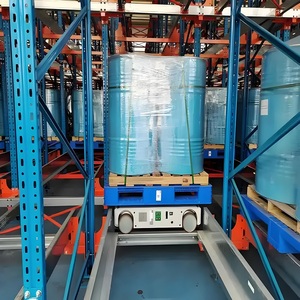
Intelligent Automated 4-Way Radio Shuttle Racking System
- Ultra high density deep lane storage
- WMS integrated autonomous cart movement
- Optimized for cold storage (-25°C)
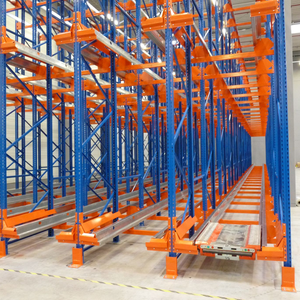
Semi-Automated Logistics Radio Shuttle Storage System
- Supports both FIFO & LIFO operations
- Reduced forklift operational travel time
- Custom rack depth up to 40+ pallets
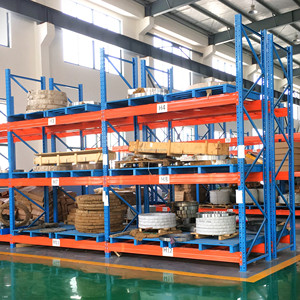
Modular High-Capacity Portable Steel Stacking Racks
- Dynamic stackable layout flexibility
- Removable posts for flat shipping storage
- Ideal for seasonal overflow goods
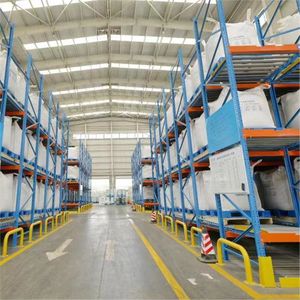
Heavy Duty Dynamic FIFO Gravity Flow Pallet Racking
- Strict First-In First-Out inventory control
- Heavy-duty braking rollers & speed controllers
- Perfect for perishable & FMCG goods
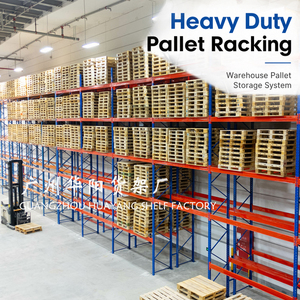
3000KG/Level Heavy-Duty Industrial Pallet Racking
- Reinforced box beam & column profiles
- Epoxy powder coated anti-corrosion finish
- Safety locks prevent accidental beam displacement
Industrial Coil & Cylinder Storage Rack with Raised End Stops
- Specialized cradles for cylindrical stock
- Prevents roll-off accidents with end stops
- Custom load cradles for steel coils/cables
1. Metallurgy & Structural Engineering Mechanics of Medium-Duty Racking
When procuring medium-duty and selective pallet racking systems from China, engineering buyers must evaluate the raw material properties and cold-roll forming geometry. Zenithrack utilizes premium Q235B and Q355B high-tensile cold-rolled steel. The mechanical reliability of upright frames relies on the structural profile design—specifically the multi-bend continuous roll profile which significantly elevates the moment of inertia ($I_x$, $I_y$) and radius of gyration.
Column Buckling Resistance
Upright frame columns undergo rigorous Euler's column buckling analysis under max load. By engineering multi-ribbed side geometry, column slenderness ratios ($\lambda = KL/r$) are kept well within ANSI MH16.1 design limits, mitigating torsional-flexural buckling risks.
Beam Deflection Limits ($L/200$)
Load-bearing horizontal beams are roll-formed into interlocking step beams or closed box profiles. Our design mandate ensures maximum elastic deflection under full rated load does not exceed 1/200th of the clear beam span ($L/200$), preventing permanent plastic deformation.
Safety Locks & Surface Treatment
Connection claws utilize 3 to 4-hook heavy connectors with automatic safety pin locks to stop accidental beam dislodgement from upward forklift impacts. All surfaces undergo a 7-stage phosphating pretreatment followed by thermosetting epoxy powder coating (60–90 μm thickness).
Storage System Architectural Comparison Matrix
Evaluate structural capacity, volumetric density, and operational speed metrics across primary warehouse racking topologies.
| Racking System Type | Load Capacity Range | Volumetric Space Efficiency | SKU Accessibility | Handling Equipment Compatibility | Optimal Application Scenario |
|---|---|---|---|---|---|
| Selective Pallet Racking | 1,000kg – 4,000kg / Level | 40% – 50% Utilization | 100% Immediate Direct Access | Standard Counterbalance / Reach Trucks | High SKU counts, fast-moving 3PL operations |
| Medium Duty Shelf Racking | 200kg – 800kg / Shelf Level | 55% – 65% Utilization | 100% Manual Hand Pick | Manual Totes, Order Pickers, Trolleys | E-commerce fulfillment, spare parts, light cartons |
| Radio Shuttle System | 1,000kg – 1,500kg / Pallet | 75% – 85% High Density | Filo / Fifo Batch Access | Autonomous Shuttle Cart + Forklift | Cold storage, food & beverage, high-volume SKUs |
| Dynamic Gravity Flow Rack | 500kg – 1,500kg / Pallet | 70% – 80% Utilization | Strict FIFO Automatic Rotation | Gravity Roller Lanes & Brake Drums | Perishable goods, pharmaceutical distribution |
| Structural Steel Mezzanine | 300kg – 1,200kg / m² Floor | 100% – 200% Floor Area Gain | Floor & Tier Level Access | Goods Elevators, Pallet Gates, Conveyors | High-ceiling facilities seeking floor expansion |
2. Strategic Procurement & Future Technology Trends (2025–2030)
Global supply chain management is experiencing a paradigm shift driven by automation, space cost inflation, and stringent carbon footprint regulations. Key trends shaping warehouse racking procurement include:
A. Transition from Static to Semi-Automated Racking
Rising warehouse labor costs and real estate prices are pushing global buyers toward hybrid radio shuttle systems and AGV/AMR-integrated racking channels that increase cube storage efficiency by up to 80% without full AS/RS capital investment.
B. Modular & Seismic Structural Design
International building codes (including US RMI and European FEM) now strictly enforce seismic shear baseplate designs, heavy-duty floor anchoring, and dynamic loading safety ratios (1.5 to 1.65) to protect workforce welfare.
C. Sustainable Zero-VOC Coatings & Eco-Steel
Environmental compliance requires zero-solvent powder coating lines that recycle 98% of overspray, alongside fully traceable green steel coil procurement to lower Scope 3 embodied carbon emissions.
Why Zenithrack is the Trusted Partner for Global Importers
Combining 15+ years of real factory production, in-house structural engineering, and rigorous international quality assurance protocols.
Direct China Manufacturer, No Middlemen
Operating an 8,000m² specialized factory equipped with 35 sets of high-precision CNC punching, cold roll-forming lines, and robotic welding stations. Annual revenue exceeds 100M+ RMB with direct factory pricing advantages.
Free Engineering CAD Layouts & 3D Models
Our 75+ member team includes dedicated structural design engineers who evaluate your warehouse floor plan, ceiling clear heights, and forklift turn radiuses to generate zero-cost CAD and 3D installation blueprints.
End-to-End Quality Gates & Testing
From raw coil ultrasonic thickness checks to weld seam magnetic particle testing, coating adhesion cross-hatch tests, and final pre-shipment assembly verification, quality is monitored at every production phase.
Frequently Asked Questions for Storage Racking Buyers
Clear, expert technical answers regarding warehouse racking selection, customization, and factory export logistics.
- Warehouse floor dimensions and building CAD/PDF drawing (highlighting column grid, doors, and fire exits).
- Clear height under the lowest roof truss, lighting fixture, or sprinkler pipes.
- Pallet specifications: width, depth, overall stacked height, and maximum gross load weight per pallet.
- Forklift model, aisle turn radius, and maximum mast lift height.
- Local building seismic zone or environmental operating conditions (e.g., cold room vs standard temperature).
Transform Your Warehouse Storage Efficiency Today
Connect with our senior structural racking engineers for direct factory quotes, custom technical layout designs, and our comprehensive 2025 Product & Technical Spec Catalog.