Featured Industrial Storage Systems
Engineered to comply with international RMI, FEM, and EN standards. Explore our core range of custom OEM selective and high-density warehouse racking lines.
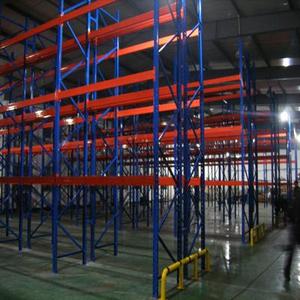
Narrow Aisle Pallet Rack High Density Storage System with Adjustable Beams
Designed for logistics hubs maximizing floor footprint. Features 100% pallet accessibility paired with reduced aisle widths for specialized VNA turret trucks.
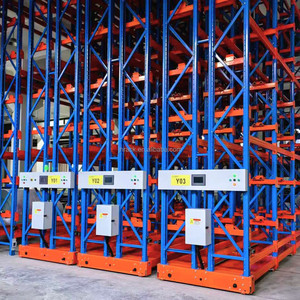
Industrial Heavy Duty High Efficiency Electric Mobile Racking System
Motorized mobile bases moving along embedded floor rails. Eliminates multiple operating aisles to unlock up to 85% higher volumetric capacity.
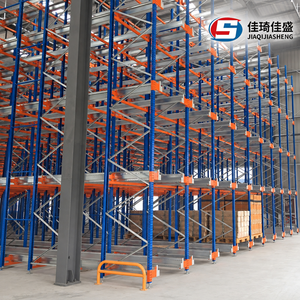
Multi-Level Automatic River-Type Two-Way Radio Shuttle Racking System
Semi-automated deep-lane pallet matrix utilizing intelligent radio-controlled shuttles. Optimized for heavy steel, raw materials, and high-volume SKU rotation.
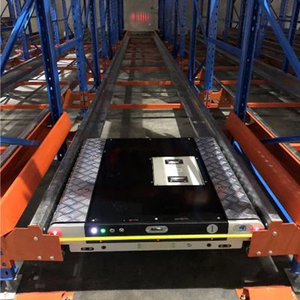
Automated Shuttle Pallet Racking System Two Way Shuttle Solution
High-density dynamic racking system reducing forklift travel times. Supports both FIFO and LIFO dispatch logistics with maximum operational safety.
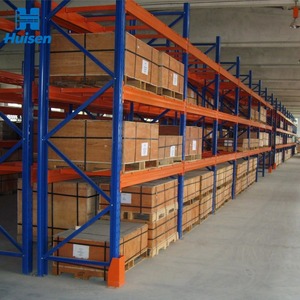
Industrial Heavy Duty Steel Adjustable Multi-Level Warehouse Pallet Rack
The benchmark standard for global distribution centers. Fully customizable beam heights, column gauges, and safety frame connectors for heavy payload flexibility.
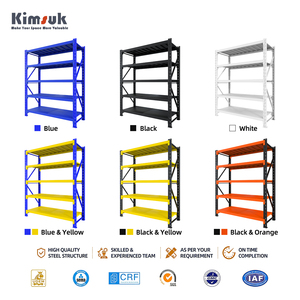
Customized Industrial Heavy Duty Pallet Rack System Metal Storage Shelving
Tailor-engineered structural steel racking configuration. Features modular beam spans, customized powder coat finishes, and optional wire mesh decking.
Jracking Industrial Vertical AU Standard Pallet Racking System
Specifically fabricated to meet AS4084 Australian standards. High rigidity teardrop and box-beam geometry engineered for cold storage and logistics hubs.
Dynamic Storage Pallet Gravity Flow Racking System for Automated Logistics
Utilizes inclined roller tracks and centrifugal brake rollers to deliver seamless FIFO product movement. Ideal for perishable inventory and buffer lanes.
Single Selective Pallet Racking: Technical Architecture & OEM Standards
Single Selective Pallet Racking remains the structural backbone of modern material handling and third-party logistics (3PL) warehousing worldwide. Operating on a direct-access paradigm, single selective racking provides 100% immediate selectivity to every individual stock-keeping unit (SKU) without requiring the reshuffling of adjacent loads. As a premier original equipment manufacturer (OEM) and global exporter, Zenithrack Industrial Equipment Co., Ltd. builds structural single selective systems designed to withstand heavy payload cycling while maintaining extreme dimensional stability across diverse seismic zones.
Metallurgical Integrity & Steel Profiles
Our upright frames are cold-roll-formed from premium certified Q235B and Q355B structural steel coils (equivalent to SS400 and Grade 50 steel). By optimizing column geometry through continuous 13-to-18-stage cold roll forming mills, Zenithrack achieves superior torsional rigidity and exceptional moment resistance.
- Upright Profiles: 80mm, 90mm, 100mm, 120mm, and 140mm front widths with material gauges ranging from 1.8mm up to 3.0mm.
- Beam Components: Interlocking twin-C step beams and box beams manufactured with robotically welded 3-hook or 4-hook connector claws.
- Deflection Tolerances: Formulated strictly under L/200 structural deflection criteria under full rated static payload.
Safety Engineering & Surface Metallurgy
Industrial safety and surface preservation determine the operational lifecycle of a selective racking matrix. Zenithrack applies advanced pre-treatment cleaning and automated electrostatic powder coating processes to ensure longevity in high-humidity or cold-chain facilities.
- Surface Pre-Treatment: 9-stage automatic wash-passivation and iron-phosphate bath removing surface oils and mill scale.
- Coating Performance: 60 to 90-micron thermosetting epoxy-polyester powder finish cured at 200°C for maximum impact resistance.
- Galvanization Option: Continuous hot-dip galvanizing complying with ISO 1461 for chemical storage and sub-zero (-30°C) freezer environments.
Technical Specification Matrix: Standard vs. Heavy-Duty Selective Racking
To assist global procurement leads, rack distributors, and structural engineering consultants, the table below details standard technical benchmarks for single selective pallet rack configurations manufactured in our Dongguan facility:
| Structural Parameter | Standard Duty Specification | Heavy Duty Specification | Custom OEM Capability |
|---|---|---|---|
| Upright Section Width | 80mm / 90mm Column Face | 100mm / 120mm / 140mm Column Face | Up to 160mm engineered profiles |
| Steel Profile Grade | Q235B Cold-Rolled Structural Steel | Q355B High-Tensile Carbon Steel | Custom alloy compliance (AS/NZS 4600) |
| Beam Level Load Capacity | 1,000 kg – 2,500 kg per pair | 2,500 kg – 4,500 kg per pair | Reinforced box beams to 5,500 kg |
| Connector Pitch Options | 50mm & 75mm Pitch (European/Asian) | 76.2mm (3-inch) Pitch / Teardrop (US) | Custom hole pattern punching |
| Frame Height Range | 2,000mm to 6,000mm | 6,000mm to 13,000mm single piece | Splice-welded structures to 24,000mm |
| Compliance Standards | RMI (MH16.1), FEM 10.2.02 | EN 15512, AS 4084-2023 | Full Finite Element Analysis (FEA) reports |
Future Procurement & Technological Trends in Warehouse Racking
Macroeconomic shifts, automated robotics integration, and ESG compliance are reshaping how supply chain directors source pallet racking globally.
1. Hybrid Automation Readiness
Procurement teams are shifting away from rigid static racks toward AMR-compatible and AGV-ready hybrid racking. Traditional single selective layouts are increasingly specified with widened lower bay clearances, floor-guided aisle rails, and integrated sensor reflector brackets to accommodate autonomous mobile robots working alongside standard forklifts.
2. Finite Element Analysis & Seismic Rigidity
With global logistics expanding in earthquake-prone regions, enterprise buyers now require computerized Finite Element Analysis (FEA) testing. Modern sourcing mandates verified structural calculations accounting for dynamic seismic accelerations, ground shear stresses, and rack-to-building anchoring load distributions.
3. Green Supply Chain & Low-Carbon Steel
Environmental, Social, and Governance (ESG) compliance has moved from marketing to contract stipulations. Global exporters must demonstrate eco-friendly manufacturing, zero-VOC powder coatings, closed-loop water treatment facilities, and recyclable raw steel procurement credentials.
4. Total Cost of Ownership (TCO) Shift
Strategic buyers prioritize long-term durability over initial CAPEX cost savings. High-durability beam connectors, heavy-duty floor baseplates, and protective column wrap guards significantly reduce annual maintenance costs caused by accidental forklift impacts.
Enterprise Manufacturing & OEM Capability
Over 15 years of operational excellence in China's industrial hub, delivering factory-direct pricing, engineering expertise, and global logistics execution.
Real Factory Direct
Operating an 8,000 m² state-of-the-art production facility equipped with 35 automated roll-forming and robotic welding suites.
Full OEM Customization
Custom colors, structural dimensions, load profiles, brand labeling, and specialized punching for international contractors.
Free Layout & CAD Design
Our engineering team provides complimentary 2D/3D BIM layout design and structural calculations tailored to your floor plan.
Rigorous Quality Assurance
Multi-stage QC inspecting steel coil chemistry, weld seam integrity, hole-punching accuracy, and powder coat thickness before export.
Frequently Asked Procurement Questions
Direct answers from our senior engineering team to help you evaluate, specify, and import pallet racking systems smoothly.
What structural data is required to obtain a custom racking design and accurate quotation? +
1. Architectural floor plan or CAD drawing showing clear warehouse height, building columns, and door locations.
2. Exact pallet dimensions (Width x Depth x Height including cargo overhang).
3. Maximum gross payload weight per pallet.
4. Forklift truck specifications (Minimum aisle width requirement and maximum mast lifting height).
5. Operating environment conditions (Ambient ambient warehouse vs. cold storage freezer, seismic zone requirements).
How does Single Selective Pallet Racking compare against Narrow Aisle (VNA) and Drive-In systems? +
What international structural design standards do Zenithrack systems comply with? +
Can Zenithrack supply customized beam colors, branding, and OEM hole punching pitches? +
What are the typical manufacturing lead times and ocean export shipping logistics? +
Do you offer free product samples and installation engineering support? +
Ready to Optimize Your Warehouse Storage Space?
Connect directly with our senior racking design engineers. Receive custom CAD layout drawings, structural load calculations, and factory-direct pricing within 24 hours.