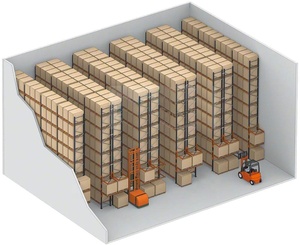
Top 10 Double Row Pallet Racking Factory & Suppliers
Featured Industrial Racking & Storage Systems
Explore engineered pallet racking solutions directly manufactured by certified factory facilities. Built to ISO9001 and international structural engineering compliance (FEM 10.2.02 / RMI).
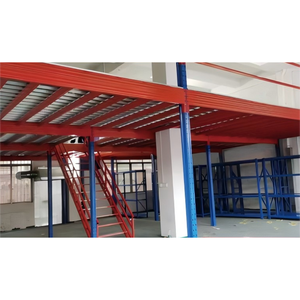
Industrial Steel Mezzanine Floor Racking System Platform Rack Warehouse Shelving Heavy Duty
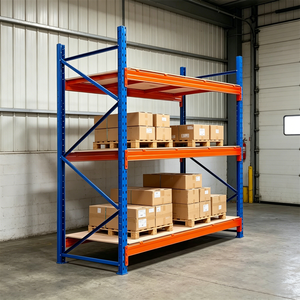
Powder Coated Heavy Duty Rack Industrial Warehouse Storage Pallet Racking Adjustable Industrial Shelves
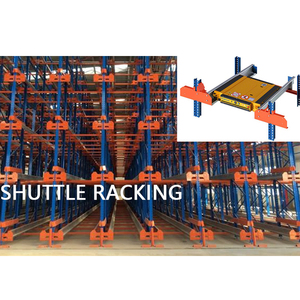
Warehouse High-Density Shuttle Rack System Asrs 4-Way Shuttle Racking Four Way for Storage Shuttle Rack FIFO & LIFO
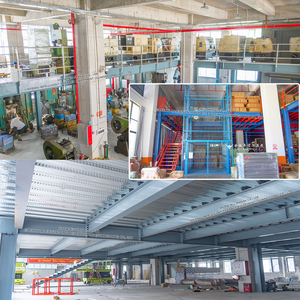
Heavy Duty I-Beam Steel Structural Platform Mezzanine Floor Rack for Industrial Warehouse Storage Factory
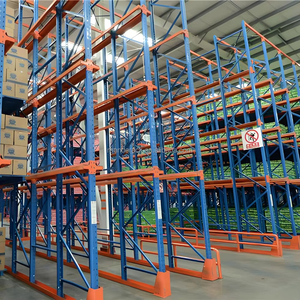
Drive Through Racking System Heavy Duty Drive-in Pallet Rack for Warehouse Storage
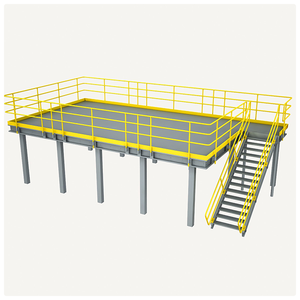
Assembled Metal Heavy Duty Multi Tier Storage Steel Floor Mezzanine Platform System Pallet Rack Supported Mezzanine
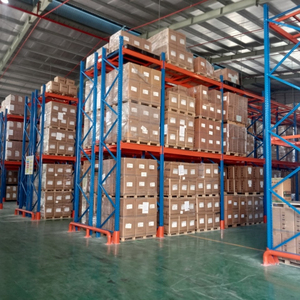
Wholesale Heavy Duty Selective Pallet Racking System Designed for Easy Pallet Access and Reliable Cold Storage Applications
15+
Years Engineering Expertise
8,000m²
Modern Production Base
35+
Automated Roll-Forming Lines
100M+
Annual Turnover (RMB)
Executive Summary: Navigating Double Row Pallet Racking Sourcing
In modern industrial logistics, maximizing floor space utilization while preserving high throughput velocity is the primary directive for supply chain directors. Double Row Pallet Racking (frequently referred to in structural engineering as Double Deep Pallet Racking) offers a strategic middle ground between 100% accessible Single Selective Racking and Ultra-High-Density Drive-In or Automated Storage Systems (AS/RS).
By placing two rows of selective racking back-to-back, double row systems require specialized deep-reach pantograph forklifts or specialized material handling equipment. This configuration reduces overall operating aisle requirements by 50% compared to traditional single-selective configurations, yielding a floor space optimization increase of 30% to 55% depending on total ceiling clearance height.
Key Mechanics of Double Row Structural Design
Engineered with heavy-duty cold-rolled steel structural upright profiles (utilizing Q235B or high-strength Q355B structural grade steel), double row pallet racking systems must withstand eccentric loading forces caused by extended pantograph forklift reach. The critical structural parameters include:
- Structural Back-to-Back Row Connectors: Rigid heavy-gauge steel ties configured every 1.5 to 2 meters along upright heights to prevent longitudinal sway and ensure system rigidity.
- Beam Deflection Safety Factors: Manufactured strictly within L/200 deflection thresholds under full rated load capacity to maintain safe extended pantograph entry.
- Guide Rails & Base Angle Deflectors: Integrated floor-anchored steel guide angles that assist reach truck positioning in deep aisles, minimizing column strike hazards.
Technical Evaluation Criteria for the Top 10 Double Row Racking Suppliers
When enterprise buyers evaluate global manufacturers for heavy-duty racking infrastructure, selecting a verified manufacturing factory over an unverified broker or trading intermediary is crucial. Below is the framework used by top structural engineers to benchmark supply chain partners:
| Evaluation Criterion | Industry Baseline Standard | Top 10 Factory Benchmark (Zenithrack Standard) | Procurement Impact |
|---|---|---|---|
| Steel Grade & Yield Strength | Commercial Grade Q195 / Q235 Steel | Certified Cold-Rolled Q235B & Q355B High-Yield Steel | +25% structural load capacity per shelf beam level |
| Structural Compliance | Basic Local Standards | RMI (USA), FEM 10.2.02 (EU), AS4084-2012 (Australia) | Compliance with global seismic & building codes |
| Surface Finish Technology | Manual Spray Painting (30-40 µm) | Automatic Electrostatic Powder Coating (60-80 µm) | Anti-corrosion lifecycle extended to 15+ years |
| Quality Control Testing | Random Visual Spot Check | Full Structural Load-Cell Testing & Ultrasonic Weld Inspection | Zero structural failure guarantee under rated loads |
| Engineering CAD/BIM Support | Paid Third-Party Layouts | In-House Free Structural CAD & 3D Warehouse Simulation | Optimal space planning & zero site fitment errors |
Selecting top-tier double row racking suppliers involves strictly auditing structural raw material certificates (MTCs), roll-forming precision tolerances, and automated robotic welding lines. Advanced manufacturing plants utilize continuous roll-forming mills equipped with dynamic optical sensor controls to ensure pitch-punching accuracy within ±0.2mm tolerances.
High Cube Density
Doubles pallet capacity per aisle by eliminating half of the operating access lanes required by standard single-entry pallet racks.
Optimized LIFO Inventory
Ideal for fast-moving consumer goods (FMCG), cold storage, and bulk distribution storing multiple pallets of identical SKUs.
Structural Safety Factor
Configured with robust seismic bracing, heavy upright column guards, and back-to-back structural spacers for maximum stability.
Future Procurement & Technology Trends in Double Row Racking (2025–2030)
As global supply chains transition toward automation and data-driven material handling, double row pallet racking systems are undergoing technological upgrades to align with Smart Logistics 4.0 standards. Key procurement trends shaping the market include:
1. Automated Guided Vehicle (AGV) & Autonomous Mobile Robot (AMR) Integration
Traditional deep-reach forklifts operated by human drivers are increasingly complemented or replaced by autonomous pantograph reach AMRs. These automated reach trucks rely on precision laser guidance (SLAM technology), demanding that racking manufacturers maintain extremely strict tolerances on beam straightness, vertical column plumbness, and ground floor anchoring.
2. IoT-Enabled Structural Health & Load Strain Monitoring
Leading industrial logistics hubs are integrating wireless strain gauge sensors and optical impact detectors directly into rack uprights. These smart sensors stream continuous stress dynamic load data to warehouse management software (WMS), alerting facilities management instantly if an upright suffers forklift impact or dangerous overload condition.
3. Eco-Friendly Green Manufacturing & Zero-VOC Coatings
With stringent global carbon footprint regulations (such as the EU's CBAM), tier-1 racking manufacturers are adopting closed-loop powder coating lines that recycle over 98% of oversprayed powder and use non-toxic, zero-VOC thermoplastic polyester finishes. Furthermore, factories utilizing green hydrogen-refined steel profiles provide verified Environmental Product Declarations (EPDs) for global project bids.
4. Hybrid High-Density Configuration (Double Deep + Shuttle Systems)
Modern distribution warehouses are increasingly blending double-deep selective rack levels with radio shuttle automated channels on higher tiers. This hybrid approach enables high SKU variety on lower picking levels while maximizing high-bay cube storage for overstock pallets.
Enterprise Capability Profile: Zenithrack Industrial Equipment
As a leading Chinese racking manufacturer with more than 15 years of dedicated engineering experience, Zenithrack Industrial Equipment Co., Ltd. stands at the forefront of high-density warehouse storage innovation. Operating from an expansive 8,000 square meter modern manufacturing facility equipped with over 35 sets of high-precision roll-forming and welding machinery, Zenithrack delivers factory-direct heavy-duty racking solutions to over 50 countries worldwide.
Factory-Direct Pricing
By eliminating middleman margins, Zenithrack offers raw-material indexed direct pricing with full OEM/ODM structural customization.
In-House QC & Testing
Dedicated quality inspectors verify steel raw materials, profile dimensions, weld seam integrity, and coating thickness at every production stage.
Free CAD & 3D Engineering Design
Senior structural engineers provide complimentary layout designs, seismic structural calculations, and 3D rendering within 24 hours.
Free Samples & Tooling Support
Test beam profile sections, upright connectors, and surface finishing first-hand with complimentary samples prior to full-container ordering.
Custom Branding & OEM Colors
Complete private labeling, custom RAL powder-coat colors, and customized installation documentation for global rack distributors.
Rapid Export Delivery
High-capacity automated cold roll-forming lines ensure fast turnaround times for large multi-container industrial logistics projects.
Frequently Asked Questions (FAQ) - Double Row Pallet Racking Procurement
Engineered answers to common questions asked by supply chain executives, warehouse logistics managers, and industrial procurement specialists.
How do I choose between selective, drive-in, double deep, and radio shuttle racking?
Choose Selective Pallet Racking when you handle high SKU counts requiring 100% immediate pallet access. Choose Double Row / Double Deep Racking when you want to increase density by 30-50% while storing 2 to 4 pallets per SKU using deep-reach trucks. Choose Drive-In Racking for low SKU counts stored in massive bulk quantities where Last-In-First-Out (LIFO) is acceptable. Choose Radio Shuttle Racking when you require maximum storage density, semi-automated handling speed, and flexible FIFO/LIFO operation.
What equipment is required to operate a Double Deep Pallet Racks system?
Double deep pallet racking requires a specialized double-deep reach truck equipped with a dual-pantograph mechanism or telescopic forklift tines. Additionally, camera-assisted fork tips and height-guided laser positioning systems are strongly recommended to facilitate smooth pallet placement into the secondary (rear) row position at heights above 6 meters.
What technical information is required for Zenithrack to design a free layout?
To generate an accurate structural CAD drawing and load profile, our engineering team requires:
1. Warehouse building floor plan or CAD drawing (showing column locations, building doors, and obstructions).
2. Clear building height under roof beams or sprinkler lines.
3. Pallet dimensions (Length x Width x Height including load) and maximum weight per pallet.
4. Reach truck model specifications, minimum aisle width requirement, and maximum lifting height.
5. Local seismic zone conditions or environmental cold-storage requirements.
How does Double Deep Racking impact inventory management (FIFO vs LIFO)?
Double deep racking naturally operates on a Last-In, First-Out (LIFO) inventory flow per slot, as the rear pallet cannot be accessed until the front pallet is removed. However, by managing pallet pairs of identical SKUs or utilizing automated WMS software batching, warehouses can effectively operate a managed FIFO system across multiple bays.
What structural safety components are installed on double row pallet racks?
Double deep systems are fitted with rigid back-to-back row connectors, heavy-duty frame column guards, guide rails for reach trucks, structural horizontal and diagonal frame bracing, and rear pallet safety stops (push-through preventers) on beam levels to ensure pallets do not push rearward into opposing rows.
Can double row pallet racks be customized for cold storage operations?
Yes. Zenithrack customizes double deep systems for cold storage environments down to -30°C using specialized low-temperature carbon structural steel and durable hot-dip galvanized or specialized epoxy powder coatings that resist condensation and corrosion.
Ready to Optimize Your Warehouse Storage Density?
Contact our senior structural racking engineers today for a complimentary warehouse evaluation, custom CAD layout drawing, and direct factory pricing quote.