Spotlight Racking & Automated Pallet Systems
Engineered to precision standards for high-density logistics, heavy manufacturing, cold storage, and modern distribution centers.
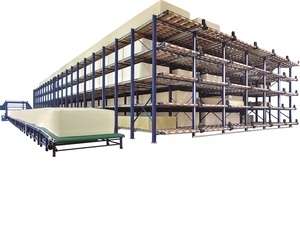
Foam Block Rack Storage System
Custom engineered heavy-duty racking designed specifically for bulky, low-density materials and industrial foam blocks with anti-sagging deck integration.
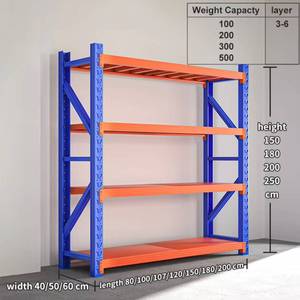
Extra Layer Heavy Duty Pallet Rack Storage Shelf
High-load multi-level warehouse racking featuring adjustable beam positions, certified Q355B cold-rolled steel posts, and structural safety locking mechanisms.
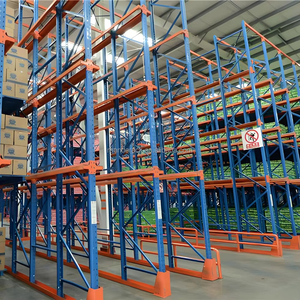
Heavy Duty Drive-Through & Drive-In Racking
Maximizes floor utilization up to 85% by eliminating picking aisles. Ideal for uniform inventory, high-volume batch production, and cold storage applications.
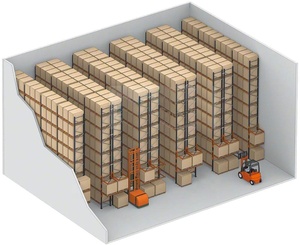
URGO Very Narrow Aisle (VNA) Pallet Racking
Precision-engineered high-bay storage operating in narrow aisles down to 1.5m. Combines 100% selective pallet access with maximum ceiling height footprint utilization.
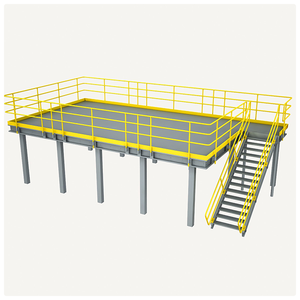
Assembled Heavy-Duty Multi-Tier Mezzanine Platform
Rack-supported industrial mezzanine floor systems that double or triple usable vertical facility area without structural expansion costs.
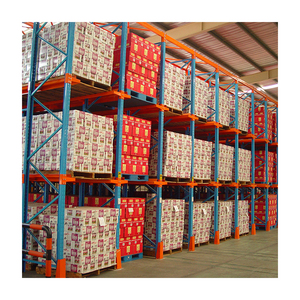
Customized Industrial Multi-Tier Drive-In System
Direct factory-priced high-density drive-in storage featuring reinforced upright frames, structural top bracing, and heavy-gauge pallet rail channels.
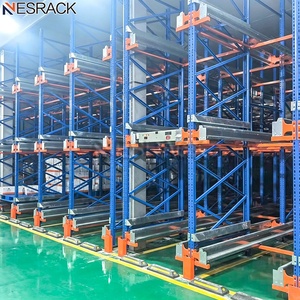
Remote-Controlled Radio Shuttle Pallet Racking
Semi-automated deep-lane storage system utilizing wireless shuttle carts to transport pallets within deep channels. Supports both FIFO and LIFO operational logic.
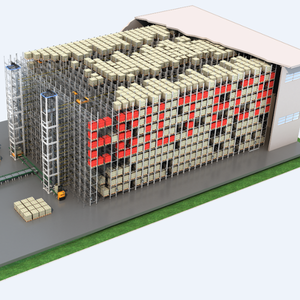
EBIL-ZMC High-Speed Satellite Shuttle Racking
Advanced automatic racking solution featuring high-speed 160m/min satellite shuttle cars, 380V power systems, and real-time WMS integration capability.
System Performance & Spatial Optimization Benchmark
Quantitative analysis comparing traditional pallet storage with semi-automated radio shuttle and fully automated AS/RS infrastructures.
Technical Comparison Matrix: Intelligent Pallet Storage Ecosystems
Selecting the optimal warehouse racking framework requires balancing capital expenditure (CAPEX), SKU diversity, throughput requirements, and spatial footprint flexibility. The table below outlines key parameters evaluated by logistics project engineers during warehouse design phases:
| Racking Architecture | Storage Density Index | SKU Selectivity | Forklift Dependency | Operational Logic | Optimal Facility Type |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | High (Manual Entry) | FIFO / LIFO | 3PL, FMCG Multi-SKU Hubs |
| Drive-In / Drive-Through | High (65-75%) | Low (Lane Restricted) | High (Driver inside lane) | LIFO (Drive-In) / FIFO | Cold Storage, Bulk Goods |
| Very Narrow Aisle (VNA) | High (70-80%) | 100% Direct Access | Specialized VNA Trucks | FIFO / LIFO | High-Bay E-Commerce Warehouses |
| Radio Shuttle System | Very High (80-88%) | Medium (Channel Level) | Low (Shuttle Handles Lane) | FIFO or LIFO Selectable | Food & Beverage, Chemicals |
| Automated AS/RS Crane Racking | Maximum (90-95%) | 100% Automated Access | Zero (Robot Stacker Cranes) | Fully Software Controlled | Smart Manufacturing 4.0 Hubs |
Future Development of Intelligent Pallet Storage Systems
Market intelligence analysis on technological advancements, structural engineering compliance, and supply chain automation trends through 2030.
1. Shift from Static Storage to Autonomous Dynamic Material Handling
The global warehousing landscape is undergoing a structural transition from static palette rack structures to dynamic, self-orchestrating storage environments. Industrial facilities face accelerating labor costs, localized land supply constraints, and demanding omnichannel fulfillment SLAs. As a response, global procurement managers are moving away from basic selective rack configurations and investing heavily in Semi-Automated Radio Shuttle Systems and Four-Way Shuttle AS/RS Platforms.
Modern radio shuttle satellites now incorporate IoT sensor arrays, LiDAR obstacle detection, and long-life Lithium Iron Phosphate (LiFePO4) battery modules capable of 16-hour continuous operation under harsh sub-zero cold chain conditions (-30°C). By converting conventional aisle space into dense storage matrixes, enterprise buyers achieve immediate spatial efficiency gains of 60% to 85% without altering building footprints.
2. Advanced Material Science & Structural Seismic Resilience Standards
Structural reliability remains the primary benchmark for warehouse safety and compliance. Top international manufacturers and exporters have aligned structural calculations with recognized international standards, including ANSI MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks), FEM 10.2.02 (European Racking Code), and EN 15512.
High-yield cold-rolled steel (specifically Q355B grade high-strength steel alloy) has replaced traditional Q235 steel in heavy-duty rack upright profiles. The structural geometry of teardrop and omega-section posts has been optimized through Finite Element Analysis (FEA) testing. This ensures dynamic deflection factors do not exceed L/200 under maximum rated payload, providing structural stability against seismic forces, mechanical forklift impacts, and accidental overloads.
3. WMS/WCS Software Integration & Real-Time Telemetry
Intelligent racking is no longer static physical steel; it is a live data node within the enterprise logistics network. Leading suppliers now offer pallet shuttle systems equipped with onboard Wi-Fi 6 / 5G industrial communication cards that seamlessly interface with Enterprise Resource Planning (ERP), Warehouse Management Systems (WMS), and Warehouse Control Systems (WCS).
Through real-time telemetry, facility operators track inventory location, batch movement, battery health metrics, shuttle velocity, and automated stock count reconciliation. This integration eliminates human picking errors, reduces warehouse inventory cycle audit costs by up to 90%, and supports FIFO (First-In, First-Out) compliance critical for pharmaceutical, food safety, and chemical manufacturing sectors.
Zenithrack Industrial Equipment: Manufacturing Pioneer
15+ years of structural steel manufacturing leadership, real factory infrastructure, and comprehensive export capabilities.
Engineering Excellence & Production Infrastructure
Zenithrack Industrial Equipment Co., Ltd. (headquartered at 15 Yinhu 2nd Road, Shishuikou, Qiaotou Town, Dongguan, Guangdong, China) is a top-tier Chinese racking manufacturer specializing in engineered warehouse storage solutions. Operating an advanced 8,000 m² modern production facility equipped with 35 sets of specialized machinery, Zenithrack has grown into a leading industry exporter with annual domestic and international sales exceeding CNY 100 million.
Unlike trading intermediaries, Zenithrack maintains full control over raw steel procurement, continuous cold-roll forming, automated robotic welding, precision hole punching, and high-durability electrostatic epoxy powder coating lines. Supported by an experienced team of 75+ structural engineers, CAD draftspersons, and certified QC inspectors, every system is custom-manufactured to match specific floor loading parameters and operational workflows.
Strict Multi-Stage Quality Control Protocol
To deliver structural reliability across thousands of global warehouse installations, Zenithrack executes a rigid 4-stage Quality Management System (QMS):
- Raw Material Inspection: Chemical composition and tensile yield strength testing of raw cold-rolled steel coils upon arrival from top-tier steel mills.
- Roll-Forming & Dimensional Verification: Real-time laser micro-caliper checking of upright profile pitch, beam hook tabs, and hole-center tolerances.
- Robotic Welding Integrity: Continuous seam welding inspection utilizing ultrasonic flaw detectors to prevent fatigue fractures under rated load stress.
- Surface Treatment & Coating Adhesion: Multi-stage chemical degreasing, phosphating, and electrostatic powder coating cured at 200°C for superior corrosion, abrasion, and moisture resistance.
Proven Track Record & Global Enterprise Clients
Zenithrack's engineered pallet racking solutions have been successfully deployed by market leaders across automotive, third-party logistics, consumer electronics, and heavy industry sectors. Major global enterprises relying on Zenithrack storage infrastructure include BYD Auto, FedEx Express, SF Express, Huawei Technologies, Cooper Tire, Foxconn, and Midea Group.
International Warehouse Racking Procurement Guide
Essential engineering data points required when requesting custom rack quotes and warehouse layout designs.
5-Point Technical Checklist for RFQ Submission
To ensure your layout drawing and load calculations are executed accurately, provide the following parameters to the manufacturing engineering team:
- Building Architectural Drawings: CAD (.dwg / .pdf) floor plan showing warehouse dimensions, column grid centers, building apex/eave height, slab thickness, and door/fire hydrant locations.
- Pallet Load Profiles: Exact pallet dimensions (Width x Depth x Height including cargo overhang), maximum gross pallet weight, and target palette position capacity.
- Material Handling Equipment (MHE) Specs: Forklift model, minimum turning aisle width requirement, maximum lift height capability, and mast collapsed height.
- Environmental Operating Conditions: Ambient temperature range (ambient, cold storage, or deep freeze down to -30°C), indoor vs. outdoor setup, and humidity/corrosion exposure.
- Regulatory & Seismic Codes: Local building authority requirements, fire sprinkler line clear heights, and localized seismic zone rating factor ($S_s$ / $S_1$).
Frequently Asked Procurement Questions (FAQ)
Detailed technical answers addressing logistics engineering, manufacturing lead times, export packing, and OEM customization.
How do I choose between selective pallet rack, drive-in rack, and radio shuttle racking systems?
Selective Pallet Racking is the industry standard when storing a high number of distinct SKUs, as it offers 100% direct access to every single pallet position. However, it requires multiple aisles, resulting in lower spatial density (40-50% floor utilization).
Drive-In Racking eliminates aisles by allowing forklifts to drive inside long storage lanes. It is highly cost-effective for low-SKU, high-volume operations utilizing LIFO (Last-In, First-Out) inventory rotation, though forklift movement inside lanes increases risk of frame impact damage.
Radio Shuttle Racking provides the highest density (up to 85% floor utilization) with maximum safety. The forklift remains outside the rack structure while semi-automated wireless shuttles transport pallets deep inside storage channels. It supports both FIFO and LIFO operational logic, significantly speeds up picking cycles, and minimizes structural damage risks.
What information is required to receive a free custom 3D layout drawing and engineering quote?
Our engineering team requires five core inputs to calculate beam deflection, upright post profiles, and spatial layouts:
- Warehouse floor plan or CAD drawing indicating building dimensions, clear height, and column locations.
- Pallet dimensions (Length × Width × Cargo Height) and gross weight per pallet.
- Maximum lift height and aisle radius required by your current forklift equipment.
- Target inventory storage capacity (total required pallet positions).
- Special operating environments such as cold storage (-30°C), outdoor anti-corrosion requirements, or high seismic rating zones.
Does Zenithrack offer OEM manufacturing, custom frame colors, and private branding?
Yes. Zenithrack provides comprehensive OEM and ODM manufacturing services for international storage equipment distributors, system integrators, and industrial rack contractors. We offer full customization of post profiles, beam sizes, load-bearing capacities, custom RAL powder coating colors (e.g., Signal Blue RAL 5005, Pure Orange RAL 2004, Pebble Grey RAL 7032), and specialized private-label brand packaging.
How are structural components packaged to prevent damage during overseas container shipping?
Export packaging is engineered for long-distance maritime transport. Upright frames and heavy beams are bundled using high-tensile steel strapping, wrapped in protective bubble film, and supported by heavy-duty timber skid bases to facilitate seamless unloading via forklift. Smaller hardware components, safety locks, footplates, and bolts are packed in heavy-gauge wooden crates or reinforced corrugated cartons.
What quality assurance guarantees and international certifications cover Zenithrack storage systems?
All Zenithrack storage systems are manufactured in compliance with ISO 9001 Quality Management Systems and engineered according to FEM 10.2.02 and ANSI MH16.1 structural steel standards. Raw cold-rolled steel materials are fully certified with mill test reports (MTR). We provide a 5-year structural warranty on racking frames and offer free replacement parts for non-conforming manufacturing items.
Transform Your Warehouse Spatial Economics Today
Consult with Zenithrack’s senior structural engineers to receive a free, zero-obligation custom CAD layout, engineering load calculation, and factory-direct price quotation within 24 hours.