Industrial Bulk Storage Pallet Racking Systems
Explore our high-load capacity racking solutions precision-engineered for heavy manufacturing, cold storage, 3PL logistics hubs, and automated distribution facilities.
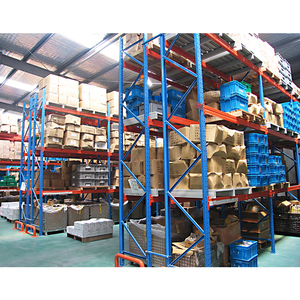
Standard Pallet Rack Heavy Duty Warehouse Racking System
Fully customizable structural beam racking featuring 100% direct pallet accessibility, adjustable 75mm pitch levels, and structural steel capacity up to 4,500kg per level.
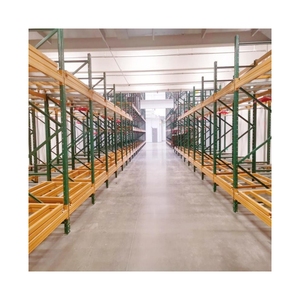
Custom Push Back Pallet Racking With Precision Guide Rail
High-density LIFO storage solution utilizing nested wheeled carts running on inclined rails. Maximizes depth up to 6 pallets deep per lane without forklift intrusion.
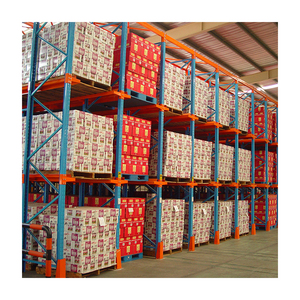
Factory Price Drive-in Rack Multi-tier Through Racking System
Eliminates operating aisles to double warehouse storage space. Designed for bulk storage of homogeneous stock under heavy-duty loading requirements.
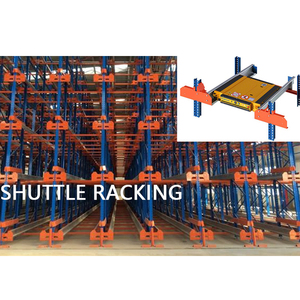
High-Density ASRS 4-Way Radio Shuttle Racking System
Semi-automated radio shuttle solution engineered for automated FIFO/LIFO inventory management with extreme volumetric floor space optimization.
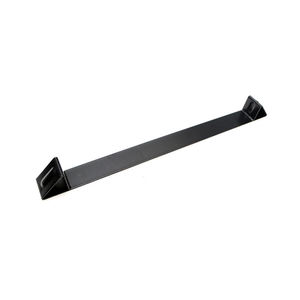
Industrial Coil Storage Rack with Raised Mechanical End Stops
Engineered specifically for cylindrical goods, steel coils, and heavy paper rolls. Features heavy-duty saddle cradles and engineered end retainers for workplace safety.
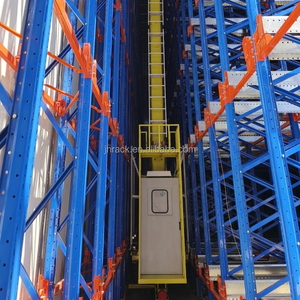
Intelligent ASRS Chain Pallet Conveyor System & Storage Rack
Fully integrated automated storage and retrieval system (AS/RS) combining structural high-bay racks with automated chain and roller pallet transfer conveyors.
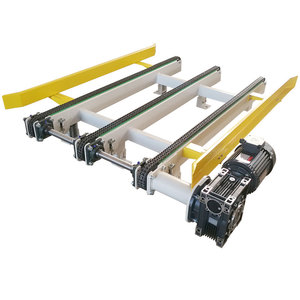
Heavy-Duty Automated Pallet Chain Conveyor Transport System
Industrial-grade automated chain conveyor modules designed for seamless integration between staging bays, high-density racking, and packing stations.
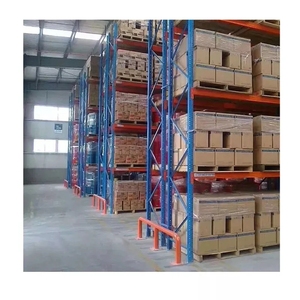
Heavy Duty Adjustable Metal Shelving & Pallet Stacking System
Versatile hybrid racking system supporting both direct pallet placement and steel wire mesh or steel deck shelving for multi-purpose bulk warehousing.
Engineering Architecture of China Bulk Storage Pallet Racking Systems
In the contemporary global logistics landscape, selecting the right bulk storage pallet racking manufacturer in China requires an in-depth understanding of structural engineering, metallurgical standards, surface finish longevity, and seismic resilience. As warehouse floor space commands premium leasing rates across North America, Europe, and Asia-Pacific, industrial operations must pivot toward optimized vertical cubic utilization without compromising structural integrity or operator safety.
Leading Chinese racking manufacturers like Zenithrack Industrial Equipment Co., Ltd. have evolved beyond traditional fabrication into sophisticated engineering entities. Modern bulk storage systems utilize structural Q235B and high-yield Q355B cold-rolled steel profiles, customized beam connector geometries, and automated robotic continuous seam welding to satisfy stringent international design standards, including ANSI MH16.1 (RMI), FEM 10.2.02, and AS4084-2012.
Metallurgical Integrity: Q235B vs. Q355B Cold-Rolled Steel Profiles
The structural reliability of heavy-duty pallet racking hinges directly on steel coil grain uniformity and yield strength metrics. Leading manufacturers utilize high-precision cold roll-forming lines to process structural upright columns and interlocking step beams:
- Q235B Carbon Structural Steel: Yield strength ≥ 235 MPa, Tensile strength 370–500 MPa. Ideal for standard selective pallet racking, medium-duty shelving, and non-seismic storage configurations.
- Q355B High-Strength Alloy Steel: Yield strength ≥ 355 MPa, Tensile strength 470–630 MPa. Specified for heavy-duty structural uprights, high-bay ASRS structures, cantilever arms, and seismic-rated installations where high strength-to-weight ratios prevent beam deflection.
| Racking Architecture | Primary Material Grade | Maximum Load / Level | Aisle Space Efficiency | Recommended Access Mode |
|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B Structural Steel | 1,000 kg – 4,500 kg | Standard (40% - 50%) | 100% Direct Forklift Access |
| Drive-In / Drive-Through | Q355B High-Yield Steel | 1,500 kg / Pallet Position | High Density (65% - 75%) | LIFO (Drive-In) / FIFO (Drive-Thru) |
| Radio / 4-Way Shuttle ASRS | Q355B Precision Structural Steel | 2,000 kg / Shuttle Unit | Ultra-High Density (80% - 90%) | Automated FIFO / LIFO Carrier |
| Heavy-Duty Cantilever Racking | Q355B Hot-Rolled H-Beam | 500 kg – 3,000 kg / Arm | Specialized (Unobstructed Front) | Side-Loader / Crane / Forklift |
| Structural Steel Mezzanine | Q355B Hot-Rolled Steel Columns | 300 kg – 1,500 kg / m² | Multiplies Floor Area 2x – 3x | Manual / Trolley / AGV Platform |
Technological Classifications of Bulk Storage Racks
High-Bay Selective Racking
Engineered with multi-cladding diamond-punched uprights and custom box-beam profiles. Provides instant access to every SKU, rendering it the benchmark for general warehousing, 3PL logistics centers, and FMCG operations.
Radio Shuttle ASRS Systems
Integrates automated battery-powered shuttles inside deep storage channels. Reduces forklift drive times, accelerates throughput speeds by 40%, and mitigates rack collision damage in high-turnover cold storage environments.
Drawer-Type Industrial Mold Racks
Heavy-duty mold storage platforms engineered with slide-out drawers, safety self-locking pins, and overhead crane integration. Capable of supporting up to 3,000kg per shelf level for plastic injection tooling.
Future Procurement & Technology Trends in Warehouse Pallet Racking
As global supply chains navigate supply volatility, automation bottlenecks, and strict ESG compliance standards, warehouse racking procurement is undergoing a fundamental transformation. Procurement directors are shifting focus from simple hardware purchase costs to Total Cost of Ownership (TCO), operational agility, and environmental sustainability.
1. Transition to 4-Way Shuttle ASRS and Autonomous Mobile Robot (AMR) Integration
Traditional static storage racks are increasingly being replaced by semi-automated and fully automated 4-way shuttle systems. Unlike standard 2-way shuttle systems that operate solely along a single aisle axis, 4-way shuttles can traverse both longitudinal and transverse channels. This allows for dynamic load balancing, direct rack-to-conveyor transfer, and footprint space utilization exceeding 85%.
2. Eco-Friendly Electrostatic Powder Coating & Zero-VOC Surface Finishing
Environmental regulations in China have driven top-tier pallet rack factories to invest in state-of-the-art automatic electrostatic powder coating lines. Utilizing zero-VOC epoxy polyester thermosetting powders, current surface treatments achieve coating thicknesses of 60–90 microns, enduring over 500 hours of continuous salt spray testing (ASTM B117) to prevent rust in high-humidity or cold storage environments.
3. Modular Structural Steel Mezzanines with AGV Decking
Modern e-commerce fulfillment hubs require high-capacity floor surfaces capable of enduring repetitive rolling wheel loads from Autonomous Mobile Robots (AMRs). Chinese manufacturers are leading the design of cold-formed structural steel mezzanines reinforced with anti-slip galvanized steel floor decking, offering uniform distributed loads up to 1,500 kg/m².
Factory Direct Manufacturing & Quality Control
Located in Dongguan, China, Zenithrack Industrial Equipment Co., Ltd. operates as a premier direct racking factory, offering customized structural design, rigorous quality control, and rapid export fulfillment.
8,000 m² Advanced Production Hub
Equipped with 35 sets of specialized machinery including automated CNC roll-forming machines, laser tube cutters, continuous robotic welding cells, and an automated powder coating line.
In-House Engineering & Free CAD Layouts
Our dedicated team of 75+ professionals includes structural engineers who deliver customized 2D CAD warehouse floor layouts and 3D FEA stress simulation analysis free of charge within 24 hours.
Rigorously Audited Quality Assurance
Every shipment undergoes full stage-gate quality control: steel coil raw material certification, profile wall thickness verification, weld penetration testing, and surface adhesion testing before container loading.
Full OEM / ODM Brand Customization
We empower international racking distributors and system integrators with custom color powder coating (RAL system), bespoke beam connector tooling, and private-label branding on hardware accessories.
Frequently Asked Questions on Pallet Racking Sourcing
Expert answers to common engineering, quality control, shipping, and installation queries encountered when purchasing bulk warehouse racks from China.
How do I choose between selective pallet rack, drive-in racking, and radio shuttle ASRS?
What crucial information is needed for Zenithrack engineers to design a free CAD layout?
- Architectural warehouse floor plan (CAD or PDF) showing column locations, building clear height, dock doors, and obstruction points.
- Pallet dimensions (Width x Depth x Load Height including wooden pallet) and maximum gross weight per pallet.
- Forklift operational specs: turning radius, mast lift height, and aisle width requirement.
- Environmental conditions (ambient, cold room, chemical storage, or seismic requirements).
What international structural standards do Zenithrack pallet racks conform to?
Do you supply physical steel samples and custom installation drawings?
How are pallet rack components packaged to prevent damage during sea transport?
Can racks be customized to meet specific corporate colors or private label branding?
Ready to Optimize Your Warehouse Storage Capacity?
Connect directly with our senior structural racking engineers today. Receive a customized 2D CAD layout, load-capacity assessment, and direct factory price quote within 24 hours.
Send an Inquiry