Featured Mobile & Heavy-Duty Storage Systems
Factory-direct warehouse racking engineered for extreme load durability, modular scalability, and flawless logistical operation.
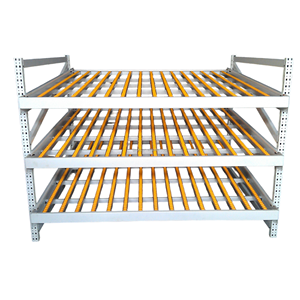
1. Technical Executive Summary: The Industrial Evolution of Mobile Pallet Racking
As modern global supply chains face mounting pressures driven by soaring industrial real estate prices, labor shortages, and energy efficiency demands, logistics infrastructure must adapt. Traditional static racking systems—while straightforward—demand multiple operational aisles that consume up to 60% of total warehouse floor footprint. Mobile Pallet Racking (commonly referred to as Motorized Mobile Racks or Heavy-Duty Portable Stacking Converter Racks) represents a paradigm shift in high-density material handling technology.
By mounting heavy-duty selective pallet racks onto motorized chassis or engineered rolling bases that traverse embedded floor rails, mobile pallet racking condenses multiple conventional aisles into a single operational access bay. When integrated into cold storage facilities, automotive spare-parts hubs, or high-throughput manufacturing plants, mobile racking elevates cubic space utilization to over 85% while preserving 100% direct access to every single SKU.
High Density Storage
Eliminate redundant access aisles. Maximize storage volume per cubic meter in high-bay distribution centers.
100% Selective Access
Unlike drive-in or push-back systems, mobile racking allows instant, direct forklift picking for any pallet location.
Automated PLC Control
Equipped with Siemens/Schneider PLC microprocessors, optical safety curtains, and remote radio frequency dispatch.
2. Structural Engineering Standards & Material Selection Principles
When engineering high-bay mobile racking systems, structural integrity under dynamic rolling loads is non-negotiable. As a leading manufacturer based in Dongguan, China, Zenithrack enforces strict metallurgic and structural compliance adhering to European FEM 10.2.07 standard, American RMI (Rack Manufacturers Institute) guidelines, and Chinese GB/T 28543-2012 specifications.
2.1 Raw Material Integrity (Q235B vs. Q355B Structural Steel)
The performance of any mobile rack hinges on the yield strength of its cold-formed profiles. Lower-tier suppliers often substitute structural steel with commercial grade Q195 steel, risking systemic frame deflection over time. Zenithrack utilizes prime cold-rolled steel coils supplied exclusively by Baosteel and Shougang Group.
- Upright Columns: Manufactured using Q355B (equivalent to S355JR / ASTM A572 Grade 50) high-tensile alloy steel. This delivers a yield strength exceeding 355 MPa, ensuring resistance to torsional forces when mobile bases accelerate or decelerate.
- Box Beams: Fabricated using twin C-section profiles interlocking with automatic robot-welded beam connectors. Safety locking pins (claw connectors) prevent accidental dislodgement during seismic vibrations or forklift contact.
- Motorized Mobile Carriages: Constructed from heavy-duty structural H-beams and thick steel plate channels, machined with precise mounting housings for forged steel wheels.
| System Parameter | Motorized Mobile Pallet Racks | Stackable Portable Converters | Gravity Roller Flow Mobile Racks |
|---|---|---|---|
| Target Application | Cold Storage, High-Bay DC, Heavy Industrial | Tire Storage, Seasonal Warehousing, Bulk Freight | FIFO Logistics, E-commerce Fulfillment |
| Load Capacity / Unit | Up to 36,000 kg per mobile carriage block | 1,000 kg – 2,500 kg per stackable tier | 500 kg – 1,500 kg per roller lane position |
| Movement Mechanism | Motorized Geared Electric Drive on Rails | Manual / Forklift Stackable (No Rails) | Gravity Roller Beds on Mobile Track Base |
| Safety Equipment | Infrared Light Curtains, Bumpers, Emergency Stops | Interlocking Stacking Corner Posts | Speed Controllers, End Stops & Dampers |
| Control Automation | PLC Radio Frequency, WMS Integration Ready | Manual Handling | Semi-Automated Stop Mechanisms |
| Surface Finish | Electrostatically Applied Epoxy Powder Coat (60-80μ) | Hot-Dip Galvanized / Outdoor Powder Coated | Zinc Plated Rollers + Coated Steel Frame |
3. Product Future Procurement Trends in Global Warehousing (2025–2030)
As international supply chains evolve toward smart manufacturing and nearshore logistics hubs, procurement teams must look beyond initial equipment acquisition costs. Understanding key future trends ensures that installed racking systems remain adaptable for decades.
1. Rapid Adoption in Cold Chain Logistics
With global demand for frozen food and biologics expanding, cold room operational costs are sky-rocketing due to refrigeration power requirements. Building or expanding refrigerated space costs up to 3x more than conventional ambient storage. Mobile racking doubles cubic freezer capacity, directly slashing per-pallet energy consumption by up to 40%.
2. WMS & AGV/AMR Integration
Modern mobile pallet racking is no longer a static steel asset. Future-ready systems seamlessly interface with Warehouse Management Systems (WMS) and Autonomous Mobile Robots (AMRs). When a forklift or AGV approaches, the WMS automatically commands the racking block via Wi-Fi/Zigbee protocols to open the exact required aisle prior to vehicle arrival.
3. ESG & Sustainable Green Steel Sourcing
Enterprise procurement departments in North America, Europe, and Australia now demand transparent carbon auditing. Leading Chinese suppliers are switching to eco-friendly powder coating lines featuring zero-VOC emissions, closed-loop water treatment systems, and recycled low-carbon steel billets compliant with ISO 14001 environmental standards.
4. Modular "Plug-and-Play" Portable Stackable Racks
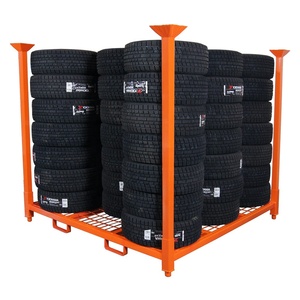
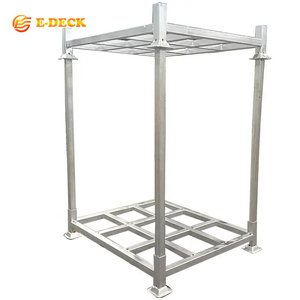
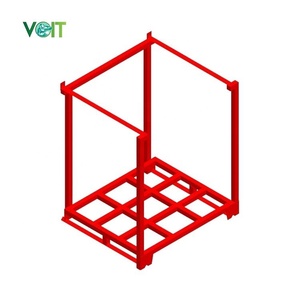
For third-party logistics (3PL) providers handling fluctuating seasonal inventory, fixed bolted racking can restrict flexibility. Portable stackable pallet converters and tire racks allow warehouses to scale up vertical storage during peak surges and collapse/nest frames away when empty, preserving valuable floor space.
4. Technology Evolution & Smart Safety Architectures
Historically, safety concerns regarding moving heavy industrial machinery were a barrier to mobile racking deployment. Today, state-of-the-art electronic safety sensor arrays have transformed modern mobile racks into one of the safest high-density storage mediums available in material handling.
4.1 Multi-Layered Safety Systems
Zenithrack integrates a triple-guard safety matrix across every motorized mobile racking installation:
- Photoelectric Safety Curtains: Mounted horizontally along the floor level and vertically at aisle entrances. If a forklift foot, fallen box, or operator breaks the infrared beam while the mobile bases are motioning, the system triggers a microsecond soft-brake halt.
- Physical Impact Safety Bumpers: Flexible rubber-padded limit switches running the full length of each mobile carriage automatically disengage power upon physical contact.
- Overload & Deflection Monitoring: Smart sensors detect uneven load distribution or mechanical resistance caused by floor debris, preventing strain on electric drive motors.
Engineering Deep-Dive: Seismic-Resistant Mobile Base Anchoring
In earthquake-prone zones (such as South America, Japan, and parts of Southern Europe), mobile racking systems require specialized anti-topple structural engineering. Zenithrack designs mobile carriages with extended wheelbases, mechanical top-guide stabilization rails, and floor-anchored anti-tip hooks. This prevents base tilting under seismic lateral acceleration forces up to seismic zone 4 requirements.
5. Enterprise Advantages & Factory-Direct Export Credentials
Selecting a racking supplier requires validating manufacturing depth, quality control rigorousness, and turnkey export capabilities. Zenithrack Industrial Equipment Co., Ltd. brings over 15 years of continuous manufacturing experience, serving Fortune 500 companies, Tier-1 logistics providers, and regional distributors worldwide.
5.1 Real Factory Capabilities (Dongguan, China)
Operating an extensive 8,000 m² modern manufacturing facility staffed by 75+ skilled engineers, welders, and technical personnel, our factory houses 35 sets of specialized industrial equipment, including:
- High-speed automated continuous roll-forming lines capable of pressing 120-meter upright profiles per minute with precise CNC punching hole pitches.
- OTC & ABB robotic welding cells delivering 100% full-penetration seam welding on beam connectors and mobile chassis frame joints.
- A 220-meter fully automated electrostatic powder coating tunnel with multi-stage chemical pretreatment and zinc phosphate washing.
- In-house metallurgic testing laboratory equipped with coating thickness gauges, universal tensile strength testing machines, and salt-spray corrosion chambers.
5.2 Proven Global Project Expertise
Having exported heavy-duty industrial racking to over 50 countries across North America, Europe, the Middle East, Southeast Asia, and Australia, Zenithrack handles complete cross-border supply chain logistics. From engineering CAD drawings, static load calculations, container loading optimization (avoiding freight damage), to installation guidance, we deliver complete turnkey confidence.
Need a Turnkey Warehouse Layout & Cost Estimation?
Our senior structural racking engineers prepare customized 2D/3D CAD layouts, capacity calculations, and factory-direct price quotes within 24 hours.
Inquire Now6. Comprehensive FAQ: Buyer's Engineering & Procurement Guide
How do I choose between selective, drive-in, radio shuttle, and mobile pallet racking?
Selective Pallet Rack: Ideal when you have high SKU diversity and require 100% direct access to every pallet, but floor footprint is not constrained.
Drive-In Rack: Best for a low number of SKUs stored in massive volumes where Last-In, First-Out (LIFO) inventory rotation is acceptable. Has lower space efficiency than mobile racking due to fixed forklift entry aisles.
Radio Shuttle Rack: Excellent for deep-lane storage with high throughput automation, supporting both FIFO and LIFO rotation via remote carriers.
Motorized Mobile Pallet Rack: The ultimate choice when floor space (or cold room volume) is extremely expensive, high SKU selectivity (100% direct access) is required, and maximum cubic density (up to 85% utilization) must be achieved.
What specific warehouse dimensions & data are needed for a free layout design?
To provide an accurate engineering layout and structural quotation, please prepare:
- Warehouse building layout drawing (CAD or dimensioned PDF) detailing column grids, building doors, and office partitions.
- Clear height under the roof truss or lower obstacle (sprinklers, lighting, HVAC ducts).
- Pallet specification: Length x Width x Load Height (including goods) and total Gross Weight per pallet position.
- Forklift model, minimum turning radius, and maximum mast lift height.
- Operational environment: Ambient warehouse temperature vs. Cold storage / Deep freeze room temperature.
What surface treatment is best for heavy-duty mobile racks: Powder Coating or Hot-Dip Galvanizing?
Thermosetting Powder Coating (60–80 microns): Ideal for dry ambient indoor warehouses and climate-controlled facilities. Offers superior color customization (RAL color codes for brand matching), scratch resistance, and cost efficiency.
Hot-Dip Galvanizing (HDG): Required for outdoor exposure, high-humidity environments, harsh chemical storage, or deep freezer cold rooms (-30°C) where condensation can cause raw steel oxidation over time. HDG coats all internal and external surfaces with a thick zinc alloy layer (>= 65-85 microns).
Can Zenithrack mobile racks be integrated into existing concrete floors?
Yes. Depending on your building condition, we offer two floor rail installation methods:
1. Embedded Floor Rails: Floor grooves are cut into the existing concrete slab, rails are leveled with high-strength non-shrink epoxy grout, and the floor is resealed flush. This permits seamless forklift operation without speed bumps.
2. Surface-Mounted Flat Rails: Ideal for leased facilities where floor cutting is restricted. Rails are anchored directly to the slab with low-profile ramp plates installed along aisle edges.
How does Zenithrack ensure strict quality control prior to export shipment?
Our certified QC department conducts rigorous 5-stage inspections:
- Raw Material Audit: Mill test certificate verification and steel coil thickness tolerance checks.
- Dimensional Precision: CNC hole punching pitch accuracy and roll-forming profile cross-section verification.
- Weld Seam Integrity: Ultrasonic and visual weld seam testing on load-bearing beam connectors and base frame assemblies.
- Coating Durability: Cross-hatch adhesion testing, impact resistance testing, and coat thickness measurement.
- Trial Assembly & Load Testing: Sample bays are fully erected on factory floor jigs prior to protective bundle wrapping and steel-strapped export packaging.
Do you supply OEM services for foreign racking distributors and system integrators?
Absolute confidentiality and OEM customization are core parts of our export business. We provide custom profile designs, OEM brand labeling, custom carton packaging, specialized powder-coat color schemes, and unbranded CAD assembly documentation so local rack dealers and warehouse integrators can market under their own company brand.