Featured Storage Systems & Racking Solutions
Engineered for high density, seismic safety, maximum cube utilization, and seamless automation integration.
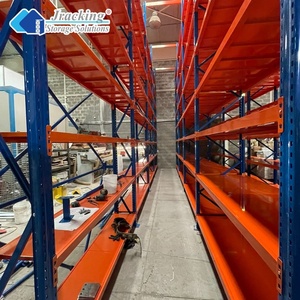
Custom engineered Q235B structural pallet racking for high-capacity fulfillment centers.
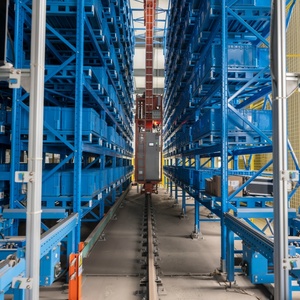
Automated storage and retrieval systems with integrated robotic picking efficiency.
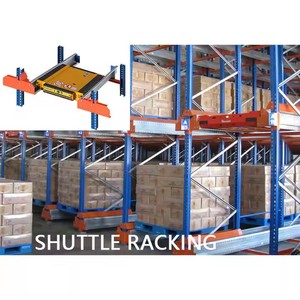
Semi-automated high-density pallet runner for cold storage and deep-lane logistics.
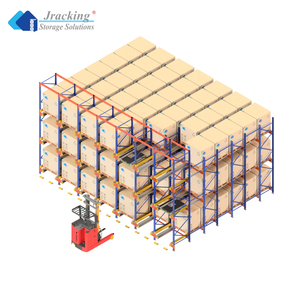
Factory-direct intelligent automated carrier racking engineered for 24/7 operations.
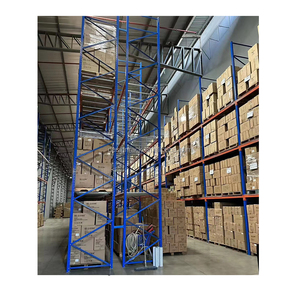
Heavy-duty modular pallet racks built to FEM and RMI rigorous structural compliance.
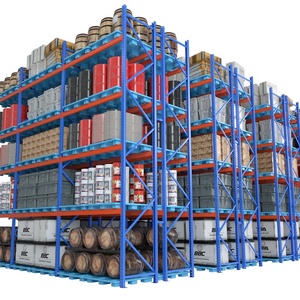
Multi-tier rack-supported structure maximizing vertical floor space utilization.
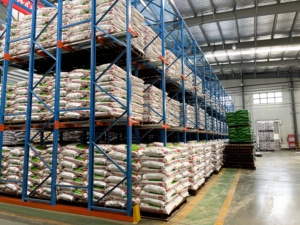
Low-temperature resistant automated pallet runner system designed for freezer rooms.
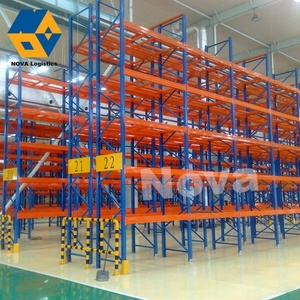
Factory-direct customizable warehouse racking optimized for heavy industrial loads.
Technical White Paper: Modern Mobile Storage Racking & High-Density Storage Engineering
In modern industrial logistics, floor area acquisition and facility thermal control represent two of the largest operational expenditures. Standard static pallet racking systems typically utilize less than 40% of available floor space for actual storage, leaving up to 60% consumed by permanent forklift aisles. Mobile storage racking systems (both Electric Mobile Pallet Racking and Trackless Heavy-Duty Mobile Racking) eliminate static aisles by mounting racking blocks onto motor-driven mobile bases running on embedded floor tracks. This structural approach doubles usable warehouse storage density within the exact same footprint.
1. Structural Mechanics and Metallurgical Standards
Mobile storage racking structures operate under dynamic kinetic stresses and heavy concentrated loads. Standard configurations support unit loads up to 24,000 kg per movable bay. Achieving long-term structural integrity requires strict compliance with international steel fabrication standards:
- Raw Material Composition: Uprights and load-bearing beams are roll-formed from high-tensile cold-rolled steel (SS400, Q235B, or Q355B grades). Yield strength is engineered to withstand severe torsional moments during carriage start-stop cycles.
- Structural Profile Optimization: Uprights feature multi-bend Omega (Ω) cross-section profiles with cold-punched teardrop or diamond beam attachment slots, yielding an optimal strength-to-weight ratio and elevated moment of inertia.
- Floor Rail Precision Tolerances: Heavy-duty mobile bases travel over precision-ground steel rails embedded directly into the concrete slab. Rail alignment tolerances must maintain a strict horizontal level within ±1.0 mm per 10 linear meters to prevent wheel flange wear and mechanical binding.
System Performance Matrix: Static Racking vs. Mobile Racking vs. Radio Shuttle
| Storage Metric | Selective Pallet Rack | Electric Mobile Racking | Radio Shuttle Racking | Automated ASRS (Miniload) |
|---|---|---|---|---|
| Floor Area Utilization | 35% – 45% | 80% – 90% | 70% – 80% | 85% – 95% |
| Direct Pallet Accessibility | 100% (Immediate) | 100% (On-Demand Aisle) | Deep-Lane (FILO/FIFO) | 100% Automated |
| Cold Storage Operating Cost | Baseline (High Energy Cost) | 45% Energy Reduction | 35% Energy Reduction | 50% Energy Reduction |
| Initial Capital Expenditure | Low | Moderate to High | Moderate | High |
| Forklift Aisle Demand | Multiple Fixed Aisles | Single Moving Aisle | Single Loading Face | Zero Internal Aisles |
2. Electronic Control Architecture & Multi-Tier Safety Sensors
Safety engineering is paramount in motorized mobile storage rack installations. Advanced Chinese manufacturers like Zenithrack integrate industrial PLC control units (Siemens S7-1200 series) with multi-layered optical protection curtains:
- Photoelectric Safety Foot Barriers: Continuous infrared beams run parallel to the ground along the entire length of each mobile carriage base. If an object or operator breaks the light beam while a carriage is in motion, emergency fail-safe brakes lock the drive motors within milliseconds.
- Optical Distance & Anti-Collision Lasers: Radar distance sensors dynamically calculate inter-carriage spacing, regulating smooth acceleration and soft-deceleration curves to eliminate cargo shifting.
- WMS & RFID Integration: Modern electric mobile storage racking communicates seamlessly with Enterprise Resource Planning (ERP) and Warehouse Management Systems (WMS) via industrial Wi-Fi or optical data transceivers, enabling automatic aisle opening prior to forklift arrival.
Global Procurement Trends: Sourcing Industrial Mobile Racking from China (2025–2030)
The global logistics and industrial storage equipment landscape is shifting rapidly toward automated, high-density, and energy-efficient solutions. Global supply chain procurement managers face persistent inflation in construction costs, driving a preference for high-cube storage density over facility expansion. Sourcing mobile storage racking directly from top-tier Chinese manufacturers has emerged as a primary strategic advantage for international distributors, system integrators, and plant engineers.
1. ESG & Cold Chain Thermal Efficiency
Refrigerated warehouse facilities consume immense electrical power. By consolidating pallets into compact mobile blocks, chilled air volume is reduced by up to 50%, generating immediate, measurable reductions in carbon footprint and utility expenses.