Featured Single Row & Heavy-Duty Pallet Racking Systems
Engineered for maximum structural stability, direct SKU accessibility, and rigorous load-bearing safety. Explore our factory-direct warehouse storage solutions manufactured in Dongguan, China.
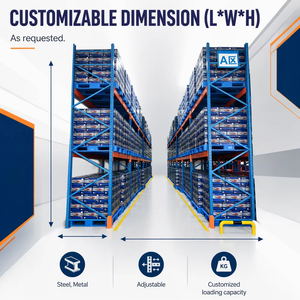
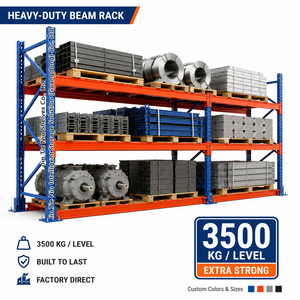
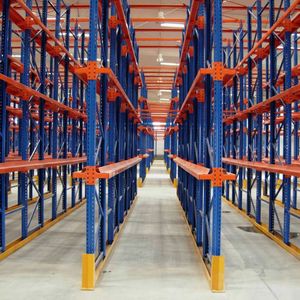
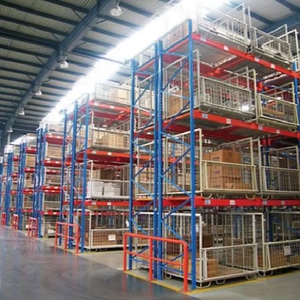
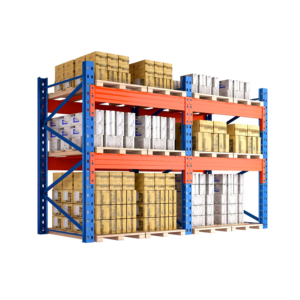
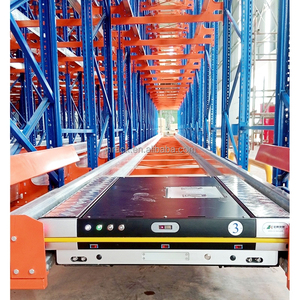
1. Executive Overview: Single Row Pallet Racking in Modern Logistics
In modern industrial logistics and material handling, Single Row Pallet Racking (frequently designated as Single-Deep Selective Racking) serves as the structural foundation for facilities requiring 100% direct item accessibility, rapid stock rotation, and flexible SKU management. Positioned along building perimeter walls or interspersed within double-row configurations, single row pallet racking eliminates the need for specialized double-reach forklifts while guaranteeing unimpeded access to every individual unit load.
While double-entry (back-to-back) rack runs maximize floor density, single row runs are critical structural components of high-efficiency distribution centers. They accommodate irregular facility footprints, support specialized pick-and-pass aisles, and integrate seamlessly with wall-mounted building columns and utility drops. As global supply chains transition toward high-velocity e-commerce order fulfillment, selecting an experienced Chinese OEM manufacturer ensures your storage infrastructure balances nominal load capacities with strict dynamic safety thresholds.
Single Row vs. Double Row Mechanical Dynamics
Single row racks exhibit unique structural behavior compared to back-to-back configurations. Lacking horizontal cross-row ties (row spacers) to a parallel rack frame, single row racks rely entirely on their upright column geometry, horizontal/diagonal bracing patterns, baseplate anchoring, and beam-to-column connector rigidity to withstand sway loads, seismic forces, and accidental forklift impacts. Sourcing single row racking requires strict adherence to vertical stability ratios and structural engineering calculations.
2. Engineering Standards & Structural Specifications
Leading Chinese racking exporters utilize cold-rolled high-tensile structural steel grades (such as Q235B and Q355B/S355JR) manufactured under tight dimensional tolerances. Below is an authoritative technical specification matrix for heavy-duty single row pallet racking systems engineered to meet international standards such as ANSI MH16.1 (RMI), EN 15512, and AS4084-2012.
| Structural Parameter | Standard Specification | High-Load Heavy Duty Option | Compliance Standard |
|---|---|---|---|
| Steel Grade | Q235B Cold-Rolled Carbon Steel | Q355B / S355JR High-Strength Alloy Steel | GB/T 700 / EN 10025 |
| Upright Profile Options (mm) | 80×60×1.8/2.0, 90×70×1.8/2.0 | 100×70×2.0/2.3/2.5, 120×95×2.5/3.0 | ISO 9001 Quality System |
| Beam Profiles (Box Beam) | 80×50, 100×50, 110×50 (1.5mm thick) | 120×50, 140×50, 160×50 (1.8–2.0mm thick) | ANSI MH16.1 / FEM 10.2.02 |
| Max Bay Load Capacity | Up to 10,000 kg (10 Tons) per frame | Up to 24,000 kg (24 Tons) per frame | EN 15512 Safety Factor 1.95 |
| Beam Deflection Limit | L/200 of clear span width | L/300 for automated high-bay integration | RMI / AS4084 Standard |
| Surface Finish | Thermosetting Epoxy-Polyester Powder (60-80μ) | Hot-Dip Galvanized (HDG >65μ coating) | ASTM B117 Salt Spray >500 hrs |
| Pitch Adjustment | 50mm, 75mm, or 76.2mm (3-inch) pitch | Custom hole-pitch engineering | Universal Teardrop / Omega profile |
3. Structural Anatomy of Single Row Selective Racking
To ensure high operational throughput without compromising workplace safety, Zenithrack engineers each component for structural redundancy. The key elements of high-performance single row racking include:
Precision Roll-Formed Uprights
Manufactured using continuous automated roll-forming machines with up to 22 forming passes. Unique Omega profiles feature stiffening ribs that resist torsional twisting under high vertical loads.
Interlocking Safety Connectors
Heavy-gauge steel beam end-connectors utilize 3 to 5 rivet hooks that wedge tightly into upright slots. Automatic spring-loaded safety locks prevent accidental beam dislodgement from forklift contact.
Heavy-Duty Anchor Baseplates
Seismically rated baseplates distribute column leg loads across the concrete slab. Dual expansion anchor bolts ensure moment-resistant foot connections critical for single row rack stability.
4. Future Procurement & Industry Trends (2025–2030)
The global warehousing and material handling industry is undergoing rapid technical evolution. Buyers seeking competitive advantage when importing racking from China should align their procurement strategies with four emerging industry trends:
A. AMR & AGV Integration with Single Row Layouts
Traditional forklift-operated narrow aisle racking is increasingly interfacing with Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Future single row racking designs require enhanced bottom-clearance openings, sensor reflective markers, and tighter fabrication tolerances (±1.0mm) to allow smooth robotic pallet retrieval.
B. Smart Structural Monitoring & IoT Strain Sensors
Industrial racking systems are adopting IoT-enabled strain gauges and deflection sensors installed directly inside upright profiles. These sensors provide real-time alerts when overload thresholds are exceeded or when subtle forklift collisions compromise structural integrity, shifting maintenance from reactive to predictive.
C. Ultra-High Tensile Eco-Steel Formulations
Escalating raw material costs and corporate sustainability goals are accelerating the shift toward low-carbon high-tensile steel alloys. By using thinner-gauge Q355B and S355 grade steels, manufacturers reduce total structural weight by 12–18% while maintaining identical payload ratings, yielding substantial ocean freight savings.
D. Advanced Automated Powder Coating Finish
Modern Chinese racking facilities have replaced manual spray lines with fully automated Swiss Gema electrostatic powder coating tunnels. Micro-processor controlled pretreatment washes and nanotech zirconium conversion coatings deliver superior corrosion resistance, ensuring long-term durability in ambient and cold-storage environments.
5. Single Row Pallet Racking Procurement FAQ
Essential technical answers compiled by Zenithrack senior structural engineers to simplify overseas procurement and custom OEM engineering.
6. Why Partner with Zenithrack Industrial Equipment
Selecting a racking supplier requires evaluating manufacturing hardware, engineering expertise, and quality control discipline. Based in Dongguan, Guangdong — the world's leading industrial manufacturing hub — Zenithrack Industrial Equipment Co., Ltd. stands as an established factory direct leader in warehouse storage systems.
Factory Direct Scale
Operating an 8,000 m² modern manufacturing plant equipped with 35 sets of specialized production machinery, including automatic cold roll-forming mills, laser steel cutters, and robotic welding cells.
Proven Market Record
Over 15 years of industry specialization with annual sales surpassing CNY 100 Million. Proven track record supplying high-bay racking systems to Fortune 500 brands and global logistics leaders like SF Express, BYD, FedEx, and Cooper.
Full Service Engineering
Supported by a dedicated 75+ professional workforce, including senior structural engineers who provide free CAD layouts, finite element analysis (FEA) reports, and customized load capacity certifications within 24 hours.
Ready to Optimize Your Warehouse Storage Layout?
Whether you are planning a new logistics hub, upgrading a selective single row rack installation, or sourcing high-volume OEM racking components from China, Zenithrack offers factory-direct engineering expertise, competitive pricing, and fast international shipping.