Featured Storage Systems for Melbourne Facilities
Direct factory engineering and supply of heavy-duty pallet racking, radio shuttle systems, and custom industrial storage frames tailored to Australian logistics demands.
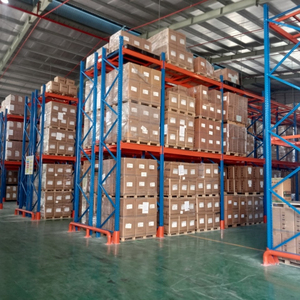
Wholesale Heavy Duty Selective Pallet Racking System Designed for Easy Pallet Access and Reliable Cold Storage Applications
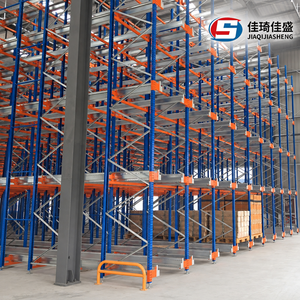
Multi-Level Automatic Warehouse Racking River-Type Pallet Two-way Radio Shuttle Rack for Storage Iron Steel Material
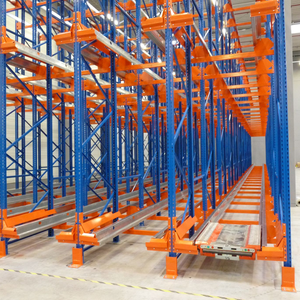
Customized Radio Shuttle Pallet Racking Automated Semi-Automatic Storage Racking for Logistics Centers
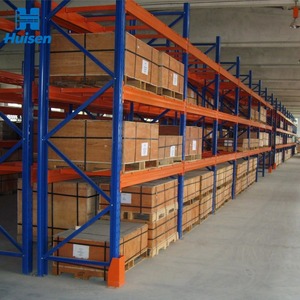
Industrial Heavy Duty Steel Pallet Racking System Adjustable Multi-Level Warehouse Storage Rack
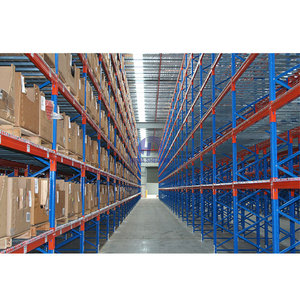
High Performance Heavy Duty Logistics Shelves Stocking Warehouse Storage Rack Pallet Rack for Heavy-Duty Reticulated Shelf
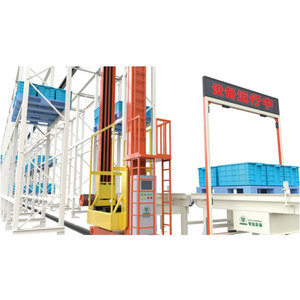
Automated Storage and Retrieval System with Stacker Crane and Steel Racking System
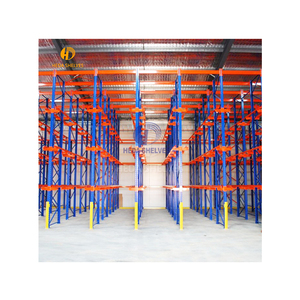
High-Capacity Drive-In Pallet Racking Storage System Drive-Thru Rack for LIFO Pallet Organization Drive in Racking Steel Units
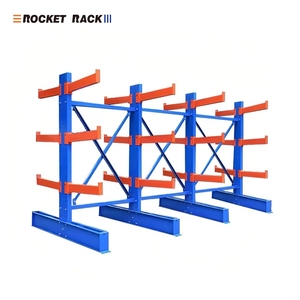
Stackable Heavy Duty Shelf Warehouse Shelves Heavy Duty Cantilever Steel Coil Rack
Solving Melbourne’s Industrial Warehousing & Land Cost Pressures
Greater Melbourne, Victoria, stands as Australia's primary logistics and supply chain engine. Key industrial precincts—including Truganina, Laverton North, and Altona in the West, Campbellfield and Somerton in the North, and Dandenong South in the South-East—are witnessing unprecedented industrial land valuation surges alongside escalating warehouse rental rates per square metre. Supply chain operators, third-party logistics (3PL) providers, food and beverage distributors, and cold storage facilities face a pressing dual challenge: maximizing pallet density within existing building footprints while drastically suppressing operational labour costs.
Traditional storage configurations such as standard selective pallet racking often squander up to 60% of floor space on forklift aisles. While manual Drive-In racking improves volumetric storage density, it imposes crippling drawbacks: high forklift collision damage risks, slow retrieval cycles, and strict Last-In-First-Out (LIFO) operational rigidity. This whitepaper evaluates how factory-engineered Automated Pallet Shuttle Systems (Radio Shuttle Racking) act as the definitive capital expenditure (CapEx) investment to achieve high-density automation without the multi-million-dollar complexity of fully automated stacker-crane AS/RS setups.
Information Gain Insight: Upgrading a 3,000 m² Melbourne warehouse from standard selective pallet racking to a 4-way Radio Pallet Shuttle System increases volumetric pallet position capacity by up to 220%, reduces forklift travel fleet requirements by 45%, and slashes energy cost per pallet footprint in refrigerated facilities by over 35%.
1. The Mechanics of Automated Radio Pallet Shuttle Engineering
An Automated Pallet Shuttle system comprises high-precision cold-formed steel racking structures fitted with continuous internal runner rails, combined with self-propelled, battery-powered shuttle carts controlled via RF remote controllers or integrated Warehouse Management System (WMS) networks. The operational workflow completely decouples forklift travel from storage channels:
- Pallet Placement: A standard counterbalanced or reach forklift deposits the shuttle cart at the entry of the designated rack channel, followed by the pallet.
- Automated Transport: The shuttle's internal optical and ultrasonic sensors detect the pallet, lift it via a heavy-duty hydraulic platform, and transport it smoothly along the channel to the deepest available storage position.
- FIFO / LIFO Adaptability: Channels can be configured for First-In-First-Out (FIFO) in double-entry layouts (ideal for perishable food and beverage distribution in Victoria) or Last-In-First-Out (LIFO) in single-entry layouts (ideal for bulk manufacturing raw materials).
High-Efficiency Battery Tech
Powered by Lithium Iron Phosphate (LiFePO4) battery cells, offering 8–10 hours of continuous operation with rapid 2-hour charging cycles and zero memory degradation.
Cold Storage Optimized
Engineered for deep-freeze environments down to -25°C. Features IP65 electrical sealing, anti-condensation internal heating, and low-temperature lubricants.
WMS & PLC Integration
Seamlessly interface with industrial Modbus/TCP, Siemens PLC, or custom warehouse software to enable real-time inventory tracking and automated batch picking.
Industrial Storage Technology Comparison Matrix
A comparative structural and financial analysis for Australian warehouse managers evaluating racking upgrades.
| Racking System Type | Floor Space Utilization | Pallet Access Speed | Forklift Damage Risk | Australian Pallet (1165x1165mm) Fit | Relative CapEx / Pallet Slot |
|---|---|---|---|---|---|
| Selective Pallet Racking | 35% – 45% | 100% Direct (Very High) | Low | Standard Dual Beam Spans | Baseline ($) |
| Drive-In Racking | 65% – 75% | Slow (LIFO only) | High (Forklift drives inside) | Guide Rails Required | Moderate ($$) |
| 2-Way Radio Shuttle Racking | 80% – 85% | Fast (Automated Lane Travel) | Very Low (External loading) | Precision CNC Rail Profile | Optimal ROI ($$$) |
| 4-Way Automated Shuttle System | 85% – 92% | Ultra-Fast (Cross-lane movement) | Zero (Fully automated integration) | Multi-directional Runner Rails | Advanced ($$$$) |
| Heavy Duty Cantilever Racking | 50% – 60% (Long goods) | Direct / Open Face | Low | N/A (Built for Pipe/Timber/Coils) | Specialized ($$) |
Why Direct Importers & Integrators Partner with Zenithrack
Zenithrack Industrial Equipment Co., Ltd. is not a trading middleman or third-party agent; we are a dedicated, direct racking manufacturing enterprise situated in Dongguan, Guangdong, China. With over 15 years of continuous engineering innovation, an 8,000 m² heavy-manufacturing facility, and a workforce of 75+ skilled engineers, fabricators, and quality control specialists, we deliver world-class storage systems built to rigorous international structural codes.
Having earned a dominant position among domestic industrial suppliers with annual domestic sales exceeding CNY 100 million, Zenithrack expanded its direct export division to supply warehouse projects across Australia, New Zealand, North America, and Europe. Our production lines feature 35 sets of high-precision roll-forming machines, automated robotic welding cells, continuous punching systems, and automated electrostatic powder coating lines.
AS 4084-2012 Rigor
Structural steel profiles engineered to meet Australian racking and seismic standards.
24-Hour Design Turnaround
Free warehouse floor plan analysis and CAD layouts generated within 24 hours.
Full Quality Control Guarantee
Our dedicated QC department inspects raw steel coils (Q235B & Q355B), structural weld integrity, slot punching precision, and paint film thickness (60–80 microns) prior to export container loading.
Tailored Racking Solutions for Melbourne Industry Sectors
1. Cold Storage & Food Logistics
Refrigerated warehouses in Altona and West Melbourne handle intense throughput of dairy, meat, and frozen produce. Zenithrack shuttle systems feature low-temperature sensors, anti-freeze stainless steel runner guides, and sealed lithium power packs engineered for uninterrupted operation at -25°C.
2. Fast-FMCG & E-Commerce Hubs
Large fulfillment centers in Truganina require high SKU throughput. By integrating Radio Shuttle channels with lower-tier Selective picking levels or Boltless Shelving, operators achieve maximum overhead high-bay storage while maintaining fast manual picking access at floor level.
3. Manufacturing & Steel Distribution
Industrial facilities in Campbellfield and Dandenong South storing heavy raw steel, long aluminum profiles, or die-molds utilize our heavy-duty Cantilever racks and specialized Mold Racks with pull-out drawers, rated for up to 3,000 kg load capacity per level.
Frequently Asked Questions for Melbourne Buyers
Essential technical and compliance answers for Australian logistics directors and warehouse owners.
How do Zenithrack shuttle systems comply with Australian Standard AS 4084-2012?
Can your radio shuttle carts handle standard Australian Hardwood Pallets (1165mm x 1165mm)?
What is the typical shipping lead time and logistics route to the Port of Melbourne?
How do I choose between Selective, Drive-In, and Radio Shuttle racking for my facility?
What information is required to receive a free custom layout drawing and pricing?
What Our Industrial Partners Say
"Our team is very satisfied with the racks — the result after installation looks great. My colleague personally visited Zenithrack’s factory in Dongguan and was impressed by their automated equipment and structural testing."
"Throughout the whole purchasing process, Zenithrack was very professional. Bradley, their technical sales manager, was extremely responsive to our custom load calculation requests. Very satisfied with the surface finish."
"I have worked with Zenithrack for 5 years importing racking products, and I'm glad I chose them from the beginning. Their structural steel powder coating quality is impeccable. My installation clients have never complained."