Engineered Racking Systems for Australian Pharma Warehouses
Factory-direct OEM/ODM storage profiles structural steel pallet racking systems certified for cleanrooms, cold chain, and high-density distribution centers across Sydney, Melbourne, Brisbane, and Perth.
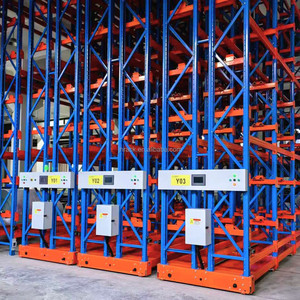
Industrial Heavy Duty High Efficiency Warehouse Electric Mobile Storage Shelf Automatic Mobile Racking System Pallet Rack
Inquire Now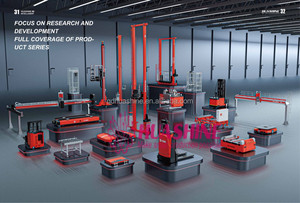
HEAVY DUTY HUASHINE ASRS Automatic Storage Racking System with Stacker Crane/AGV/4 WAY CAR for Raw Material/Finished Goods
Inquire Now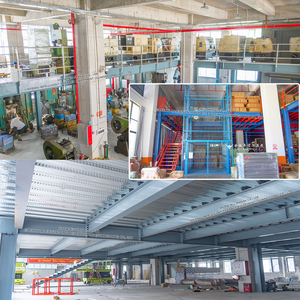
Heavy Duty I-Beam Steel Structural Platform Mezzanine Floor Rack for Industrial Warehouse Storage Factory
Inquire Now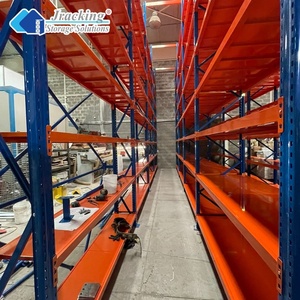
Jracking EURO Standard Warehouse Storage Racks Heavy Duty Steel Pallet Racking System For Distribution
Inquire Now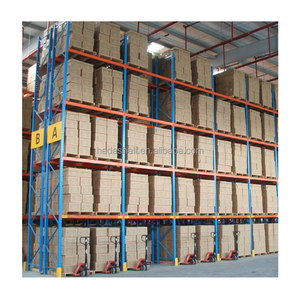
Heavy Duty Metal Pallet Storage Racking 1000kg/2000kg/3000kg Per Layer Industrial Pallet Shelving Rack
Inquire Now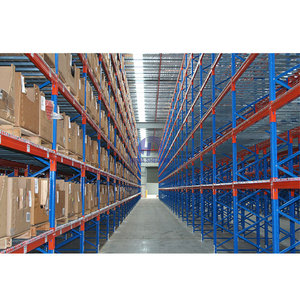
High Performance Heavy Duty Logistics Shelves Stocking Warehouse Storage Rack Pallet Rack for Heavy-Duty Reticulated Shelf
Inquire Now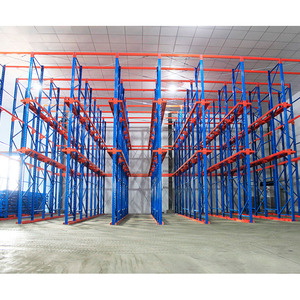
Drive-Through Pallet Rack Forklift Pickup Heavy Duty High Density Warehouse Storage Rack
Inquire Now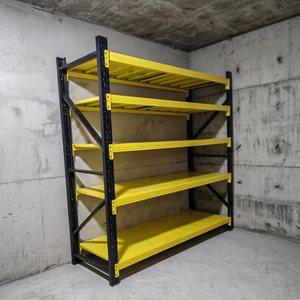
Steel Mezzanine Rack Warehouse Mezzanine Shelving System Pallet Rack Storage Platform Industrial Multi-Level Racking
Inquire NowWhitepaper: Technical Engineering & OEM/ODM Standards for Australian Pharmaceutical Racking Systems
The Australian pharmaceutical logistics supply chain operates under strict regulatory oversight from the Therapeutic Goods Administration (TGA) and requires unwavering adherence to AS 4084:2023 / AS 4084-2012 (Steel Storage Racking) standards. As a premier OEM/ODM manufacturer specializing in precision structural steel racking solutions, Zenithrack provides custom-engineered pallet storage infrastructures designed specifically to overcome the environmental, operational, and regulatory challenges of pharmaceutical supply chains across Australia.
Key Information Gain: AS 4084:2023 Structural Compliance & TGA Validation
Unlike standard commercial racking, pharmaceutical pallet racking deployed in Australian facilities requires specific design checks: dynamic deflection tolerances lower than L/200 under maximum rated load, certified structural steel grades (Q235B/Q355B equivalent to AS/NZS 3678 Grade 250/350), specialized anti-microbial epoxy powder coatings resistant to aggressive chemical sanitizers, and seismic load calculation according to AS 1170.4 for earthquake resilience in regional zones.
1. Engineering Material Integrity & Cleanroom Compatibility
Pharmaceutical products—ranging from Active Pharmaceutical Ingredients (APIs) and bulk raw materials to finished solid dosage forms and temperature-sensitive biologics—demand an uncompromised cleanroom and warehouse environment. Standard steel racking prone to flaking paint, particulate shedding, or rust oxidation poses severe audit risks during TGA Good Distribution Practice (GDP) inspections.
Our OEM/ODM manufacturing protocols integrate advanced surface preparation and material formulations:
- Structural Steel Selection: High-tensile cold-rolled steel profiles engineered for structural stability, ensuring high strength-to-weight ratios and minimal frame deflection.
- Antimicrobial Powder Coating: Thermosetting epoxy-polyester coatings infused with silver-ion antimicrobial additives that actively inhibit bacterial growth, micro-fungi, and mold spores on rack surfaces.
- Sub-Zero Cold Chain Galvanizing: For blast freezers and cold storage units operating between -25°C and -80°C, we utilize hot-dip galvanizing according to ISO 1461 / AS/NZS 4680, preventing hydrogen embrittlement and surface micro-cracking caused by extreme thermal cycling.
- Zero-Dust Shelf Decks: Smooth perforated steel panels or wire mesh decking with rounded safety edges prevent dust accumulation and facilitate unobstructed airflow for temperature uniformity throughout high-bay racking tiers.
Localized Application Scenarios in Australia
Tailored racking design solutions optimized for regional climatic conditions, localized warehouse floor plans, and industry-specific supply chain requirements in Australia.
Cold Chain Vaccine & Biologics Hubs (2°C to 8°C & -20°C Freezers)
Major pharmaceutical cold chain distribution centers situated in Melbourne (Truganina, Altona) and Sydney (Western Sydney Aerotropolis, Eastern Creek) require maximum cube utilization within expensive refrigerated footprints. Our Electric Mobile Racking Systems and Radio Shuttle Racking eliminate static service aisles, increasing cold room storage density by up to 85% while reducing energy consumption per pallet position.
TGA-Compliant Cleanroom & API Bulk Raw Material Storage
In specialized manufacturing plants in Brisbane and Adelaide producing sterile injectables or oral solid doses, raw materials must be strictly segmented. Our OEM drive-in and selective pallet racking systems feature chemical-resistant, non-gassing powder coats and customized barrier mesh walls to isolate controlled substances and active ingredients safely without cross-contamination risks.
High-Throughput 3PL E-Commerce & Retail Pharmacy Distribution
Fast-moving healthcare logistics hubs handling over-the-counter (OTC) medicine, nutraceuticals, and medical devices depend on rapid order fulfilment. By pairing Multi-Tier H-Steel Structural Mezzanine Platforms with heavy-duty selective racking, logistics operators gain 200% to 300% additional usable floor space for automated sorting, pick-to-light systems, and conveyancing without expanding physical real estate footprints.
High-Security Vault & Scheduled Medicine Storage Racking
Schedule 8 (S8) controlled drugs demand secure enclosure within warehouse spaces. Zenithrack designs custom heavy-duty enclosed pallet racking modules with integrated biometric access mounting points, anti-pry steel cladding, and anti-collapse mesh walls, satisfying strict state-level Australian health authority security guidelines.
Pharmaceutical Storage Technology Decision Matrix
Selecting the optimal storage topology requires balancing density, direct SKU accessibility, automation capability, and compliance overheads. The technical visualizer below outlines performance attributes calculated for Australian logistics standards:
| Racking Topology | SKU Access | Space Utilization | Cold Storage Efficiency | TGA & AS 4084 Fit | Ideal Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% Direct | 40% – 50% | Moderate | Compliant (Universal) | High SKU diversity, fast picking, general distribution. |
| Electric Mobile Racking | 100% Direct (On-Demand) | 80% – 90% | Extreme (High Thermal Savings) | Compliant (Requires Sensor Safety) | Cold rooms, vaccine freezers, high-value bulk pharmaceuticals. |
| Radio Shuttle System | Deep-Lane (FIFO/LIFO) | 75% – 85% | High | Compliant (Semi-Automated) | Batch manufacturing, high volume per SKU, cold chain. |
| Automated ASRS (Stacker Crane) | Automated (Software Controlled) | 90% – 95% | Optimal (Unmanned Lightless) | Highest Audit Traceability | 24/7 automated pharma manufacturing and major national distribution nodes. |
| H-Steel Structural Mezzanine | Manual Floor Access | Multiplies Floor Area (2x–3x) | N/A (Ambient Zones) | Compliant (BCA & AS Standards) | Kitting, secondary packaging, hand-pick pharmaceutical items. |
Emerging Industry Trends Shaping Australian Pharma Logistics
1. Adoption of AS 4084:2023 Structural Revision Standards
The Australian standard for steel storage racking updated structural verification procedures, imposing stricter load testing, member tolerance criteria, and mandatory rack safety inspection schedules. Zenithrack’s structural design team utilizes advanced Finite Element Analysis (FEA) software to simulate vertical deflection, torsional buckling, and seismic shock loads, ensuring that every OEM custom rack shipped to Australia meets or exceeds AS 4084:2023 structural standards.
2. Transition to Semi-Automated & AGV-Guided Racking Systems
With rising labor costs in metropolitan Australian industrial hubs, pharmaceutical supply chains are rapidly transitioning from manual forklift picking to Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs). OEM/ODM racking manufacturers must provide tighter manufacturing tolerances on beam placement, upright vertical alignment, and guide-rail straightness (within ±1.5mm tolerance) to support robotic pallet handling without collision risk.
3. Focus on Sustainability, Zero-VOC & Green Warehousing
Australian healthcare corporates and government buyers prioritize ESG (Environmental, Social, and Governance) targets. Our manufacturing facility employs automated powder coating recovery systems, zero-VOC (Volatile Organic Compound) electrostatic paints, and recyclable high-grade steel, enabling Australian warehouse operators to earn credits under Green Star industrial building ratings.
Why Choose Zenithrack as Your OEM/ODM Partner in Australia?
Zenithrack Industrial Equipment Co., Ltd. brings over 15 years of world-class structural steel fabrication experience, combining precision automated production lines with deep engineering expertise in pharmaceutical storage infrastructure.
Direct Factory OEM/ODM Customization
We eliminate intermediary markup while granting complete customization freedom. Whether your warehouse requires unique bay widths to accommodate specialized CHEP/Loscam pallets (1165mm x 1165mm standard in Australia), non-standard column colors, or custom load-rated box beams up to 4000kg per level, our engineering team manufactures to your exact specification.
Rigorous End-to-End Quality Assurance (QA/QC)
Every batch of raw steel undergoes tensile testing and ultrasonic flaw detection before cold roll-forming. Production steps—punching, automated robotic welding, shot-blasting surface treatment, and electrostatic powder coating—are strictly audited by an independent QC department with detailed inspection certificates provided prior to container loading.
Frequently Asked Questions (Australian Procurement FAQ)
Technical and logistics answers for Australian facility managers, project engineers, and supply chain directors importing storage racking systems.
Are your pallet racking systems fully compliant with Australian Standard AS 4084:2023?
How do your rack profiles handle Australian standard CHEP and Loscam pallets?
What are the sea freight lead times and ocean logistics routes to main Australian ports?
- Port Botany (Sydney, NSW): 12 – 16 days transit
- Port of Melbourne (VIC): 14 – 18 days transit
- Port of Brisbane (QLD): 11 – 15 days transit
- Fremantle (Perth, WA): 16 – 22 days transit