Featured Automated Pallet Conveyor & Racking Systems
Custom-engineered pallet conveyor storage systems manufactured for rigorous industrial use, high-throughput fulfillment, and seismic-compliant Northern California facilities.
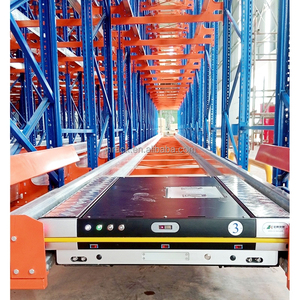
Customized High Density Storage LIFO Pallet Shuttle Racking Galvanized Warehouse Racks Series Pallet Radio- Shuttle Rack System
Get a Quote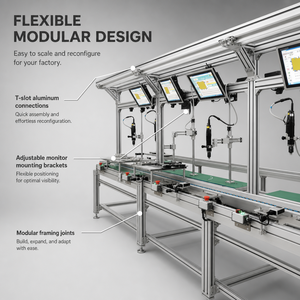
PTS2 Pallet Conveyor System for Battery Module Production Double Speed Chain
Get a Quote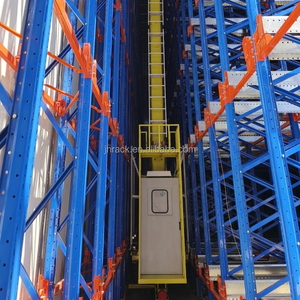
Intelligent ASRS Chain Pallet Conveyor System Industrial Automatic Pallet Racks Shelf Storage Warehouse Racking Systems
Get a Quote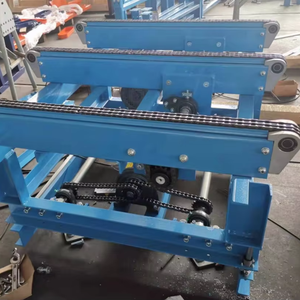
New 1000KG Load Capacity Restaurant Pallet Powered Pop up Chain Transfer Unit Conveyor System
Get a Quote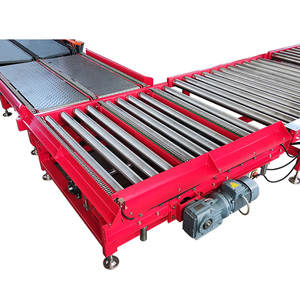
Heavy Duty Pallet Pop-up Roller Transfer Conveyor System for Australian Standard 2-Way Wooden Pallets
Get a Quote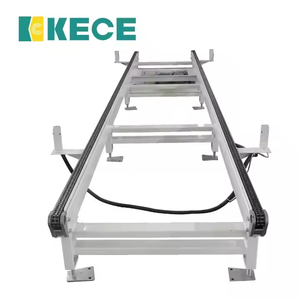
New Pallet Chain Conveyor System for Manufacturing Plant-Durable Materials Handling & Transport with Adjustable Speed
Get a Quote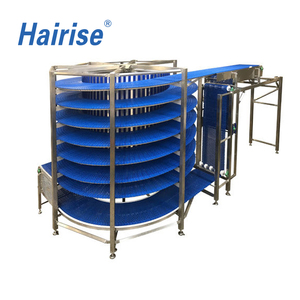
Hairise Automatic Pallet Conveyor Modular Belt Spiral Conveyor System Box Packing for Food Industry
Get a Quote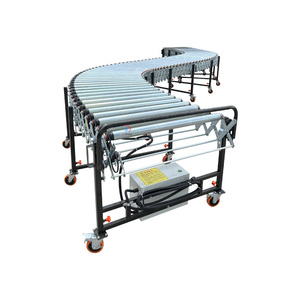
Flexible Powered Roller Conveyor Customized Pallet Handling Conveyor System for Truck Container Loading and Unloading
Get a Quote1. The San Francisco Bay Area Logistics Landscape: Real Estate Pressures & Automation Realities
The San Francisco Bay Area—encompassing San Francisco proper, Silicon Valley (San Jose, Santa Clara, Sunnyvale), the East Bay (Hayward, Fremont, Oakland), and the North Bay—represents one of the most concentrated and expensive industrial real estate markets in North America. With commercial warehouse lease rates routinely hovering between $25.00 and $45.00 per square foot NNN, industrial enterprise operators can no longer afford horizontal footprints dominated by wide aisle forklift transport and static racking.
Compounding the challenges of land scarcity is Northern California’s intense labor market dynamics. Warehouse operational expenses in Alameda, San Mateo, and Santa Clara counties face some of the highest baseline wages nationwide ($22.00 to $34.00/hour for skilled material handling technicians). Consequently, forward-thinking logistics executives, plant engineering managers, and 3PL fulfillment directors are executing aggressive capital transitions toward automated pallet conveyor storage systems, ASRS integrations, and radio shuttle high-density storage to maximize cubic volume utilization and minimize labor overhead.
As a premier factory and direct exporter specializing in heavy-duty material handling, Zenithrack Industrial Equipment Co., Ltd. bridge the gap between world-class structural manufacturing and the hyper-specific architectural demands of Northern California facilities. By engineering heavy-duty pallet handling chain conveyors, pop-up roller transfer units, double-speed battery module production lines, and high-density radio shuttle racks, Zenithrack empowers San Francisco Bay Area enterprises to achieve up to 300% greater storage density and 65% faster pallet throughput compared to legacy selective racking configurations.
Seismic Engineering Imperatives (CBC 2022 & RMI Compliance for Northern California)
Operating a warehouse facility within the San Francisco Bay Area requires navigating stringent seismic safety protocols dictated by the California Building Code (CBC 2022), Title 24 regulations, and the Rack Manufacturers Institute (RMI) standards. The region’s proximity to major fault networks—including the Hayward, San Andreas, and Calaveras faults—classifies almost all local industrial structures under Seismic Design Category (SDC) D, E, or F.
In high seismic hazard zones, standard off-the-shelf storage racking and structural conveyor mounts are prone to severe dynamic load shifts, weld failure, or structural collapse during a seismic event. Zenithrack’s engineering team utilizes high-tensile structural steel profiles (including Q235B and Q355B structural grades), heavy-duty welded footplates, seismic base isolation anchor bolts, and custom horizontal frame bracing designed specifically to absorb dynamic ground accelerations. When exporting systems into the San Francisco market, Zenithrack provides complete structural calculation sets, detailed CAD elevation layouts, and engineering stamp readiness to streamline local municipal building permit approvals across SF, San Jose, Fremont, and Oakland.
| System Architecture | Primary Bay Area Application | Throughput Speed | Seismic Rating (SDC) | Space Efficiency Gain |
|---|---|---|---|---|
| Radio Shuttle High-Density Racking | Deep-lane cold storage & high-volume SKU buffer zones | Up to 1.2 m/s shuttle travel | Category D / E / F Compliant | +250% vs Selective Racking |
| Double-Speed Chain Conveyor (PTS2) | EV Battery assembly & high-tech device manufacturing | Precision variable (0.5–15 m/min) | High structural frame anchoring | Optimized line footprint |
| Pop-Up Roller & Chain Transfer Units | Right-angle sorting, cross-docking & pallet merging | 1000KG+ payload transfer in <2.5s | Heavy-floor anchor plates | Eliminates forklift cross-aisles |
| Automated ASRS Chain Pallet Conveyors | 24/7 Fully automated logistics & pharmaceutical hubs | Continuous 30–60 pallets/hr/lane | Integrated structural tower tie-ins | +300% Vertical Cube Usage |
| Hairise Modular Belt Spiral Conveyors | Food & beverage packaging vertical elevation transport | Continuous vertical flow | Sanitary stainless base support | Saves up to 75% floor footprint |
2. Technical Deep-Dive: Pallet Conveyor & Storage Architecture
Modern warehouse automation in Northern California demands robust mechanical integrity, high electrical compatibility (UL/CE standard integration), and seamless operational safety. Zenithrack’s manufacturing methodology integrates state-of-the-art cold roll-forming, robotic welding, and automated powder coating processes within an 8,000 m² factory footprint.
Heavy-Duty Pallet Chain Conveyors & Pop-Up Transfer Mechanics
For applications handling standard 48x40-inch GMA pallets, Euro pallets, or heavy 2-way wooden skid platforms weighing upwards of 1,500 kg (3,300 lbs), mechanical chain conveyors serve as the backbone of internal movement. Zenithrack’s heavy-duty chain conveyor series utilizes precision-engineered duplex steel roller chains riding on ultra-high-molecular-weight (UHMW) wear strips. This minimizes friction coefficients, reduces electrical power demand, and ensures zero dynamic deformation even under peak continuous loads.
When changing material directional flow at 90-degree intersections, Zenithrack’s Pop-Up Chain and Roller Transfer Units employ heavy pneumatic or motor-driven eccentric lifting cams. Capable of hoisting full 1,000 kg payload pallets within 2.2 seconds, these systems eliminate complex robotic turn-tables, keeping facility footprints compact and maintenance requirements exceptionally low.
PTS2 Double-Speed Chain Conveyors for Advanced Cleanroom & EV Production
San Francisco and Silicon Valley represent global epicenters for electric vehicle (EV) battery module assembly, semiconductor wafer transport, and advanced biomedical device manufacturing. The PTS2 Double Speed Chain Pallet Conveyor System is custom-manufactured to support cleanroom operations and ESD-sensitive handling environment requirements.
The double-speed mechanism utilizes specialized engineering plastic chain links where the outer roller diameter exceeds the inner drive roller diameter. When pallets rest on the conveyor chain, they travel at approximately 2.2 times the drive motor's linear velocity. This dynamic speed enhancement allows assembly technicians or automated robotic arms to perform work while pallets move swiftly between station index points, reducing cycle times in cleanroom assembly bays across South San Francisco and Fremont facilities.
3. Micro-Localized Application Scenarios Across Northern California Industrial Hubs
Different sub-markets within the San Francisco Bay Area exhibit distinct industrial profiles, each requiring tailored conveyor and storage rack engineering:
Silicon Valley & Fremont (Tech & EV Manufacturing)
High-precision PTS2 double-speed chain conveyors and heavy-duty pop-up transfers integrated into cleanroom environments for battery module lines, hardware testing centers, and automated sub-assembly processes.
South San Francisco & East Bay (Biotech & Pharma Clean Logistics)
Stainless steel modular belt spiral conveyors and galvanized radio shuttle racking systems deployed inside temperature-controlled storage rooms (-20°C freezer environments) to prevent corrosion and maintain strict hygiene standards.
Port of Oakland Corridor & Hayward (3PL Cross-Docking)
Flexible powered roller conveyors and heavy-duty pop-up roller systems designed for rapid container loading/unloading, high-turnover pallet buffer bays, and seamless staging near major shipping lanes.
Central Valley & Tri-Valley (Agriculture & Food Distribution)
Hairise food-grade modular belt conveyor systems and heavy-load ASRS chain pallet racks handling mass cold-storage distribution for produce, wine, and packaged food products entering the San Francisco metro area.
4. Technology Integration Trends in Northern California Material Handling
The industrial sector in San Francisco is at the forefront of combining physical material handling infrastructure with intelligent software architectures. Modern facilities are rapidly adopting three key operational paradigms:
A. AGV and AMR Conveyor Interfaces: Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs) are replacing conventional forklift transport across Bay Area fulfillment centers. Zenithrack manufactures custom docking stations, powered roller interfaces, and optical sensor alignment brackets that enable AGVs to seamlessly drop off or pick up heavy pallets from stationary chain conveyor lines without human intervention.
B. 24V DC Brushless Motor Efficiency: Energy conservation is paramount under California’s stringent Title 24 energy code standards. Zenithrack’s zero-pressure accumulation (ZPA) roller conveyor lines utilize intelligent 24V DC motorized drive rollers (MDR). Motors operate exclusively when a pallet is detected in a specific zone, cutting facility electrical energy usage by up to 55% compared to continuously running AC gearmotor drives.
C. Warehouse Management System (WMS) & Radio Shuttle Syncing: In high-density radio shuttle racking systems, Zenithrack integrates RF communication modules and optical positioning sensors. Wireless hand-held tablets allow operators to send shuttle cars into deep lanes (up to 40 pallets deep) to execute automated FIFO (First-In, First-Out) or FILO (First-In, Last-Out) retrieval scripts, feeding out-bound pallet conveyors automatically.
5. Enterprise Profile & Export Advantage: Zenithrack Industrial Equipment
When San Francisco procurement managers and general contractors source material handling equipment directly from global manufacturing hubs, verifying engineering credibility, steel quality, and production capabilities is critical to project risk mitigation.
Zenithrack Industrial Equipment Co., Ltd. is a premier manufacturer and exporter based in Dongguan, China, specializing in heavy-duty warehouse storage racks, intelligent pallet conveyors, radio shuttle systems, and multi-tier structural mezzanines. With over 15 years of focused manufacturing excellence, Zenithrack has established itself among the top-tier storage system producers, generating annual sales exceeding 100 million CNY.
8,000 m² Advanced Factory
Equipped with 35 sets of high-precision CNC roll-forming lines, automated laser cutters, robotic welding cells, and an eco-friendly automated powder coating plant.
In-House Technical Engineering
Over 75 dedicated structural engineers, quality assurance inspectors, and project managers ensuring every export order meets strict international standards.
Free Layout & CAD Design
Zenithrack provides complimentary 2D/3D warehouse CAD design layouts, structural load calculations, and installation guidance drawings within 24 hours.
OEM & Customization Support
Complete OEM/ODM customization capabilities for rack dimensions, beam profiles, custom paint finishes (RAL colors), galvanized outdoor treatments, and brand labeling.
Fast Export Lead Times
Sufficient raw material reserves (certified Q235B/Q355B steel coil) and streamlined factory automation guarantee quick 14–21 day production cycles for container shipments.
Rigorous Multi-Stage QC
Every batch undergoes strict steel thickness verification, weld seam ultrasonic flaw testing, hole-pitch accuracy inspection, and powder coating thickness testing.
6. San Francisco Market Procurement & Technical FAQ
How do Zenithrack’s pallet conveyors and racking systems comply with San Francisco seismic codes?
What information is required to receive a free custom CAD layout and quotation?
- Warehouse floor plan drawing (PDF or DWG format) showing column spacing and dock doors.
- Facility clear height under roof joists or sprinkler heads.
- Pallet dimensions (Length x Width x Loaded Height) and maximum weight per pallet.
- Handling equipment details (forklift type, reach truck model, or automated conveyor interface requirements).
- Operating environment conditions (ambient warehouse, cold storage room, cleanroom, etc.).
How do we choose between Radio Shuttle Racking, ASRS Chain Conveyors, and Selective Pallet Racks?
Selective Pallet Racking: Ideal when you stock many distinct SKUs with relatively low pallet volume per SKU, requiring 100% direct immediate access to every pallet.
Radio Shuttle Racking: Recommended when floor space is expensive and you have high pallet volume per SKU. It provides maximum density (up to 85% cube utilization) with automated deep-lane shuttle retrieval under FIFO or LIFO operating models.
Intelligent ASRS Chain Conveyors: Chosen for fully automated high-throughput manufacturing lines (such as EV battery assembly or pharmaceutical distribution) requiring 24/7 continuous transport, zero manual forklift labor, and direct integration with software WMS systems.