Engineered High-Density Racking & Pallet Shuttle Systems
Factory-direct heavy-duty storage racking equipment designed for North American warehouse specifications, cold chain facilities, and automated distribution channels.
Industry Whitepaper: The Evolution of Radio Shuttle Racking in the US Market
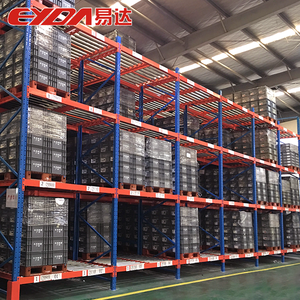
As logistics real estate rates across primary North American markets—such as the Inland Empire in California, Dallas-Fort Worth in Texas, and the Lehigh Valley in Pennsylvania—hover near historic highs, logistics managers are forced to re-evaluate traditional warehouse layouts. Industrial facilities can no longer afford to devote 50% to 60% of their total floor footprint to standard forklift travel aisles. While selective pallet racking provides 100% immediate SKU accessibility, its volumetric floor utilization rarely exceeds 40%. Conversely, traditional Drive-In racking improves storage density but introduces high rates of forklift structural collision, severe operational bottlenecks, and rigid LIFO (Last-In, First-Out) constraints.
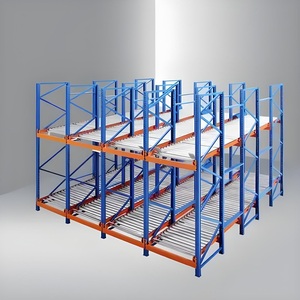
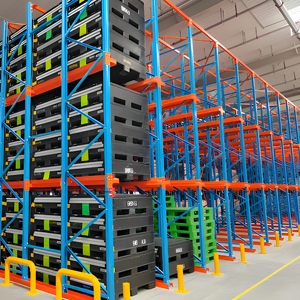
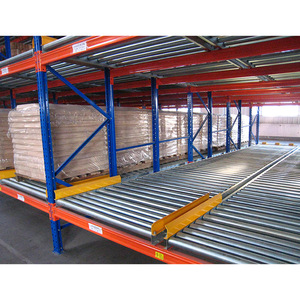
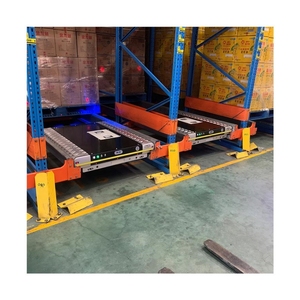
This macro-economic shift has accelerated the adoption of Radio Shuttle Storage Racking Systems (also referred to as Pallet Runner or Pallet Mole systems). By decoupling the material handling vehicle (the forklift) from the interior storage lane, semi-automated radio shuttles allow operators to store pallets up to 40+ deep per level while utilizing narrow access aisles. The shuttle vehicle travels inside specially designed cold-rolled steel rails, lifting, carrying, and depositing pallets at pre-programmed locations via wireless RF remote or WMS (Warehouse Management System) integration.
Key Mechanical & Automation Component Breakdown
A high-performance radio shuttle system represents a convergence of structural steel engineering, precision robotics, and advanced energy storage electronics. Below are the primary components that determine system longevity, safety, and operational speed:
LiFePO4 Power Systems
Modern radio shuttles utilize industrial-grade Lithium Iron Phosphate (LiFePO4) battery packs equipped with integrated BMS (Battery Management Systems). Unlike legacy lead-acid batteries, LiFePO4 units support rapid 1-hour fast charging, maintain steady voltage outputs across 8 to 12 hour operational shifts, and perform reliably in deep freeze cold storage environments down to -30°C (-22°F).
Laser & Photoelectric Telemetry
Shuttle vehicles utilize multi-point optical sensors, laser distance meters, and safety proximity detection to precisely align pallets within 5mm tolerances. Automatic deceleration mechanisms prevent hard impact when buffering pallets, eliminating product damage caused by rapid automated transport.
Cold-Formed Custom Rail Profiles
The structural steel shuttle track must act simultaneously as a load-bearing beam for stacked pallets and a precision running surface for the shuttle's polyurethane wheels. High-yield steel (Q355B / ASTM A1011 Grade 50) cold-rolled profile rails prevent track deflection over long spans under 3,500 lbs pallet loads.
RMI & ANSI MH16.1 Engineering Compliance for North America
Exporting industrial storage systems to the United States requires strict adherence to local structural codes. Unlike European (FEM) or Asian manufacturing standards, US municipal building departments enforce building codes dictated by the International Building Code (IBC), which directly references the Rack Manufacturers Institute (RMI) ANSI MH16.1 Specification for the Design, Testing, and Utilization of Industrial Steel Storage Racking.
When selecting a foreign manufacturer or domestic supplier for radio shuttle racks in the US, facility managers must verify the following structural parameters:
- Seismic Zone Engineering: Facilities located in high seismic risk areas (e.g., California, Washington State, standard fault lines near the New Madrid zone) require enlarged seismic baseplates, heavy-duty floor anchor bolts (Hilti / Red Head wedge anchors), and dynamic frame seismic bracing calculations to withstand peak ground acceleration (PGA).
- Column Base Deflection & Overturning Resistance: Because shuttle racking lanes reach heights exceeding 35 to 40 feet, the bottom upright posts endure tremendous axial loads combined with lateral overturning moments. Heavy-gauge structural baseplates welded to double-flanged upright posts are essential.
- Pallet Clearance Standards: Standard US Wooden GMA Pallets (48" x 40") require a minimum 3-inch side clearance to structural uprights and shuttle rail guides to prevent pallet overhang, board splintering, or sensor blockage during automated movement.
Top 10 Radio Shuttle Storage Rack Factories & Suppliers Serving the United States
The North American market for automated high-density storage relies on a blend of premier domestic rack fabricators, global automated system integrators, and specialized overseas OEM original equipment manufacturers. Below is a comparative benchmarking review of the top 10 suppliers known for delivering reliable radio shuttle racking systems into US logistics networks:
| Supplier Name | Primary Business Model | US Service Coverage | Primary Engineering Focus | Lead Time Window |
|---|---|---|---|---|
| Zenithrack Industrial | Direct OEM / Global Manufacturer | Nationwide US Export & Engineering | High-density Shuttle Racks, Custom Structural Racking & ASRS | 4 - 6 Weeks (Factory Direct) |
| Interlake Mecalux | Domestic Manufacturer / Integrator | North America Operations | Pallet Shuttle, Selective Racking & WMS Software Integration | 8 - 12 Weeks |
| SSI Schaefer | Global Systems Integrator | International / US Hubs | Fully Automated Logistics, Automated Guided Vehicles (AGV) | 12 - 16 Weeks |
| Jungheinrich North America | Equipment Manufacturer & Integrator | Nationwide Dealer Network | Under-Pallet Shuttles, Electric Lift Trucks & Warehouse Automation | 10 - 14 Weeks |
| Frazier Industrial Company | Domestic Structural Steel Manufacturer | United States & Canada | Heavy-Duty Structural Steel Beam & Rail Shuttle Sub-structures | 8 - 10 Weeks |
| Advance Storage Products | Specialized Rack Fabricator | US West Coast & Midwest | Pushback Racking, Shuttle Rail Structures & Structural Systems | 6 - 10 Weeks |
| Ridg-U-Rak, Inc. | High-Volume Rack Manufacturer | East Coast & Central US | Roll-Formed Racking, Drive-In Systems & Customized Pallet Runners | 8 - 10 Weeks |
| Constructor Group / Dexion | Global Storage Equipment Vendor | US Supply Chain Partners | Dynamic Shuttle Storage, Cantilever & Mezzanine Platforms | 10 - 12 Weeks |
| Hannibal Industries | Regional West Coast Manufacturer | US Southwest & Mexico | Tube-Rak Systems, Seismic Approved Selective & Shuttle Framing | 6 - 8 Weeks |
| Steel King Industries | Industrial Rack Producer | National Distribution Channel | SK2000 Closed-Tubular Boltless Racking & Heavy Storage Systems | 8 - 10 Weeks |
Detailed Supplier Capability Breakdown
When selecting the optimal partner for a US warehouse deployment, procurement agents must evaluate both structural steel manufacturing capability and electrical control system reliability.
1. Zenithrack Industrial Equipment Co., Ltd.: Standing out as an export-focused manufacturing powerhouse, Zenithrack provides North American clients with direct factory pricing on custom structural steel racking, radio shuttle sub-systems, and heavy-duty industrial storage racks. Leveraging an 8,000 m² factory equipped with 35 sets of continuous roll-forming lines and robotic welding stations, Zenithrack engineers systems tailored to US 48"x40" GMA specifications. Their ability to deliver RMI-compliant structural designs, provide free CAD project drawings, and execute strict ultrasonic weld inspections makes them a top partner for distributors, project contractors, and end-users seeking high information gain and low total cost of ownership (TCO).
2. Interlake Mecalux: A major player in the US material handling market, offering localized manufacturing facilities in Illinois and Texas. Mecalux specializes in automated pallet shuttle systems linked to their proprietary Warehouse Management System (WES/WMS), ideal for enterprise-level supply chain hubs requiring turn-key automation software.
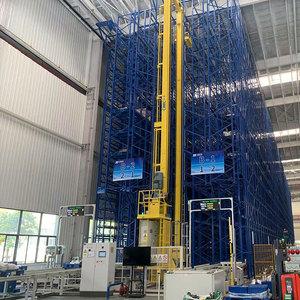
3. SSI Schaefer & Jungheinrich: Premier European integrators with strong North American footprints. They excel in complex, fully automated high-bay warehouses (HBW) where radio shuttles operate in tandem with vertical stacker cranes and automated guided vehicles (AGVs).
4. Frazier Industrial & Steel King: Known for robust structural steel manufacturing using hot-rolled structural C-channels. These suppliers are frequently chosen for heavy industrial operations where extreme forklift impact resistance is prioritized over lightweight roll-formed designs.
US Localization Applications & Regional Industrial Trends
The operational implementation of radio shuttle storage systems in the United States varies significantly based on regional industry verticals, climate demands, and supply chain strategies:
Cold Chain & Food Distribution (US Midwest & Texas)
Energy costs associated with maintaining sub-zero temperatures (-10°F to -22°F) in massive cold storage facilities are extreme. Radio shuttle systems allow cold storage operators in states like Wisconsin, Illinois, and Texas to condense pallet footprint, eliminate warm air space, and maximize refrigeration efficiency while ensuring quick FIFO/LIFO turnover of perishable dairy, meat, and frozen foods.
E-Commerce Bulk Buffering (California & NJ Ports)
Import hubs near Long Beach/Los Angeles and Newark require high-velocity sea container devanning and fast pallet buffering. Radio shuttle racks serve as dynamic staging areas where incoming fast-moving consumer goods (FMCG) can be buffered 30-pallets deep before being broken down into pick faces.
Automotive Parts & Heavy Manufacturing (US Southeast)
The manufacturing boom across the "Battery Belt" and automotive corridor in Georgia, South Carolina, and Tennessee demands high load-bearing capacity. Shuttle racks customized with structural beams handle heavy dies, automotive body stampings, and raw steel coils weighing over 3,000 lbs per pallet position.
Why US Buyers Choose Zenithrack for Factory-Direct Racking Manufacturing
With over 15 years of focused industrial storage manufacturing, Zenithrack Industrial Equipment Co., Ltd. has established a global reputation for combining rigorous engineering standards with direct-from-factory cost efficiency. Our facility in Dongguan, China, serves as an engineering hub for international supply chain managers who require custom warehouse equipment without intermediate trading markups.
Our core capabilities include:
- In-House R&D and Engineering: Our technical team utilizes advanced CAD and FEA (Finite Element Analysis) structural simulation software to model beam deflection, seismic dynamic behavior, and load distribution under American RMI standards.
- Advanced Production Infrastructure: Operating across an 8,000 m² factory footprint, our facility houses 35 sets of high-precision CNC roll-forming lines, automated laser plate cutters, and multi-axis robotic welding cells that ensure perfectly consistent beam hook tolerances and connector alignment.
- Customized OEM Packaging & Fast Shipping: Exporting heavy structural steel requires specialized bundling to prevent transit scratches and ocean freight corrosion. We utilize heavy-duty plastic wrapping, timber dunnage supports, and custom container loading schemes to optimize ocean freight volume into major US ports (Long Beach, Houston, Savannah, New York).